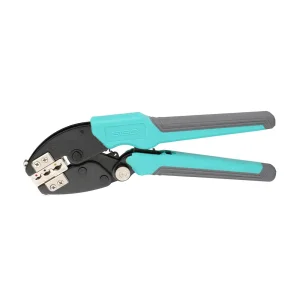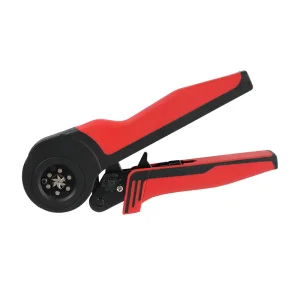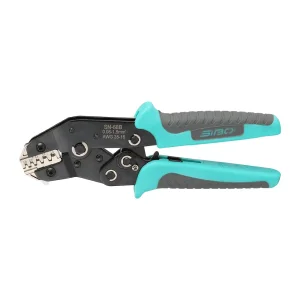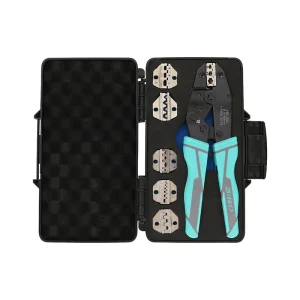
Calibrated for industrial panel builders, solar PV field technicians, and automotive wire harness manufacturers demanding complete structural compaction and gas-tight electrical joins.
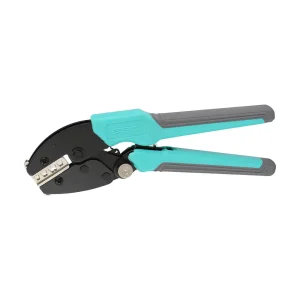
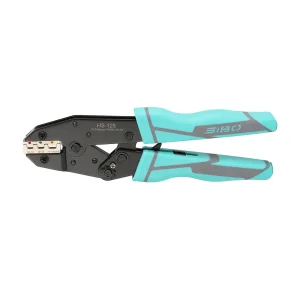
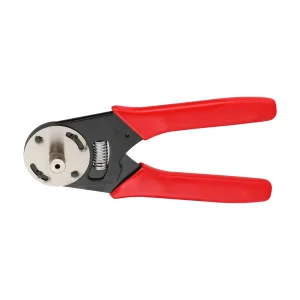
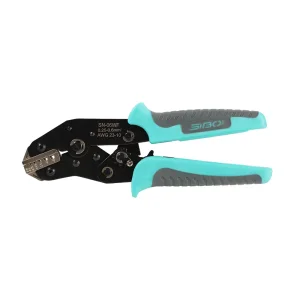
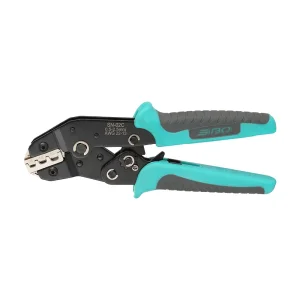

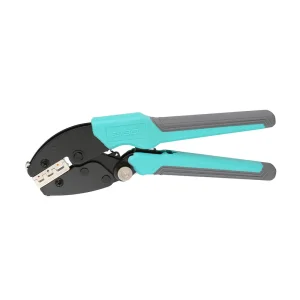
Cold plastic deformation requires rigorous control over terminal barrel geometry, copper strand compaction, and volumetric stress relaxation to eliminate voids and establish micro-welded junctions.
Micro-wire processing (D-Sub connectors, sensor terminations, industrial Ethernet, and ECU harness loops) requires micron-scale die tolerance (±0.01mm). Insufficient crimp height causes intermittent high-resistance faults, while over-crimping shears microscopic copper strands. Our Yueqing manufacturing line implements EDM wire-cut dies calibrated for exact conductor envelope ratios, preserving tensile integrity according to DIN EN 60352-2.
Encompassing DIN insulated ferrules, pre-insulated rings/spades, and MC4/solar connectors (2.5/4/6 mm²). In solar PV applications, thermal cycling creates cyclic stress that induces terminal fretting. SIBO high-leverage ratchet mechanisms utilize cold-rolled 42CrMo structural alloy jaws that ensure a gas-tight, oxygen-free contact interface preventing copper oxidation and reducing contact resistance below 5 milliohms.
At 16mm² to 50mm², hand-tool leverage requires high mechanical advantage through progressive toggle-link or gear-assisted ratchets. Hexagonal and indent compression profiles force stranded Class 2 and Class 5 copper cores into solid polygon formations. Each crimp meets UL 486A-486B mechanical extraction forces without shearing insulation jackets or warping copper cable lug tangs.
| Wire Range (mm²) | AWG Equiv. | Typical Die Profile | Primary Terminal Classification | Target Extraction Force (Min. IEC/UL) | Recommended SIBO Series |
|---|---|---|---|---|---|
| 0.1 – 1.0 | AWG 28 – 18 | Micro B-Crimp / 4-Indent | Deutsch DT, D-Sub, JST, Micro-Lock | > 20 N – 90 N | SN-68B / Deutsch Closed Barrel DT |
| 0.25 – 6.0 | AWG 24 – 10 | Trapezoidal / Oval Dual-Stage | Pre-insulated Ring, Spade, Ferrules | > 50 N – 360 N | SN-06WF / SO-30J / SO-125 Pro |
| 2.5 – 6.0 | AWG 14 – 10 | Precision F-Crimp with Locator | Photovoltaic (MC4 / Sunclix type) | > 310 N (UL 6703 Standard) | SO-2546B Pro / SO-2546C Pro |
| 0.08 – 16.0 | AWG 28 – 5 | Self-Adjusting Hexagonal / Square | Bootlace Ferrules, Twin Insulated Ferrules | > 40 N – 570 N | SO 16-4 / SO 16-6 Hexagonal |
| 10.0 – 50.0 | AWG 8 – 1/0 | Compound Indent / Heavy Hex | Non-Insulated Heavy Lugs, Battery Terminals | > 670 N – 1800 N | SO-10 Pro / Heavy Series / Custom Modular |
Based in Yueqing, Zhejiang—the core of China’s electrical apparatus manufacturing sector—our manufacturing operations leverage complete supply-chain integration, rapid prototyping, and scalable production capacity.
Yueqing contains over 10,000 electrical manufacturing enterprises within a 30-kilometer radius. Raw alloy steel suppliers, precision CNC tooling facilities, specialized vacuum heat-treatment furnaces, and mold foundries operate in close coordination. This localized integration reduces procurement turnaround from weeks to days, protecting international brand customers against raw material delays and volatile shipping schedules.
Tool longevity depends on balanced metallographic grain structure. Our workshop uses continuous salt-bath quenching and controlled vacuum induction tempering to treat ratchet pawls, eccentric pivots, and die blocks. The main frame attains HRC 40–45 for elasticity, while crimping cavities achieve HRC 58–62 for wear resistance over tens of thousands of cycles.
Supplying multinational retail brands and regional industrial wholesalers requires strict customization flexibility. We manufacture specialized handle geometry, customized dual-color ergonomic grips (PP+TPR), laser-engraved part serializations, branded blister kits, and Oxford zip cases with customizable quick-swap die inserts tailored to custom terminal cross-sections.
From extreme sub-zero renewable generation fields to tight aviation test benches, reliable terminal crimping protects critical electrical systems against vibration, thermal expansion, and mechanical shock.
Photovoltaic installations operate under high DC voltages (up to 1500V DC). Defective open-barrel crimps on 2.5mm², 4mm², or 6mm² PV cables are a primary root cause of series arc faults and module fires. The SO-2546 series provides controlled crimp height and built-in terminal locator guides, ensuring reliable field assembly across utility-scale arrays and rooftop setups.
Modern transportation electrical architectures feature both micro-sensor wiring (0.1–0.5mm²) and high-power battery storage links (16–50mm²). Deutsch closed-barrel connectors (DT/DTM series) require four-indent crimps that grip both insulation and core conductors without distorting round pin alignments, maintaining IP68/IP69K environmental sealing under vibration.
Control cabinet assembly demands clean wire organization. Self-adjusting square (SO 16-4) and hexagonal (SO 16-6) crimpers shape twin and single ferrules into standardized profiles that seat flush into push-in terminal blocks, avoiding stray copper whiskers that can trigger short circuits in PLC control systems.
Every hand tool manufactured by SIBO conforms to international electrical performance criteria. Our quality laboratory uses tensile destruction benches, micro-sectioning, and cycle durability tests to maintain process consistency.
We evaluate mechanical tensile retention by applying axial loads at regulated pull speeds until conductor separation or breakage. Our tools consistently exceed required pull-out thresholds (e.g., >570 N for 16mm², >1500 N for 50mm²), ensuring connections hold under real-world cable-pull and vibration stresses.
Destructive metallurgical micrographic inspection ensures crimp quality. Samples are cast in resin, diamond-lapped to mirror clarity, and examined under 200x digital magnification. Quality crimps exhibit uniform strand compression with no internal voids, micro-fissures, or cracked insulation barrels.
Materials for tool handles and metallic components are fully compliant with EU RoHS 2.0 (Directive 2011/65/EU) and REACH (EC 1907/2006). Grip plastics are free from banned phthalates, SVHCs, and heavy metals, qualifying them for major retail channels across Europe and North America.
Meeting modern industrial requirements demands lighter handle designs, fast tool-free die changes, and digital tracking for traceable assembly processes.
Replacing standard hex-key die fasteners with neodymium magnetic indexing systems. Allows field operators to swap between insulated, non-insulated, and ferrule jaws in under 5 seconds with positive tactile engagement.
Implementing forged aluminum-magnesium aircraft alloys for frame arms. Reduces overall tool weight by 38% compared to traditional stamped carbon plates, cutting operator hand fatigue during repetitive installation shifts.
Embedding high-frequency NFC tags into tool handles. Enables technicians to scan the tool with a mobile device to log calibration dates, verified wire gauges, and maintenance records into corporate ERP systems.
Integrating compact micro-sensors into the toggle frame. Provides instant green/red LED feedback verifying adequate peak compressive tonnage on each crimp, preventing incomplete cycles on safety-critical assemblies.
Detailed answers addressing tool life, terminal compatibility, die maintenance, and private-label ordering for international buyers.
Ratchet crimpers (such as our SO-30J and SO-125) use precision-machined cavities engineered for designated wire cross-sections. A full-cycle ratchet holds the handles closed until full stroke depth is reached, ensuring consistent crimp height across production runs. Self-adjusting tools (like the SO 16-4 and SO 16-6) use sliding multi-segment cam jaws that adjust dynamically to single or twin ferrules from 0.08mm² to 16mm², making them versatile for panel maintenance and troubleshooting.
Die longevity depends on core metallurgy and surface processing. We use 42CrMo and tool-grade carbon alloy steels. The dies undergo vacuum heat treatment followed by precision surface carbonitriding, providing an outer hardness of HRC 58–62 with a tough inner matrix. This prevents cavity widening, shoulder cracking, and deformation under daily use.
Die profile selection is dictated by terminal geometry and application standards: Hexagonal delivers uniform radial pressure for round pin contacts and power lugs (10–50mm²); Square provides high edge-contact force for wire ferrules into spring-loaded terminal blocks; B-Crimp (F-Crimp) rolls open-barrel tabs into stranded conductor cores for automotive harnesses; and Indenters pierce heavy non-insulated lugs (SO-10 Pro) for low-resistance earthing bonds.
For standard models with custom laser-marked logos, MOQs start at 500 units. For fully customized dual-color ergonomic handles, unique die sets, and tailored packaging (blister cards, color boxes, or branded Oxford zip kits), typical batch sizes start at 1,000 to 2,000 units. Standard production lead times average 25 to 35 days, supported by buffer stocking programs for contracted distributor accounts.
If oversized wire or incorrect terminal placement stalls the tool before completion, SIBO ratchet tools include a manual quick-release lever located between the internal handles. Pressing the release disengages the ratchet pawl immediately, opening the jaws and allowing safe tool extraction without damaging the frame or dies.
Every commercial production batch can include EN 10204 Type 3.1 material certificates for raw steel, tensile pull-test verification reports (IEC 60352-2 / UL 486A), RoHS/REACH compliance documentation, and standard Certificate of Origin paperwork (Form E, CO, or EUR.1) to simplify customs clearance.
Tested and calibrated for industrial distribution networks, field contractors, and high-volume cable harness assembly workshops.