
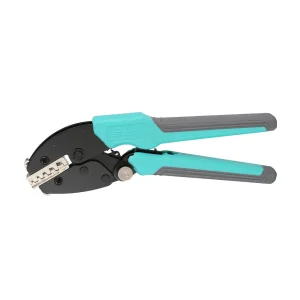
Engineered with auto-stop full-cycle ratchets, micro-wire EDM EDM die cavities, and ergonomic high-leverage force transfer handles for zero-failure electrical terminations.


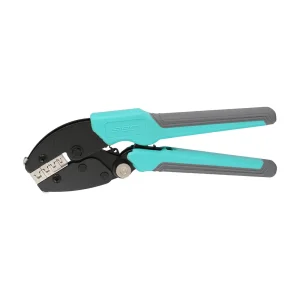
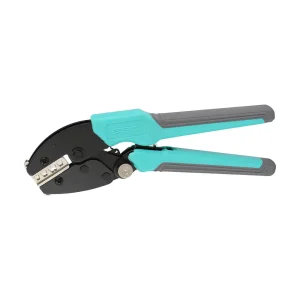
Why ratchet mechanism precision governs electrical conductivity, thermal endurance, and permanent contact resistance.
Crimping is not merely squeezing metal; it is a precisely controlled mechanical cold-extrusion event. When stranded copper conductors are compressed within a conductive terminal sleeve, both the terminal barrel and wire strands undergo severe plastic flow.
SIBO ratchet crimping tools feature die cavities ground within micro-tolerances (±0.015mm), ensuring the terminal walls compress beyond the copper's yield point without reaching shear fatigue. This eliminates microscopic voids between wire strands, achieving a monolithic copper density that resists oxidation and corrosion over decades of thermal cycling.
Under non-optimized manual compression, air remains trapped between strands. Ambient oxygen, moisture, and industrial sulfur cause copper oxidation, drastically increasing electrical resistance ($R_{contact}$) and precipitating thermal runaway.
A true gas-tight joint, guaranteed by our full-cycle ratchet linkage, shears the surface oxide layers on both the stranded wires and the inner barrel walls. Under high compressive pressure, virgin metal surfaces fuse at the molecular level, fulfilling the strict gas tightness requirements of IEC 60352-2 without requiring heat or solder fluxes.
Operator fatigue is the primary culprit behind field connection failure. Standard non-ratchet crimpers allow premature jaw release, yielding inconsistent crimp heights and reduced tensile pull-out strength.
Our hardened carbon-steel ratchet pawl and wheel system enforces mandatory cycle completion: the jaws will not open until complete closure is achieved. Coupled with an emergency safety release lever and a calibrated eccentric pressure adjustment disc, each tool provides quantifiable repeatability across tens of thousands of cycles.
Located in Yueqing, Zhejiang—China's global capital of low-voltage electrical equipment—SIBO Tools integrates raw metallurgy, precision CNC tooling, and direct-to-port export infrastructure.
Yueqing houses thousands of specialized electrical component, stamping, and metallurgical facilities. We source premium 42CrMo alloy steel and special engineering polymers within a 15-kilometer radius, drastically compressing lead times and raw material freight overhead.
Unlike budget stamping operations, SIBO utilizes slow-feeding wire electrical discharge machining (WEDM) and multi-axis CNC machining centers. This delivers polished die cavities with sub-micron surface finishes that prevent plating galling or terminal sticking.
Our pliers frames and jaw dies undergo multi-stage vacuum heat treatment and oil quenching. Jaws reach a calibrated hardness of HRC 48-52, ensuring wear resistance exceeding 50,000 crimp cycles while maintaining core mechanical toughness against brittle fracture.
From custom 3D CAD modeling of bespoke die cavity profiles to rapid tooling prototyping, customized dual-injection soft grip molding, and private-label laser etching, our in-house engineering team accelerates product launch cycles from months to weeks.
A single sub-standard crimp can cause catastrophic electrical fires, grid downtime, or vehicle recalls. Discover how SIBO tools provide standardized integrity across key global industries.
The Challenge: Modern solar installations run at DC potentials up to 1500V. Field assembly of MC4 and compatible PV connectors requires consistent contact resistance ($<0.25\text{ m}\Omega$). Any crimping imperfection introduces a hot-spot that degrades string yield or causes arcing fires.
The SIBO Solution: Our SO-2546B Pro and SO-2546C Pro series incorporate precision locator plates and progressive B-crimp cavities for 2.5mm², 4mm², and 6mm² (14-10 AWG) PV cables. The ratchet release ensures the stamped solar contact's insulation and core tabs compress uniformly, matching international IEC 62852 standards.
The Challenge: Automotive engine bays, chassis sensor lines, and battery management harnesses undergo relentless mechanical vibration and thermal oscillation from -40°C to +125°C. Open-barrel connectors must grip both the core and rubber wire seals without tearing.
The SIBO Solution: Tools like the SO-04BPro and SN-68B feature stepped F-crimp and B-crimp geometries. By forming the conductor wings into smooth, overlapping hearts while independently stabilizing the insulation strain relief, SIBO tools safeguard wire harnesses against vibration fatigue according to USCAR-21 specifications.
The Challenge: High-density control cabinets utilize multi-core flexible wires that must be terminated into terminal blocks and spring clamps via insulated ferrules. Improperly shaped ferrules loosen, overheat, or fail pull-out tests.
The SIBO Solution: Our self-adjusting hexagonal and trapezoidal crimpers (such as the Mini Hexagonal 16-6 and SN-06WF) automatically adapt pressure according to conductor gauge (0.25 to 6mm² or up to 16mm²). The resulting uniform geometric crimp guarantees seamless insertion into cage clamps and contactors in compliance with DIN 46228 Part 1 & 4.
The Challenge: Telecommunication base stations and rail transit signal panels require zero micro-arcing and complete electromagnetic shielding stability. Connections involve both uninsulated spade terminals and high-density circular connectors.
The SIBO Solution: The SO-10 Pro and SO-10WF Pro provide heavy-duty indent compression dies designed for pure mechanical cold consolidation of copper lugs up to 10mm². Every batch delivers certified mechanical retention, preventing signal dropouts under extreme environmental conditions.
B2B tooling distributors, private-label brand owners, and utility procurement directors can cross-reference terminal topologies against our specialized mechanical crimper architectures.
| Series & Model | Terminal Architecture | Wire Gauge Range | Die Geometry Type | Mechanism & Adjustment | Primary Industrial Sector |
|---|---|---|---|---|---|
| SO-30J Pro | Insulated Terminals (Red, Blue, Yellow) | 0.5 – 6.0 mm² (AWG 22-10) | Color-coded Oval Compaction | Full-cycle Ratchet + Pressure Disc | Building Switchboards, HVAC, Control Panels |
| SO-2546B/C Pro | Solar PV MC4 Pins & Sockets | 2.5 / 4.0 / 6.0 mm² (AWG 14-10) | Stepped Locator B-Crimp | Precision Calibrated Ratchet | Solar EPC, PV Farm Maintenance, Inverters |
| SO-04BPro | Non-Insulated Open-Barrel Tabs | 0.5 – 6.0 mm² (AWG 20-10) | Dual-Fold B-Type Wing Crimp | Progressive Mechanical Leverage | Automotive Harness, White Goods, Sensors |
| SO-10 Pro | Non-Insulated Ring & Fork Lugs | 1.5 – 10.0 mm² (AWG 16-8) | Single-Point Indent Wedge | High-Ratio Lever Carbon Frame | Power Distribution, Grounding Networks |
| SO-10WF Pro | End Sleeves / Wire Ferrules | 0.25 – 10.0 mm² (AWG 24-8) | Trapezoidal Progressive Profile | Auto-Locking Precision Ratchet | PLC Terminal Blocks, European Cabinetry |
| Mini 16-6 Hex | End Sleeves / Ferrules | 0.08 – 16.0 mm² (AWG 28-5) | Self-Adjusting Hexagonal Form | Synchronized 6-Jaw Cam Assembly | Automation Machinery, Micro-terminals |
| HS-30J Set | Multi-Terminal (Quick Change 5 Jaws) | 0.5 – 16.0 mm² Modular | Interchangeable Jaws Kit | Heavy-Duty Ratchet + Oxford Bag | Field Maintenance, OEM Repair Kits, Retail |
We provide complete custom color matching (Pantone-specific dual-component TPR handles), corporate brand laser engraving on polished jaws, and certified custom mold toolmaking for distinctive ergonomic handgrips that elevate your tool brand in regional markets.
Choose from industrial blow-molded cases, durable custom 600D Oxford zipper carrying pouches with elastic organization loops, blister packaging with full-color CMYK insert cards, or sustainable kraft retail boxes engineered to optimize pallet shipping volumes.
Each production run is tracked through raw steel spectrometry, Vickers micro-hardness testing, tensile test bench validation ($F_{pull}$ pull-off tests), and crimp cross-section analysis. Mill test certificates and REACH/RoHS compliance sheets are provided with every order.
From clean-energy electrification to micro-wire miniaturization, hand crimper design is advancing rapidly to meet stringent next-generation standards.
Modern electrical codes demand thicker terminal barrels and specialized copper alloy materials. To combat repetitive strain injuries (RSI) among technicians, SIBO has re-engineered the mechanical leverage toggle ratio in its Pro series. By increasing kinetic transmission efficiency by over 35%, operator hand grip force is reduced from 450N to less than 280N without diminishing terminal compression force.
As bifacial solar panels and decentralized string inverters reach higher currents (over 30A per string), contact resistance specifications have narrowed dramatically. Hand tool dies are evolving from generic notches into calibrated, brand-specific nesting cavities equipped with integrated terminal stops to prevent contact pin bending during crimp cycling.
With electronic control units (ECUs), sensor networks, and autonomous robotics requiring sub-miniature wire sizes (AWG 32 to 24), crimper dies demand ultra-fine tolerances. SIBO's investments in optical profile grinding and nano-coatings enable flash-free miniature crimps that eliminate damaged insulation jackets or deformed locking lances.
Essential guidance directly from our factory engineering team addressing die calibration, international standards, and OEM collaboration.
A genuine full-cycle ratchet incorporates an internal spring-loaded pawl that mechanically prevents the plier handles from opening once compression has begun, releasing only when the crimp stroke hits 100% mechanical closure. This eliminates operator variability and under-crimped connections, ensuring gas-tight joint compliance under IEC 60352-2 standards.
SIBO tools are equipped with a star-wheel eccentric adjusting disc secured by a locking screw. By rotating the disc clockwise or counterclockwise (+/-), technicians can fine-tune compressive force to compensate for handle flex, micro-wear, or specific terminal wall thickness variations over the life of the tool.
Yes. As a direct-factory manufacturer, our R&D engineering department requires only sample terminals and wire cross-section specifications (or CAD drawings). We design custom die geometry, mill prototypes on our slow-feeding CNC wire EDM units, and provide certified pull-test cross-section reports within 15 working days.
Standard factory catalog models in standard packaging maintain an agile MOQ of 100 to 500 units, with dispatch capability in 7 to 14 days. Comprehensive OEM orders featuring custom handle colors, custom pad printing/laser branding, and bespoke packaging require an MOQ of 1,000 units with a production turnaround of 25 to 35 days.
Open-barrel tools (e.g., SO-04BPro) roll metal tabs into an interlocking B-shape directly onto stripped wire and jacket strain reliefs. Insulated terminal tools (e.g., SO-30J Pro) compress color-coded vinyl/nylon sleeves without puncturing the dielectric. Ferrule crimpers (e.g., Mini 16-6) form stranded wire bundles into square, trapezoidal, or hexagonal shapes to fit screw and spring clamps.
Our products undergo rigorous testing according to DIN EN 60352-2, DIN 46228, and UL 486A-B criteria. We verify tensile retention strength on calibrated motorized test stands, conduct micro-section etching to inspect copper compaction, and test hardness across all wear surfaces to maintain uniform factory standards.
Explore our classic, multi-die combination toolkits, European-style mini pliers, and self-adjusting hexagonal crimpers engineered for specialized industrial assembly.
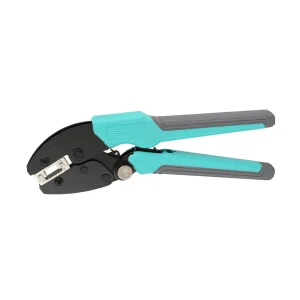
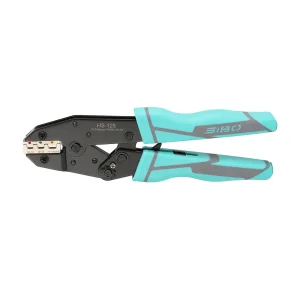
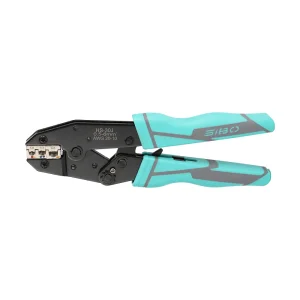
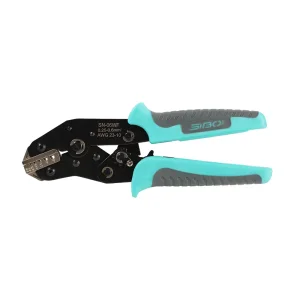
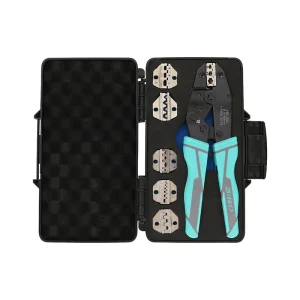


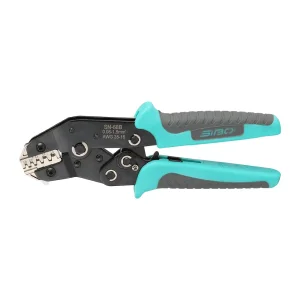
Whether you require 10,000 customized private-label ratchet crimpers for a national tool brand rollout or high-precision MC4 connector pliers for commercial solar installations, SIBO Tools delivers verified manufacturing quality directly from Yueqing, China.