Engineered for high-repetition termination integrity across solar power stations, OEM wiring harnesses, and high-density industrial control cabinets.
A rigorous analysis of why mechanical ratcheting geometry, synchronized die profiles, and carbon-alloy thermal processing determine electrical conductivity and joint longevity.
Equipped with a positive locking mechanism that prohibits jaw release until full mechanical stroke closure is achieved. This eliminates human error, operator fatigue inconsistencies, and incomplete crimp heights that lead to thermal degradation in field connections.
Dies are produced using precision wire-EDM cutting from vacuum-treated AISI 4140 or equivalent chromium-molybdenum tool steels. Hardened to 42-48 HRC, they withstand hundreds of thousands of compression cycles without profile deformation or dimensional drift.
Our tooling induces controlled plastic deformation of both the stranded conductor and the connector barrel. By eliminating micro-voids, the interface achieves a gas-tight bond that completely isolates the copper core from oxidative atmospheric ingress.
| Tool Architecture | Terminal Profile Suitability | Wire Cross-Section (mm² / AWG) | Mechanical Release Mechanism | Contact Resistance Target |
|---|---|---|---|---|
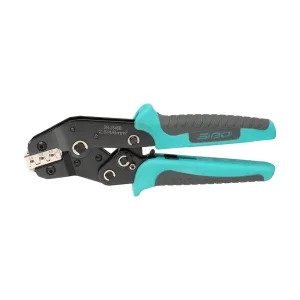
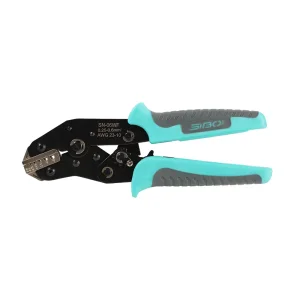
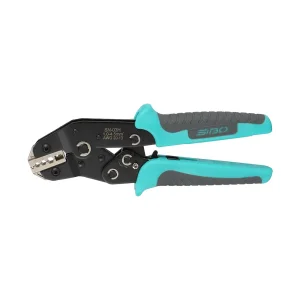
| SN-2546B Pro Series | Solar PV (MC4 Type Contacts) | 2.5 / 4.0 / 6.0 mm² (14-10 AWG) | Full-cycle ratchet with manual emergency bypass | < 0.25 mΩ |
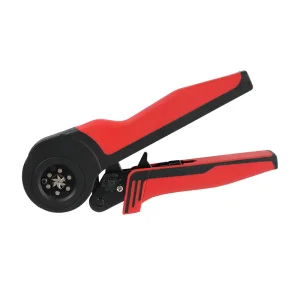
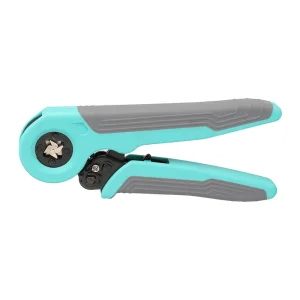
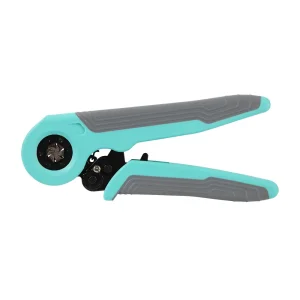
| SO-16-6 Hexagonal | End Sleeves / Wire-End Ferrules | 0.08 - 16.0 mm² (28-5 AWG) | Self-adapting mechanical cam action | Conforms to DIN 46228 Part 1 & 4 |
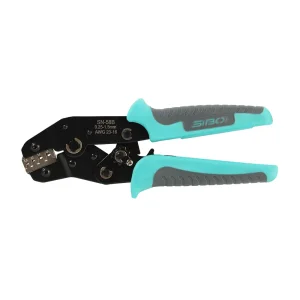
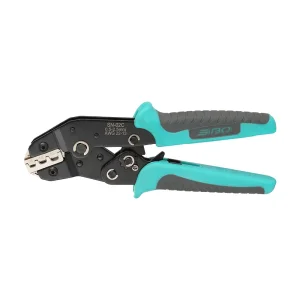
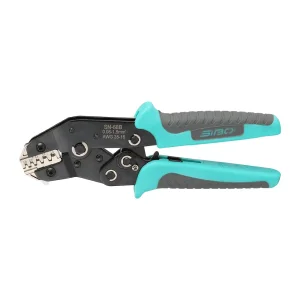
| SN-58B Precision | Open Barrel (Dupont, JST, Molex) | 0.25 - 1.5 mm² (24-16 AWG) | Synchronized double-hinge toggle ratchet | IEC 60352-2 Compliant Pull-Out |
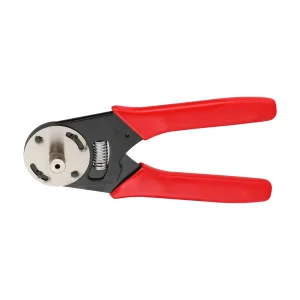
| SO-10 Pro Heavy-Duty | Non-Insulated Rings & Spades | 1.5 - 10.0 mm² (16-7 AWG) | High-leverage eccentric pivot hinge | UL 486A-486B Industrial Standard |
Located in Yueqing, Zhejiang—the undisputed global epicenter for low-voltage electrical apparatus—SIBO delivers integrated design-to-delivery speed that traditional western toolmakers cannot emulate.
Every step—progressive stamping, high-frequency induction hardening, electrostatic handle molding, and automated die CNC machining—is orchestrated within a 15km operational radius.
Custom terminal designs require custom die profiles. Our localized engineering ecosystem allows SIBO to draft, wire-cut, harden, and calibrate bespoke die profiles in less than 72 hours.
Bulk acquisition of certified high-carbon steel plates and standardized handle component molds translates directly into aggressive cost efficiencies for Tier-1 tool brands and distributors.
Every batch of compact crimping pliers undergoes tensile pull testing (IEC 60999 compliance) and optical cross-section micrography to assure absolute uniformity before container departure.
B2B tool importers, private-label conglomerates, and technical contractors require rigorous validation. SIBO implements full compliance protocols aligned with European and North American industrial frameworks.
Every crimp profile is pre-validated against standard pull-out force criteria (IEC 60352-2 and DIN EN 60947-1). Tools are engineered to withstand maximum extraction forces without slippage or conductor shearing.
All thermoplastic elastomer (TPR/PP) dual-injection handle grips undergo toxicological screening. We guarantee zero restricted phthalates, lead, or halogenated compounds, fulfilling strict EU chemical safety directives.
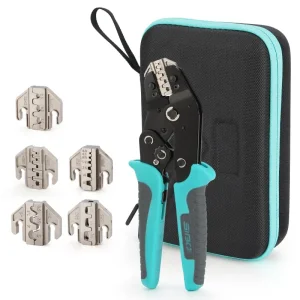
From personalized corporate color palettes and dual-tone grip molding to permanent fiber-laser logo engraving and tailored Oxford storage kit layouts, our manufacturing team delivers turnkey brand solutions.
How electrification, automated harness assembly, and modular quick-change tooling are shaping the evolution of the manual compact crimper market.
Field installations of utility-scale solar arrays demand continuous, heavy-duty terminations of MC4 contacts under harsh ambient conditions. The SIBO SO-2546 and SN-2546B series deliver repeatable micro-indentation that guarantees thermal stability under continuous 1500V DC operating voltages.
Modern electric vehicles and autonomous sensor suites deploy microscopic open-barrel contacts (Molex Micro-Fit, JST, AMP) where manual errors can trigger communication bus failures. Our high-precision SN-58B tools provide dual-action folding for wire and insulation jackets simultaneously.
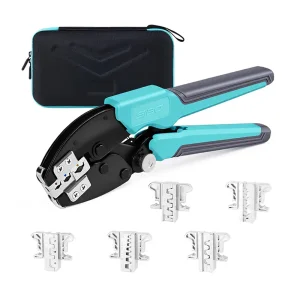
Technicians increasingly reject carrying multiple single-purpose crimpers into high-altitude or confined panel workspaces. SIBO's patented magnetic jaw quick-replacement sets allow switching from insulated sleeves to non-insulated lugs in under three seconds with absolute zero backlash.
In-depth responses covering mechanical tolerances, tool life cycles, international shipping compliance, and private-label production minimums.
Versatile European-standard pliers, quick-replace multi-jaw sets, and closed-barrel automotive crimpers built for demanding daily field service.