Engineered to international mechanical compliance standards (IEC 60947-7-1 / DIN 46228). Explore factory-direct ratcheting, self-adjusting, and quick-change crimping systems.

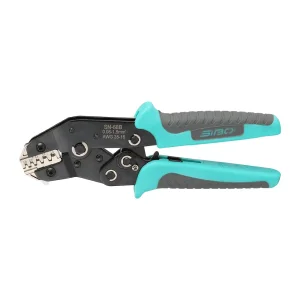
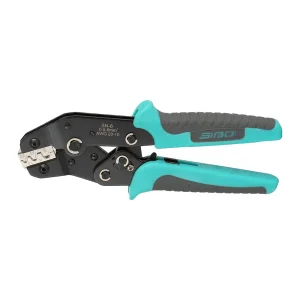
In modern industrial wire harness assembly, switchgear engineering, and renewable energy integration, crimped electrical terminations represent the critical nexus between safety, longevity, and electrical efficiency.
Precision crimping does not merely hold stranded copper wires; it subjects the ferrule sleeve and conductors to calculated plastic deformation. Our factory tooling is calibrated to achieve a solid conductor compaction density exceeding 85%, eliminating microscopic air voids that cause contact resistance increases, galvanic oxidation, and thermal runaway.
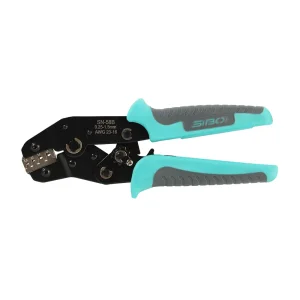
Human error accounts for over 72% of field termination faults. SIBO crimping mechanisms integrate precision carbon steel ratchets with calibrated pressure releases. The tool's synchronized eccentric cam requires full-stroke completion before releasing, guaranteeing that mechanical force curves are strictly replicated on every cycle.
Crimper jaws operate under cyclic shear and compressive pressures exceeding 15 kN/cm². We forge dies from vacuum-degassed Cr12MoV, AISI 4140, or high-carbon alloy steel, hardened via controlled vacuum quenching to 58–62 HRC. This prevents premature cavity deformation and maintains tolerance accuracy through 50,000+ operations.
Located in Yueqing, Zhejiang—the global capital for low-voltage electrical apparatus—our facility leverages an ultra-dense, vertical supply network delivering rapid prototyping, material trace assurance, and cost-efficient economies of scale.
Yueqing's specialized ecosystem guarantees direct proximity to premier cold-rolled strip steel mills, specialized heat-treatment plants, and precision CNC EDM facilities within a 15-kilometer radius. This geographic compression cuts supply chain lead times by 65% compared to fragmented global competitors, providing robust resilience against logistics bottlenecks.
Our tooling frames are blanked from high-tensile structural alloy steel using 250-ton automated stamping presses. Die cavities are cut via Japanese and Swiss high-precision wire-cut EDM machinery, ensuring microscopic tolerances that prevent conductor pinching, burr formation, or unequal pressure distribution across ferrule terminal barrels.
Quality assurance is embedded at each manufacturing stage. From spectral analysis of incoming steel batches to coordinate measuring machine (CMM) verification of die geometries, every production run is monitored using real-time Cp and Cpk capability indexes (targeted at Cpk > 1.33) to safeguard zero-defect supply to tier-1 OEMs.
Wire ferrule termination has evolved from basic indent crushing into mathematically calculated geometric profiles that correspond with modern push-in spring cage terminal blocks (such as WAGO, Phoenix Contact, and Weidmüller).
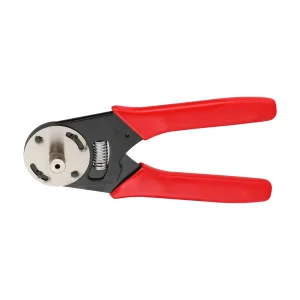
Square crimping profiles produced by self-adjusting 4-jaw systems provide flat contact surfaces on all four quadrants. This profile is engineered for rectangular clamp cages, ensuring maximum contact area and zero wire strand displacement. Recommended for control cabinets and automation racks handling wire cross-sections up to 16 mm² (AWG 5).
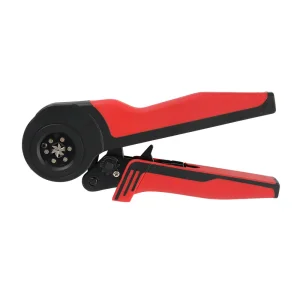
Hexagonal crimping delivers a near-circular cross-section, ideal for compact, rounded terminal chambers such as modern push-in terminal blocks and miniature circuit breakers. By distributing inward mechanical pressure through six dynamic sliding steel segments, hexagonal tools eliminate protruding edges and prevent insertion jams in dense DIN-rail enclosures.
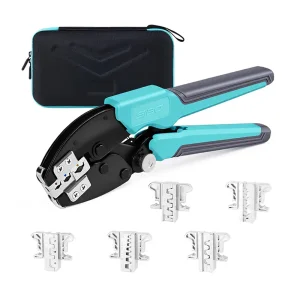
Modern field technicians and assembly lines demand tooling versatility without sacrificing mechanical rigidity. Our patented magnetic-retained jaw frames allow toolless die swaps in under 5 seconds, combining automotive Deutsch DT closed-barrel cavities, open-barrel B-crimps, insulated lugs, and solar MC4 dies on a single calibrated chassis.
| Profile Geometry | Primary Standards | Applicable Cross Sections | Ideal Application Terminal Blocks | Pull-Out Retention (IEC 60947-7-1) |
|---|---|---|---|---|
| Square (4-Jaw) | DIN 46228 Part 1 & 4 | 0.08 – 16.0 mm² (AWG 28–5) | Rectangular screw cages, modular industrial switchboards | Exceeds standard threshold by >35% |
| Hexagonal (6-Jaw) | DIN 46228 Part 4, UL 486F | 0.25 – 10.0 mm² (AWG 23–7) | Push-in spring cage connections, compact automation blocks | Exceeds standard threshold by >40% |
| Trapezoidal Indent | EN 60999-1, NF C 63-023 | 0.50 – 50.0 mm² (AWG 20–1/0) | High-current distribution feeds, motor control terminal posts | Exceeds standard threshold by >45% |
| B-Type Open Barrel | SAE AS7928, USCAR-21 | 0.05 – 6.0 mm² (AWG 30–10) | Automotive wiring harnesses, computer headers (Molex/JST) | Meets 100% USCAR pull-off criteria |
From extreme thermal cycles in photovoltaic fields to high-vibration automotive drive units, SIBO crimping instruments meet demanding operational environments worldwide.
Photovoltaic installations operate under UV radiation, seasonal thermal swings (-40°C to +90°C), and continuous 1500V DC loads. Loose or improper solar crimps lead to arcing and field fires. Our SO-2546C Pro and SO-2546B Pro solar tools feature EDM-machined die pockets for 2.5, 4.0, and 6.0 mm² MC4 connectors, ensuring low contact resistance and moisture-tight cold compression.
Automotive electronics require fault-free signal paths under severe mechanical vibration. For Deutsch closed-barrel solid contacts and open-barrel JST/Molex connections, our 4-indent and micro B-crimp systems control conductor roll-over, wire core compression, and insulation strain relief without shearing micro-strands.
Panel builders make thousands of ferrule terminations per week. Hand strain and fatigue lead to inconsistent torque, loose strands, or incomplete jaw closure. Our self-adjusting ergonomic crimpers (SO 16-6 and SO 10-4) integrate short handle spans, multi-lever compound pivots, and self-adaptive jaws, lowering operator force input by 35%.
Purchasing directors, private-label brands, and multinational hardware importers evaluate Chinese hand-tool suppliers on regulatory alignment, batch-to-batch repeatability, and total cost of ownership (TCO).
Every tool and die design from SIBO undergoes compliance testing matched to target market requirements. Our systems are verified against IEC 60947-7-1 for electrical terminal pull-out tension, DIN 46228 (Parts 1-4) for ferrule compression specifications, UL 486F standards, and EU RoHS/REACH environmental compliance for non-toxic ergonomic handle polymers.
We provide full-spectrum engineering for international tool distributors, retail chains, and hardware brands. Services include two-tone injection handle customization (TPR/PP blends), fiber-laser brand marking, custom die profile development for proprietary terminals, and tailored retail packaging (blister packs, molded carry cases, Oxford canvas tool rolls).
We trace every manufacturing run from raw steel heats to finished tool assembly. Digital micrometer data and hardness test reports are logged per production lot. Wear components such as ratchet teeth, pawls, and eccentric adjusters undergo endurance cycling to guarantee long service life for your end customers.
Explore specialized solar PV crimping pliers, miniature European-style pre-insulated terminal tools, classic high-leverage indent crimpers, and heavy-duty industrial models.
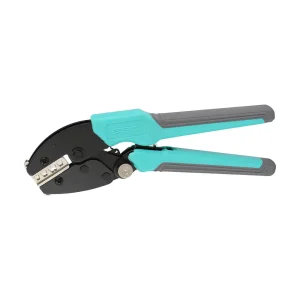
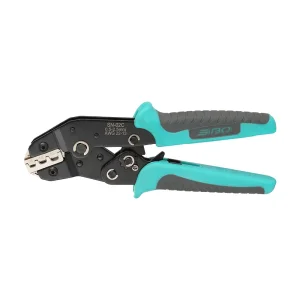
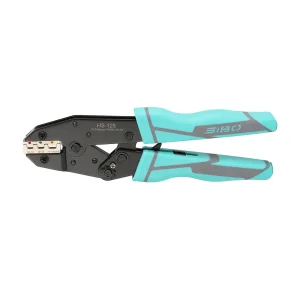
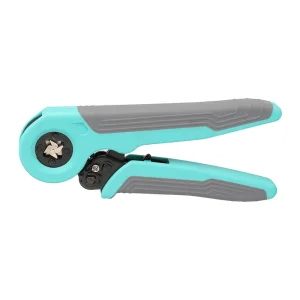
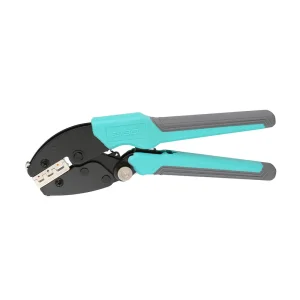
Comprehensive engineering guidance on mechanical crimp standards, die cavity selections, and global supplier qualification.
