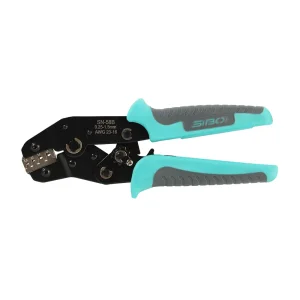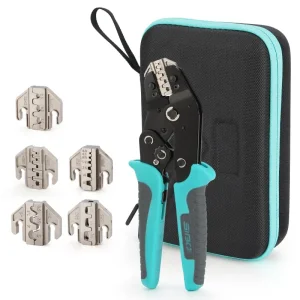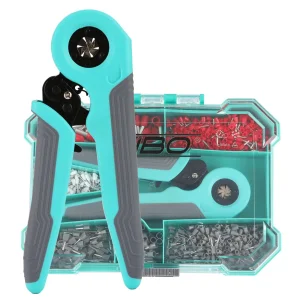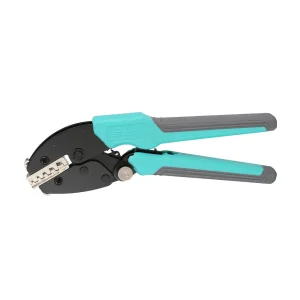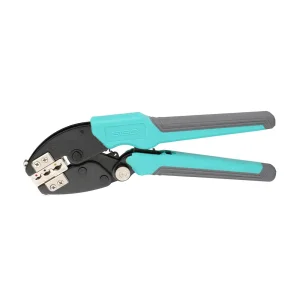
Industrial ratcheting mechanisms, German-standard self-adjusting crimpers, and heavy-duty cable cutters engineered for zero-defect wire termination.
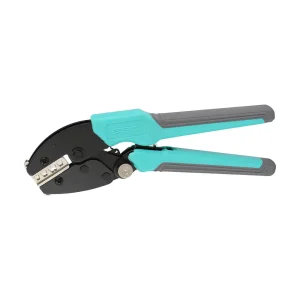
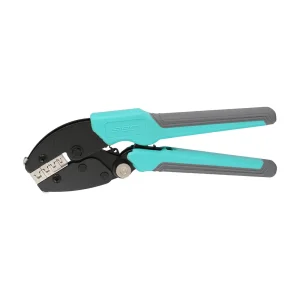

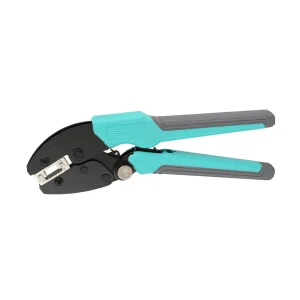
A strategic breakdown of procurement criteria across high-reliability international commercial and infrastructure sectors.
Global utility-scale solar generation demands continuous, zero-loss electrical connectivity. Tooling specifications mandate full-cycle ratcheting actions that guarantee consistent micro-ohm terminal resistance under harsh UV and mechanical vibration conditions, compliant with IEC 62852 standards.
Tier-1 automotive wire harness manufacturing demands precision-toleranced open-barrel crimpers and solid barrel indent crimp solutions capable of processing high-gauge copper cabling without damaging delicate silicone seals or terminal retention tabs, meeting USCAR-21 specifications.
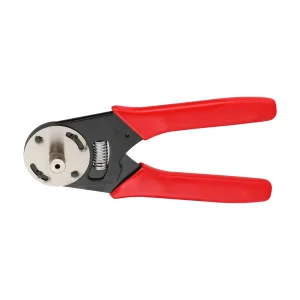
Switchgear builders and system integrators require self-adjusting ferrule crimping pliers that seamlessly adapt to cross-sections from 0.08 mm² to 16 mm². This eliminates tool switching, accelerating production line speeds while ensuring standardized DIN 46228 square and hexagonal profiles.
Inside the Yueqing Sibo manufacturing ecosystem: Tooling alloys, thermal processing, and mechanical force multiplication.
| Tool Engineering Parameter | Material / Structural Specification | Testing & Compliance Protocol | Operational Impact |
|---|---|---|---|
| Crimp Die Jaws | AISI 4140 Chromium-Molybdenum Alloy / Powder Metallurgy | Vacuum oil quench, Hardness Rockwell C (HRC) 48–52 | 50,000+ cycle wear life with zero profile divergence |
| Leverage Chassis & Arms | High-Tensile Cold-Rolled Carbon Structural Steel (Q235/50CrV4) | 3-point mechanical bending load test up to 4,500 N | Translates low hand-effort into massive crimping pressure |
| Ratcheting Assembly | High-Carbon Steel Gear Wheel with Emergency Quick-Release Cam | Full cyclic tooth-mesh fatigue test per EN 60352-2 | Eliminates partial-cycle errors; failsafe operator mechanism |
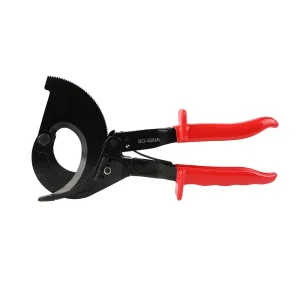
| Cutting Blades (Cutters) | Forged SK5 High-Carbon Spring Tool Steel / Manganese Steel | Induction edge-hardening, laser sharpness validation | Clean, shear-action cutting without copper conductor flattening |
| Ergonomic Hand Grips | Dual-Compound High-Impact Polypropylene (PP) + Thermal Plastic Rubber (TPR) | Drop impact tested at -20°C and chemical solvent soak | Reduced musculoskeletal operator fatigue and anti-slip tactile grip |
A closed-loop manufacturing paradigm spanning five integrated steps, leading future hand tool innovation.
Every crimping cavity begins with 3D CAD modeling and digital compression stress simulation. We design specialized geometries matching insulated flags, closed barrels, or MC4 terminals to prevent conductor strand slippage and barrel splitting.
Tooling jaws are shaped through slow-feeding wire EDM and multi-axis CNC milling, securing dimensional tolerances within ±0.005 mm. This exactness guarantees die symmetry and uniform pressure distribution across terminal barrels.
During chassis assembly, ratcheting pawls are adjusted and tension-tested. Full cyclic engagement guarantees that crimp mechanisms cannot be prematurely disengaged until the terminal attains its terminal compression height.
Finished batch runs undergo destructive tensile separation tests and microscopic microsectioning analysis to ensure electrical junctions exceed international pull-off values specified by UL 486A-486B and DIN EN 60352-2.
SIBO’s technical roadmap integrates wireless Bluetooth cycle-counters, electronic force verification, and real-time maintenance alert modules inside industrial hand tools for mission-critical aircraft and rail harness plants.
A dependable bridge between Yueqing's industrial manufacturing power and global commercial hardware distribution channels.
We transform your brand concept into market-ready retail products: dual-color injection-molded brand handles, laser-engraved logo positioning, customized die matrix cavities, and retail-ready Oxford carrying bags or clamshell blisters.
All Yueqing Sibo wire strippers, ratchet pliers, and cable cutters are manufactured under certified ISO 9001 quality systems. Products meet CE directives, RoHS environmental guidelines, and REACH chemical standards for friction-free EU and US importation.
Benefiting from our location in Yueqing, Zhejiang—China’s epicenter for electrical apparatus—we streamline container logistics via Ningbo and Shanghai ports. Direct video inspection, comprehensive QA inspection sheets, and bilingual technical support are provided with every shipment.
In-depth responses from our senior tool design engineers for distributors, electrical wholesalers, and product managers.
Providing precision crimpers, custom stripping kits, and private-label contract manufacturing for leading global electrical supply names.
Multi-jaw modular kits, closed barrel micro-crimp assemblies, and heavy-gauge ferrule systems tailored for demanding OEM field kits.