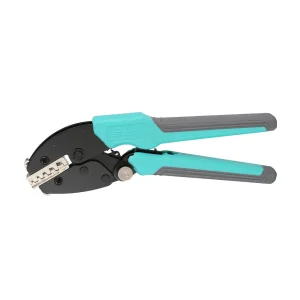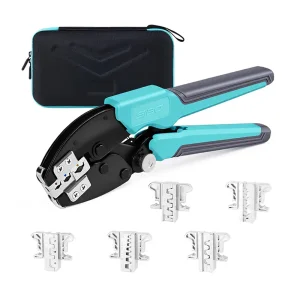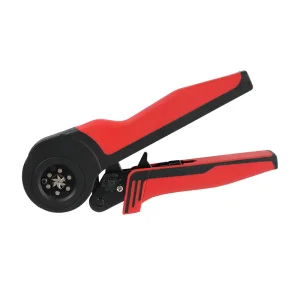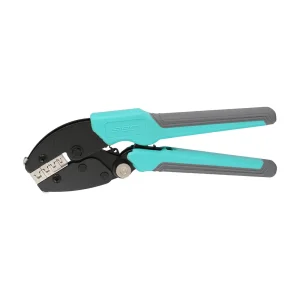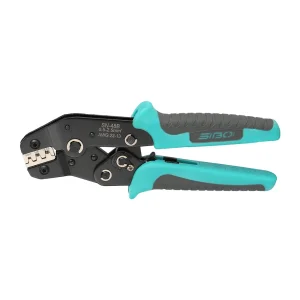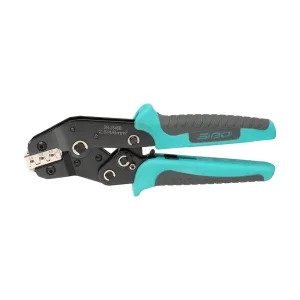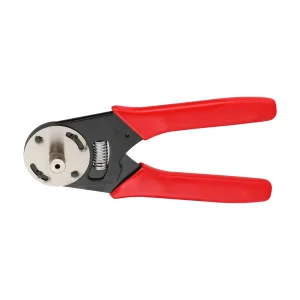
Designed in Yueqing’s electrical core, these high-reliability crimpers combine micro-machined die profiles with anti-fatigue mechanisms to guarantee microscopic cold-weld crimping integrity.

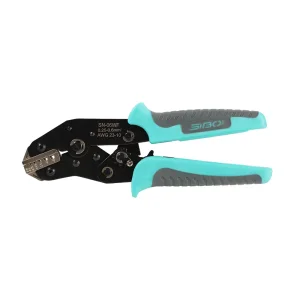
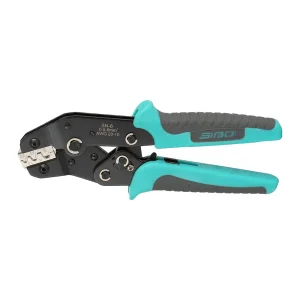
In modern electrical design, the terminal crimp is no longer classified as a simple mechanical friction joint. Under high-frequency current profiles, harmonic distortions, and harsh environmental thermal cycling, improper crimping leads directly to terminal overheating, micro-arcing, and fatal resistance buildup. As electrical architecture evolves toward higher voltages—seen markedly in 800V/1000V electric vehicle powertrains, 1500V DC photovoltaic combiner boxes, and hyperscale edge-computing data servers—the demand for repeatable, gas-tight metallurgical compression has transformed terminal crimper manufacturing.
Traditional manually operated pliers often introduce unpredictable human variances: inconsistent closing force, premature tool release, and die alignment errors. These defects create voids between copper strands, initiating oxidation, hot-spots, and rapid contact failure. Modern manufacturing standards dictated by IEC 60352-2, UL 486A-486B, and DIN EN 60947-7-1 require crimp profiles to achieve an optimal degree of conductor compaction (typically 80% to 85% solid metal mass density) without severing individual wire strands.
| Connection Architecture | Standard Jaw Geometry | Compaction Density Target | Typical Mechanical Pull-Out Limit | Core Industrial Risk Mitigated |
|---|---|---|---|---|
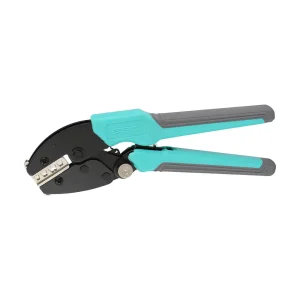
| Pre-Insulated (SO-30J / SO-125) | Double-Cavity Oval Contoured | > 78% Metal Fill Ratio | UL 486A Compliance (>150N for 2.5mm²) | Insulation wall rupture & conductor cold-shear |
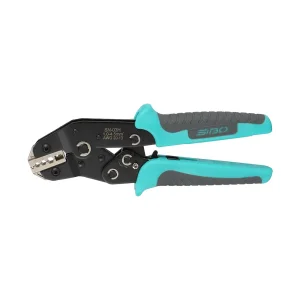
| Open-Barrel F-Crimp (SO-04BPro) | Symmetrical B-Type Serrated | > 84% Gas-Tight Compression | IEC 60352-2 Category B Standard | Strand pullout, fretting corrosion, micro-sparking |
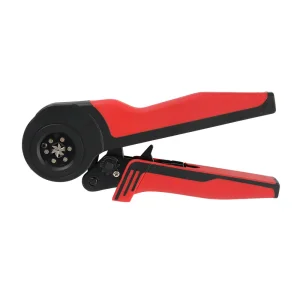
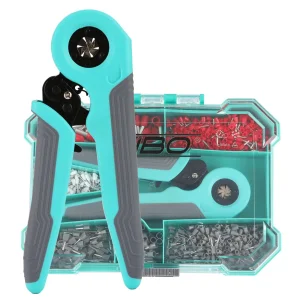
| End-Ferrules (SO-16-6 Hexagonal) | 6-Synchronized Segmental Jaws | > 82% Homogeneous Bundle | DIN 46228 Part 1/4 Structural Integrity | Stray strand short-circuits & terminal block damage |
| PV Solar MC4 (SO-2546B Pro) | Segmented Step-Down Die Cavity | > 88% Core Compaction | TÜV / UL 6703 Photovoltaic Proofing | Arc-faults caused by 1500V DC resistance heating |
To consistently hit these tight mechanical pull-out benchmarks, contemporary manufacturers in Yueqing, China have transitioned completely from stamping low-carbon iron to executing high-vacuum hot die-forging, employing 42CrMo and SCM440 alloy steels, and machining crimp cavities via ultra-low-speed wire Electrical Discharge Machining (EDM). The outcome is an industrial-tier terminal crimper line that eliminates erratic operator behavior through integrated multi-tooth ratchets, precise cycle calibration, and ergonomic lever-assist linkages.
Located in Yueqing—the epicentre of global low-voltage electrical apparatus—SIBO Tools integrates digital manufacturing, automated metallurgical testing, and agile engineering response.
Our die sets undergo computer-controlled Slow-Feeding Wire Cut EDM processes that ensure cavity tolerances within ±0.005mm. This extreme precision delivers uniform cross-sectional compression across every AWG step.
Operating inside Yueqing provides zero-mile supply integration with cold-heading foundries, high-spec heat treatment centers, and non-ferrous raw metal specialists, significantly reducing lead times for OEM projects.
Every batch undergoes destructive tensile pull testing using calibrated dynamic load cells, cross-section metallurgical imaging, and Vickers microhardness profiling (HRC 42-45 frame, HRC 58-62 jaw cavities).
A deep dive into the engineering and compliance metrics evaluated by European and North American distributors when choosing a long-term China tooling partner.
Ensure that the supplier utilizes true progressive-lock mechanisms that prevent release until the toggle passes the center-cam point. This entirely eliminates under-crimped lugs resulting from worker fatigue.
Professional tools require an accessible eccentric adjustment wheel on the chassis. This allows calibration technicians to re-torque the leverage system after 5,000 cycles, extending operational lifespan.
Modern field technicians crimp hundreds of joints per shift. Procuring tools with dual-injection thermoplastic rubber (TPR) and Santoprene handles reduces operator strain and eliminates carpal vibration risks.
SIBO’s comprehensive crimper families are verified in high-stress, mission-critical infrastructure around the globe.
Photovoltaic installations operate under intense UV and severe thermal expansion. Our SO-2546B/C Pro tools ensure that solar cables maintain ultra-low contact resistance (<0.2mΩ), protecting against thermal arcing.
Engine bays and chassis wiring harnesses experience continuous mechanical vibration. Our SO-04BPro and SN-48B open-barrel tools deliver flawless dual B-crimps—one grasping the copper core and the other securing insulation strain-relief.
High-density automated cabinets demand ultra-compact wire preparation. SIBO’s self-adjusting hexagonal crimpers (SO-16-6) compress wire ferrules into symmetrical geometries that slide seamlessly into cage-clamp terminals.
Direct engineering clarity addressing terminal compatibility, die metallurgical metallurgy, and custom OEM manufacturing workflows.
From multi-jaw magnetic replacement sets to specialized flag and open-barrel systems, discover tools engineered for relentless production uptime.