
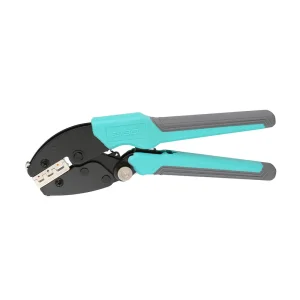
Precision-machined ratchet mechanisms, self-adjusting ferrule dies, and European-style mini pliers calibrated for zero-defect wire termination across high-volume production facilities.
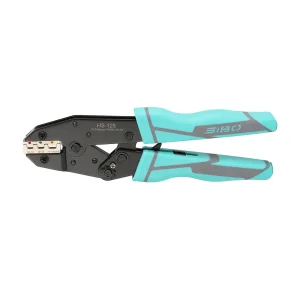

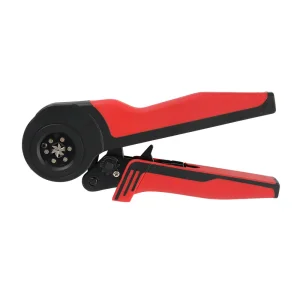
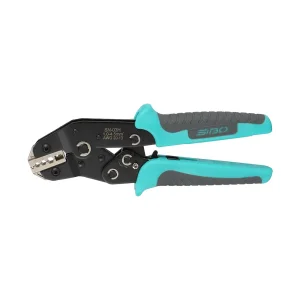
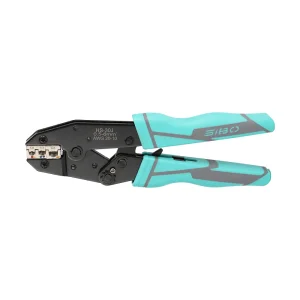
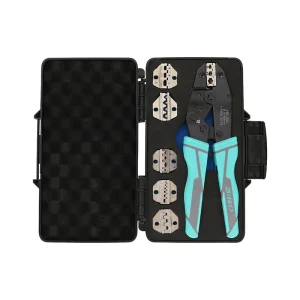
In modern electrical engineering, wire termination integrity defines system safety, contact resistance, and long-term operating durability. Global Tier-1 supply chains can no longer tolerate loose tolerances or unpredictable manual hand tools.
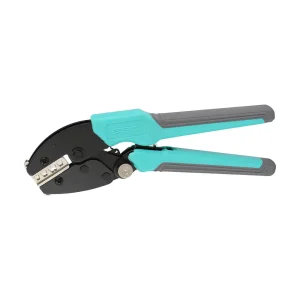
Procurement engineers in high-reliability sectors mandate crimp geometries compliant with UL 486A-B and DIN EN 60352-2. A crimper must achieve optimal mechanical compaction without cutting copper strands. Our calibrated ratchet design ensures complete jaw closure before disengagement, eliminating human error in shift work.
The tool life and crimp profile depend entirely on die manufacturing. Yueqing Sibo utilizes vacuum-heat-treated 40Cr and SCM440 alloy steels with precision slow-wire electrical discharge machining (WEDM). This ensures die cavity tolerance within ±0.015mm, preventing flashing, uneven ears, or barrel fracture under load.
Assembly line workers execute between 1,500 and 3,000 crimping operations per shift. Enterprise procurement standards prioritize compound mechanical advantage designs that lower hand squeeze force by over 35%. Dual-component thermoplastic rubber (TPR) grips provide anti-slip tactile comfort and resist shop chemicals.
A gas-tight connection requires an electrical contact surface compaction ratio between 80% and 85%. Over-crimping reduces the cross-sectional area and weakens mechanical tensile strength, while under-crimping creates micro-gaps that corrode, increase millivolt drops, and create thermal hot-spots in industrial switchgear.
Customized crimping geometry across renewable power grids, automotive harness plants, mission-critical aerospace testing, and low-voltage distribution assemblies.
High-voltage 1500V DC strings in utility-scale solar farms demand ultra-low contact resistance to prevent field fires. Models such as the SO-2546C Pro provide dedicated locator pins and dual-stage dies engineered for MC4 contacts across 2.5mm², 4mm², and 6mm² cross-sections.
Open-barrel mini crimping tools like the SN-48B and SO-04BPro deliver standardized "B-crimp" / "F-crimp" profiles. The wire strands are compressed into a hexagonal density block while the rear insulation wings wrap smoothly without rupturing the silicone jacket.
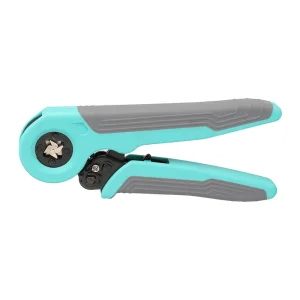
Compact PLC terminals and high-density DIN-rail terminal blocks rely on bootlace ferrules. SIBO's self-adjusting crimpers (SO 16-6 and SO 10-4) apply multi-wedge radial pressure, turning stranded conductors into compact square or hexagonal pin geometries.
Sub-miniature D-sub contacts and signal wiring for telecommunication relays necessitate low-tonnage, micro-increment ratchets. SN-series mini pliers prevent neck thinning and terminal bend, maintaining RF and data integrity under continuous vibration.
Evaluate standard tool parameters against international engineering baselines to streamline corporate RFQs and supplier selection.
| Tool Series | Terminal Suitability | Wire Gauge Range | Die Material / Hardness | Ratchet Mechanism | Compliance Standards |
|---|---|---|---|---|---|
| SO-125 / SO-30J Pro | Pre-insulated terminals (rings, spades, bullets) | 0.5 – 6.0 mm² (AWG 22–10) | AISI 4140 Steel / HRC 43–46 | Full-cycle ratchet with manual emergency trip | DIN EN 60352-2 |
| SO-10 Pro | Non-insulated copper lugs & ring terminals | 1.5 – 10 mm² (AWG 16–7) | Forged 40Cr Alloy / HRC 45–48 | High-leverage compound ratchet lever | UL 486A-B |
| SO 16-6 & SO 10-4 | End wire ferrules (bootlace ferrules) | 0.08 – 16 mm² (AWG 28–5) | Precision Sintered / HRC 44–47 | Self-adjusting radial hexagonal / square | DIN 46228 Part 1-4 |
| SO-2546C Pro | Solar MC4 photovoltaic pin contacts | 2.5 / 4.0 / 6.0 mm² (AWG 14–10) | Wire-cut Carbon Steel / HRC 46–49 | Direct pressure die with locator assist | TÜV / IEC 62852 |
| SN-48B / SO-04BPro | Open-barrel terminals (AMP, Molex, JST styles) | 0.14 – 1.5 mm² (AWG 26–16) | Fine-blanked SCM440 / HRC 42–45 | Two-step B-crimp roll indentation ratchet | IPC/WHMA-A-620E |
Integration of micro-strain sensor interfaces inside the tool frame to monitor real-time clamping peak pressure during industrial harness runs, feeding assembly data to MES systems.
Research into high-yield aluminum-titanium alloy forgings to reduce tool weight by 42% while retaining 12kN compressive strength, eliminating hand and wrist tendon strain among electrical operators.
Patented tool-free push-button jaw retention mechanisms allowing tool operators to switch between insulated, non-insulated, and solar dies in under 4 seconds without misplacing fasteners.
Understanding supply chain clusters, cost dynamics, and why over 70% of the world's hand-held terminal crimpers trace their core toolmaking origins to Zhejiang's electrical industrial heartland.
Known globally as China's electrical capital, Yueqing concentrates thousands of terminal manufacturers, steel suppliers, stamping houses, and heat treatment facilities within a 30-kilometer radius. SIBO leverages this localized supply web to achieve unprecedented tooling turnarounds, reduced component lead times, and economies of scale.
While Western buyers explore nearshoring in Eastern Europe or Mexico, toolmaking remains restricted by shortages of specialized tool-and-die craftsmen. Partnering directly with audited Yueqing manufacturers delivers the dual benefit of advanced CNC machining precision alongside rock-solid container-load delivery consistency.
Fluctuations in tool steel and plastic polymers can disrupt profit margins for overseas brands. SIBO maintains long-term billet reserves and computerized stamping dies that maximize raw sheet utilization, shielding our distributor network from unexpected price shocks during raw material market swings.
Every batch of crimping pliers undergoes rigorous quality gatekeeping to satisfy international environmental directives, occupational ergonomics, and cross-border safety standards.
All handle grips and surface finishes are formulated to be free from lead, mercury, cadmium, and hexavalent chromium. Full chemical spectrum testing confirms compliance for distribution across the European Union and North America.
Our in-house QA laboratory executes daily destructive tensile pull tests using motorized testers to guarantee that crimped joints meet or exceed the minimum pullout force values specified under UL and CSA certifications.
The factory implements continuous Kaizen and 5S workflows. Complete lot traceability ensures that each production batch can be tracked from raw carbon steel coils to final optical coordinate measuring machine (CMM) die verification.
We provide end-to-end private labeling support, including fiber laser handle etching, corporate Pantone grip molding, retail blister or Oxford bag kit creation, and direct DDP shipping to European and American 3PL warehouses.
From open-barrel harness crimpers to MC4 photovoltaic tools and energy-efficient insulated terminal pliers — factory-direct configurations built to buyer specifications.
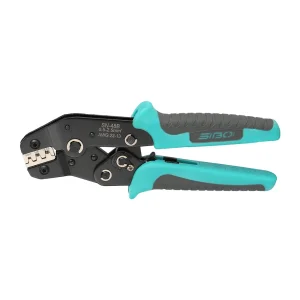
Clear engineering insights addressing die tolerances, tensile certification, ratchet calibration, and custom OEM tool runs.