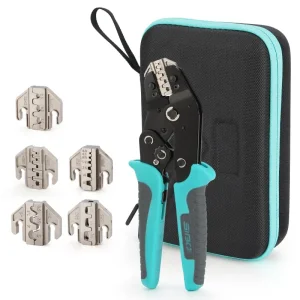
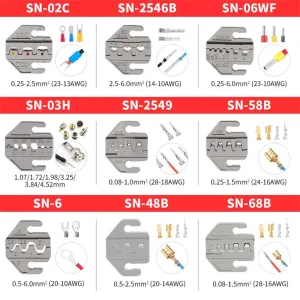
Explore our industrial-grade crimping solutions designed for rigorous manufacturing workflows, repeatable pull-force ratings, and minimal contact resistance.


Addressing the shifting paradigm from manual harness assembly to high-tonnage semi-automated terminal processing across global EV, renewable energy, and grid infrastructure sectors.
Electric mobility mandates thick-gauge cabling ranging from 35mm² to 120mm² and beyond. A custom 15-ton benchtop crimper delivers the uniform hydraulic compression needed to meet strict automotive cross-section void ratios below 5%.
Utility-scale photovoltaic farms, BESS (Battery Energy Storage Systems), and wind turbines demand heavy lugs crimped to perfection to avoid thermal hotspots and terminal oxidation under continuous mega-watt loads.
Manual handheld tooling introduces operator fatigue and variance. Tier-1 harness factories utilize bench crimpers to ensure mechanical repeat rates up to 1,200 cycles per hour while integrating full-cycle force recording.
A comprehensive breakdown of force-displacement monitoring, metallurgical die tooling, and smart factory compatibility.
| System Attribute | Standard Bench Unit | Custom 15-Ton Factory Configuration | Compliance / Verification |
|---|---|---|---|
| Nominal Clamping Force | 60 kN - 100 kN | 150 kN (15.3 Metric Tons) ± 1.5% | ISO 6722 / USCAR-21 / DIN 46235 |
| Stroke Travel Distance | 20 mm - 35 mm | 45 mm Adjustable with Micrometer End-Stop | Digital Linear Encoder Feedback |
| Cycle Duration | 3.5 - 5.0 seconds | 1.8 - 2.4 seconds (Dual-stage Hydraulic Pump) | Continuous Production Benchmarked |
| Conductor Capacity | 0.5 mm² - 50 mm² | 10 mm² up to 300 mm² (Copper & Aluminum Lugs) | IEC 60352-2 / UL 486A-486B |
| Crimp Force Monitoring (CFM) | Not included or analog dial | Dynamic Multi-Zone Piezoelectric Load Cell | MES Integration via OPC-UA / Modbus |
| Die Tooling Metallurgy | Standard Carbon Steel | SKD11 / DC53 Vacuum Hardened (HRC 60-62) | Extreme Wear Resistance (>150,000 cycles) |
Modern 15-ton bench crimpers interface directly with Industry 4.0 shopfloor systems to log stroke profiles, peak pressures, and operator IDs.
Integrated optical safety grids disable the hydraulic actuator instantly if an operator's hands breach the tooling perimeter.
Hybrid electro-pneumatic actuation speeds up pre-clamping, cutting overall cycle times down to less than 2 seconds.
Tool-less die swap systems reduce changeover downtime from 20 minutes to under 90 seconds across multiple lug configurations.
Empirical performance indicators recorded across verified industrial plant installations worldwide.
Eliminating operational vulnerabilities with international field calibration, genuine wear parts distribution, and full regional certification.
Every customized bench crimper adheres to EU machinery directives, low-voltage regulations, and emergency stop fail-safe mandates.
We maintain verified service relationships throughout North America, Central Europe, and East Asia for on-site load cell re-certification.
Our rapid-prototyping centers manufacture custom wire profile dies within 5 business days, dispatched with comprehensive metallographic test logs.
Insights directly from our chief hydraulic engineers and industrial procurement specialists.
Heavy wire gauges (70mm² to 300mm²) require sufficient plastic deformation of both the terminal barrel and the copper strands. A 15-ton system provides the compaction force necessary to remove inter-strand voids, delivering gas-tight connections with zero micro-corrosion risk over decades of service.
CFM captures the force-displacement curve in real-time during every compression stroke. If missing strands, incorrect terminal thickness, or loose wire insertion are detected, the system halts operation immediately, flags the defect, and prevents the operator from removing the harness until authorized.
Yes. Our in-house CAD/CAM tooling department manufactures customized die geometries from high-hardness tool steels (such as SKD11 and DC53), precision-engineered to your connector CAD models and exact cross-sectional requirements.
Preventive maintenance includes hydraulic fluid replacement every 1,000,000 cycles or 12 months, linear guide re-greasing every 25,000 cycles, and annual re-calibration of the internal piezoelectric load cell against traceable ISO standards.
Complete your production setup with heavy-duty cable preparation cutters, open-barrel ratchets, and modular jaw assemblies.