Verified factory production lines featuring micro-tolerance jaws, calibrated full-cycle ratchet ratcheting levers, and heat-treated die sets.

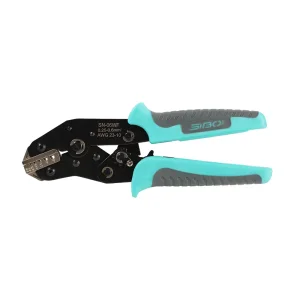
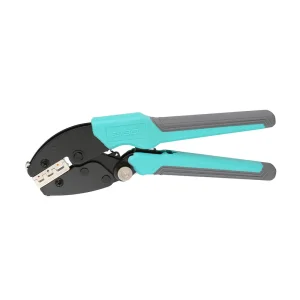
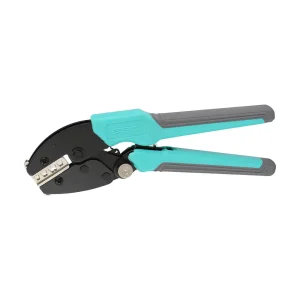
Understanding the microstructural mechanics, mechanical leverage kinematics, and metallurgy that separate consumer tools from high-integrity factory crimpers.
The primary thermodynamic and mechanical objective of an industrial cable lug crimper is achieving a true gas-tight joint. By generating controlled plastic deformation of the lug barrel and copper strands, the tool eliminates air voids. This eliminates galvanic oxidation and thermal cycling resistance spikes inside the termination.
Dies and high-stress load pivot levers are forged from vacuum-degassed structural alloy steels (40Cr, AISI 4140, or high-carbon SKD11). Die cavities undergo slow-feed Wire EDM cutting with profile tolerances held within ±0.015mm, followed by multi-stage vacuum heat treatments.
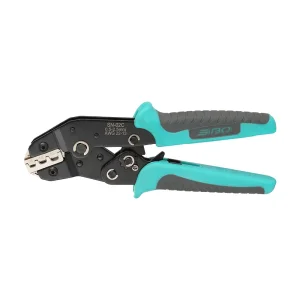
SIBO precision hand tools feature high-mechanical-advantage compound pivot levers with integrated ratchets. An integrated eccentric pin enables periodic adjustment to compensate for mechanical wear, guaranteeing identical crimp heights across a tool's 50,000-cycle certified lifespan.
In electrical joints, inadequate crimping pressure leads to loose strand packing, high electrical resistance, localized heating, and fire hazard. Over-crimping thins the terminal barrel wall, causing work hardening and strand shear. Yueqing Sibo Tools engineers every die profile specifically around DIN 46235 (heavy-duty copper lugs), DIN 46234, and UL 486A-486B standards to achieve cold fusion between strands without wall fracturing.
Why sourcing custom cable lug crimpers directly from Yueqing, Zhejiang—the global capital of low-voltage electrical apparatus—delivers unmatched cost-to-performance advantages.
Yueqing consolidates over 60% of China's electrical hardware component suppliers within a 15-kilometer radius. Raw alloy supply, cold rolling, precision investment casting, and tool steel forging are secured on just-in-time schedules with zero inter-provincial freight overhead.
With localized mold-making shops, tooling iterations for proprietary client lug shapes take 7 to 14 days rather than months. Custom extrusion dies, injection molds for TPR soft handles, and laser-marking fixtures operate at direct manufacturing costs unreachable in Western hubs.
SIBO enforces dual-stage quality checking: incoming raw steel spectrographic analysis, hardness testing post-quenching, automated coordinate measuring machines (CMM) for die cavity geometry, and mechanical destructive pull-out force validation before batch export.
Proximity to Ningbo-Zhoushan Port and Shanghai Port provides seamless weekly container vessel sailings to Rotterdam, Hamburg, Los Angeles, Dubai, and Busan. Lead times from factory assembly to ship departure are compressed into predictable logistics schedules.
How Fortune 500 electrical tool brands, tier-1 utilities, and private-label distributors structure custom manufacturing runs with Yueqing Sibo Tools.
| Procurement Parameter | Standard Catalog SKU | OEM Private Label Tier | ODM Custom Development |
|---|---|---|---|
| Typical Order MOQ | 100 - 500 Pieces | 1,000 - 2,500 Pieces | 3,000 - 5,000 Pieces (Die Cost Amortized) |
| Die Cavity Customization | Standard DIN / AWG / Solar Sizes | Custom Laser Markings & Cavity Labeling | Full Bespoke Wire EDM & Stamping Geometry |
| Ergonomic Grip Design | Standard Dual-Color PVC / PP | Custom Pantone Two-Tone TPR Soft Grips | Bespoke Molded Grips with Anti-Slip Textures |
| Packaging Configurations | SIBO Blister Card or Industrial Box | Private Brand Color Box / Dual Blister | Blow-Molded Cases / Oxford Bags / Master Kits |
| Factory Testing Documentation | Batch QC Pass Certificate | Mill Test Reports & Hardness Verification | PPAP Level 3, Tensile Curves, Cpk > 1.33 Reports |
We work under enforceable B2B Non-Disclosure Agreements (NDAs). Proprietary customer die designs, handle contour CAD files, and retail graphic packaging remain the exclusive property of the commissioning partner.
Every tool handle and die set can be laser-etched with client trademarks, model codes, terminal cross-section ratings (AWG/mm²), and manufacturing traceability date codes for industrial asset management.
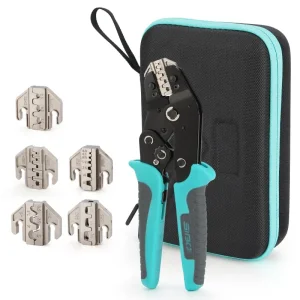
Distributors frequently build multi-die field service kits pairing a master ratchet frame with 4 to 8 interchangeable quick-swap jaws, terminal assortments, and precision cable cutters housed in custom-stitched, heavy-duty ballistic Oxford cloth bags.
How the green energy transition, smart grid expansion, and digital factory initiatives are driving innovation across manual and hydraulic crimping hand tools.
Utility-scale photovoltaic farms are standardizing on 1500V DC architectures to minimize transmission losses. This shift demands tighter crimp height tolerances on MC4-compatible and Stäubli solar contacts. SIBO's SO-2546 series provides multi-point crimping to stop thermal hot spots.
Electric vehicle battery management systems and charging infrastructure require dual-stage hexagonal and indent crimps that bind both conductor strands and braided EM shielding in a single mechanical stroke, preventing electromagnetic interference.
Field electricians no longer accept screwdrivers to swap jaws. Next-generation tools use magnetic detention ball locks and push-button release mechanisms, allowing die swaps in under three seconds with zero screw loss on site.
Matching specific cable lug geometry, conductor stranding, and environmental conditions to the correct factory tool model.
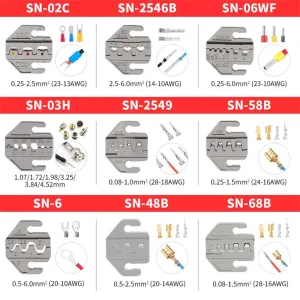
High-density PLC interfaces and terminal blocks demand DIN 46228 square and hexagonal ferrule crimping (e.g., SO-10WF Pro, SN-06WF). Even circumferential pressure ensures fine strands enter spring-clamp connectors smoothly without bending.
Harsh saltwater environments degrade crimp joints rapidly. Indent crimping on heavy tin-plated copper lugs (SO-10 Pro) cold-welds strand boundaries, halting moisture ingress along the copper core.
Wire harnesses use open-barrel connectors with separate conductor and insulation grips. Tools like the SO-04BPro and SO-06B deliver a "B-crimp" that curls the barrel tabs downward into the wire strands for vibration resistance.
Central office battery backup systems utilize double-hole copper lugs requiring calibrated indent or closed-barrel hex crimping. This maintains millivolt drop limits under continuous 48V DC float charge operations.
SIBO products meet strict testing standards so OEM distributors can sell directly into European, North American, and Asian-Pacific markets.
The core standard governing solderless crimped connections. Dictates rigorous test procedures for tensile pull-out strength, micro-sectioning strand deformation, and electrical contact resistance under environmental exposure.
Mandatory for equipment destined for the North American market. Involves static heating tests, continuous current-cycling verification at rated ampacity, and minimum mechanical pullout force thresholds for copper wiring.
All plasticized handle grips (PVC, TPR, PP) and metal surface platings comply with EU 2015/863 (RoHS 3) and Regulation (EC) No 1907/2006 (REACH). Guaranteed free of lead, cadmium, phthalates, and hexavalent chromium.
Explore our specialized catalog series, ready for private-label branding, customized jaw sets, and wholesale carton shipments.
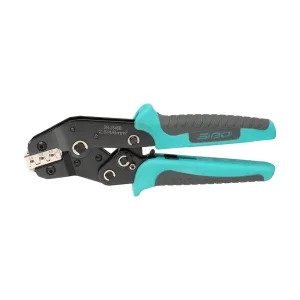
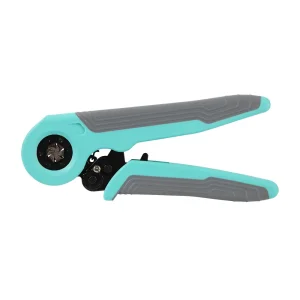
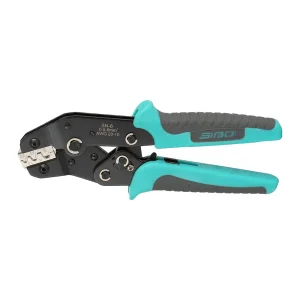
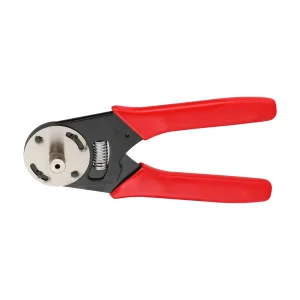
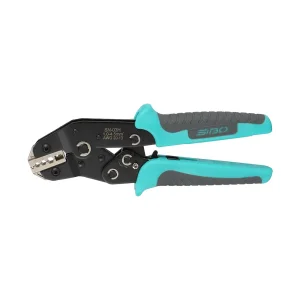
In-depth engineering answers addressing tool calibration, die profiles, factory audits, and OEM customization.
Our die sets are manufactured using slow-feed Wire EDM cutting with profile tolerances held strictly within ±0.015mm (±0.0006 inches). Each cavity undergoes optical comparator inspection and digital micro-caliper verification against terminal CAD cross-sections before release to assembly lines.
The internal ratchet gear remains engaged until the tool handles close past the critical bottom dead center point, ensuring full jaw closure. This prevents under-crimping caused by operator fatigue or rushed cycles. If foreign debris blocks closure, an emergency release lever clears the jaws safely without ruining the tool frame.
DIN 46235 specifies thick-walled electrolytic copper tubes requiring deep hexagonal or indent compression dies capable of high forces. DIN 46234 lugs are formed from stamped copper sheets with brazed seams, requiring gentler indent or roll-forming dies to avoid seam rupture. SIBO produces separate die families for both standards.
Yes. We have high-tonnage double-injection molding machines for custom two-color handles using TPR and polypropylene. We can incorporate molded logo reliefs into handle steel tooling, or pad-print and laser-etch branding based on client volume requirements.
Self-adjusting tools (such as the SO 10-6 series) use an internal floating multi-segment cam mechanism. As the handle closes, the six carbon-steel jaw segments compress radially inward toward the centerline. When the ferrule reaches target compaction density, increasing resistance triggers the ratchet trip point, delivering uniform hexagon crimps from 0.08mm² to 10mm² with zero manual die adjustments.
We provide Batch Inspection Certificates, Steel Raw Material Mill Test Reports, Rockwell Hardness (HRC) verification records, tensile pull-out test reports in kilonewtons (kN), and ASTM B117 neutral salt spray corrosion reports for export surface platings.
Standard catalog orders with custom laser markings ship in 15 to 25 business days. Full OEM orders involving custom dual-color handle moldings and private blister packaging take 30 to 45 days. ODM projects requiring bespoke die tooling take 14 days for initial sample prototyping followed by 30 days for mass production.
Standard ratchet crimpers feature ergonomic TPR grip handles intended for de-energized wiring operations only. For live-line service applications, SIBO offers dedicated 1000V VDE-certified tools manufactured to IEC 60900 specifications, featuring dual-layer injection insulation spark-tested at 10,000V AC.
