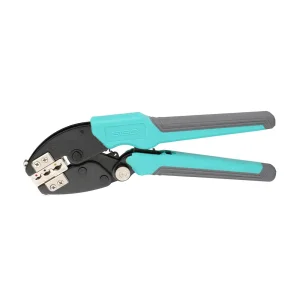
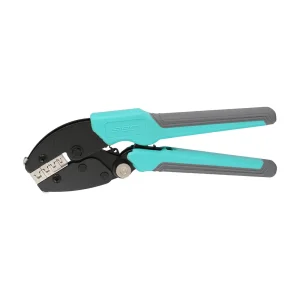
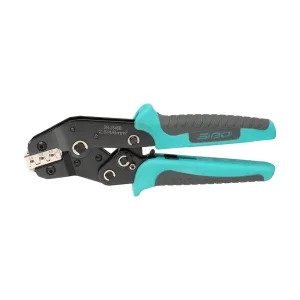
Factory-direct wire crimping pliers calibrated for photovoltaic, automotive, electrical switchgear, and terminal ferrule installations.
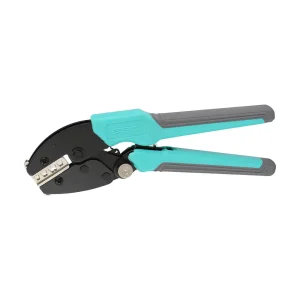


How the rapid shift toward clean electrification, industrial IoT automation, and high-voltage e-mobility is redefining crimp-quality tolerances globally.
The global transition to 1500V utility-scale DC solar arrays requires irreversible, gas-tight terminations. Faulty field crimps remain the #1 cause of catastrophic DC arc faults and thermal fires in photovoltaic systems. Precision-engineered tools like the SO-2546C Pro ensure exact compression height, maintaining low contact resistance across 25+ years of environmental exposure.
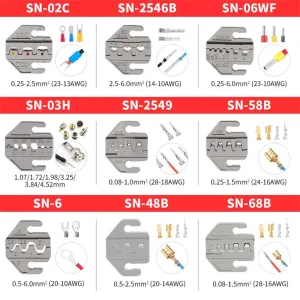
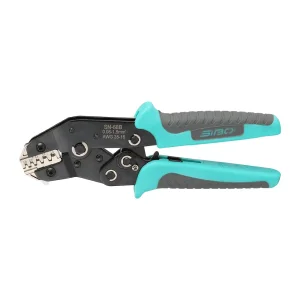
Electric vehicle (EV) battery management systems (BMS) and dynamic sensor arrays demand micro-tolerance crimps. Open-barrel connectors crimped with SN-68B and SN-2549 series tools provide controlled double-curl B-crimps that resist extreme mechanical vibration, high current density spikes, and broad thermal fluctuations without strand fracturing.
With high-density DIN-rail automation, control cabinets require high-density wiring terminated with end ferrules. Self-adjusting square and hexagonal crimping systems (such as the Mini 16-6 and SO 16-4) produce uniform cross-sectional compaction, ensuring low-resistance insertion into spring-clamp terminal blocks.
A comprehensive examination of plastic metal deformation, gas-tight micro-welding, and international compliance (IEC 60352-2 / UL 486A-B).
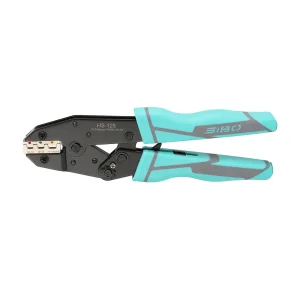
Under industrial standards such as DIN EN 60352-2, a dependable solderless crimp is not simply mechanical pressure; it is a controlled cold-flow process. When the jaws of the SIBO Pro Ratchet Crimper reach bottom dead center, the copper wire strands and terminal barrel undergo deliberate plastic deformation. This action fractures the surface oxide layer (CuO/Al2O3), triggering inter-metallic diffusion and cold micro-welding across contact faces. The resulting assembly forms an oxygen-free, gas-tight joint immune to oxidative corrosion, environmental moisture ingress, and thermal vibration loosening.
Improperly calibrated hand tools cause two persistent catastrophic field failures: Under-crimping (excessive air pockets, leading to high millivolt drops, thermal runaway, and electrical fires) or Over-crimping (severe strand nicking and localized barrel wall thinning, drastically reducing tensile pull-out strength below UL 486 thresholds). SIBO manufactures every die set from high-grade 42CrMo structural alloy steel, vacuum oil-quenched to HRC 58-62, guaranteeing that the calculated crimp height (CH) and crimp width (CW) remain stable after tens of thousands of cycles.
| Crimp Family / Terminal Type | Applicable SIBO Tool Series | Target Wire Cross Section | Terminal Standard Benchmark | Mechanical & Tensile Validation |
|---|---|---|---|---|
| Pre-Insulated Terminals (Ring, Spade, Pin, Butt) |
SO-30J Pro, SO-125 Series | 0.5 – 6.0 mm² (AWG 20 – 10) |
DIN 46237 / IEC 60760 | Dual-zone crimping: conductor strand compaction + insulation strain relief sleeve without sleeve rupture. |
| Wire-End Ferrules (Single & Twin Bootlace) |
SO-10WF, Mini 16-6, SO 16-4 | 0.08 – 16.0 mm² (AWG 28 – 5) |
DIN 46228 Part 1 & Part 4 | Self-adjusting hexagonal or 4-mandrel square compaction for optimized contact area in push-in cage clamps. |
| Photovoltaic PV Contacts (MC4 / Solar Connectors) |
SO-2546B Pro, SO-2546C Pro | 2.5 / 4.0 / 6.0 mm² (AWG 14 / 12 / 10) |
IEC 62852 / UL 6703 | Calibrated locator pin, high-leverage ratchet mechanism guaranteeing contact resistance <0.25 mΩ. |
| Open-Barrel Non-Insulated (Automotive & Harness Terminals) |
SN-68B, SN-2549, SO-04B Pro | 0.08 – 2.5 mm² (AWG 28 – 13) |
USCAR-21 / IEC 60352-2 | Precision-ground EDM B-crimp roll profile ensuring core strand capture and independent insulation grip. |
| Heavy Cable Stripping & Cutting (Cu/Al Multi-Strand Core) |
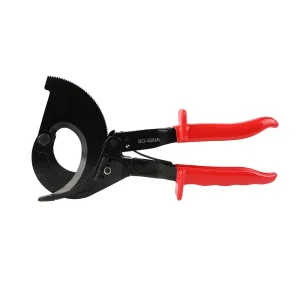
FST-325A, FST-520, FST-520A | Up to 400 mm² / 500 mm² (max. Ø 52mm) |
IEC 60228 Class 2 & 5 | Curved ratchet shear blade preventing cable ovalization and core deformation prior to lug crimping. |
Deploying specialized crimping architectures to eliminate electrical field failures across high-vibration, corrosive, and cleanroom operating environments.
Challenge: Solar parks encounter massive daily thermal cycling (-40°C to +85°C), high UV flux, and wind vibration. Inconsistent hand crimps on solar connectors cause resistive hot spots, arcing, and inverter shutdowns.
The SIBO Solution: The SO-2546 Pro series incorporates an ergonomic compound leverage linkage reducing manual exertion by 35%, coupled with an emergency ratchet quick-release. When tested under UL 6703 thermal cycling, contacts crimped with SIBO dies showed no measurable contact resistance degradation over 2,000 thermal shock cycles.
Challenge: Sub-millimeter micro-terminals used in CAN-bus wiring and engine ECU interfaces are vulnerable to ear twisting, asymmetry, and micro-cracking of terminal tin plating.
The SIBO Solution: Custom SN-series slot-jaw pliers utilize high-precision CNC Wire-cut EDM tooling dies with an integrated terminal positioner. The synchronized B-crimp form bends the open-barrel brass wings into smooth internal arcs without cutting individual copper filaments, preserving dynamic flexural endurance.
Challenge: High electromagnetic interference and saline/humid marine environments accelerate terminal corrosion when uninsulated copper strands are exposed inside PLC cabinets.
The SIBO Solution: Deploying the SO-10WF Pro and self-adjusting hexagonal crimpers seals multi-stranded flexible cables into bootlace ferrules. The hexagonal crimp provides a 360-degree uniform compressive boundary that seats securely into narrow spring-cage terminal blocks with zero stray wire overhang.
From custom terminal die cavities to private-label ergonomic dual-component handles and custom tool kit cases in Yueqing, Zhejiang, China.
Send your terminal drawing, stamped brass samples, or wire gauge spec. Our tooling engineers model custom die nests within 48 hours for validation.
Jaws are fabricated from premium forged tool steel or cold-drawn alloy stock, vacuum heat-treated to ensure exceptional tensile rigidity under peak load.
Multi-component PP+TPR soft handles custom-molded in your corporate Pantone colors with pad-printed or embossed brand logos.
Combine multi-die quick-change pliers, cable cutters (FST-520), and terminal assortments inside durable, heavy-duty embroidered textile kits.
Anticipating the technological shift in manual and electro-hydraulic crimp verification, ergonomic lightweighting, and surface durability.
Compound eccentric-lever ratchet linkages achieving 30-40% manual force reduction. Integrated emergency trip-release switches for blocked or foreign object safety.
Applying vacuum PVD TiN and DLC nanocoatings to die nests, reducing friction coefficient, preventing terminal tin sticking, and increasing die life past 100,000 cycles.
Embedding tactile micro-indicators and calibrated optical confirmation marks to ensure visual compliance with zero under-crimp risk for military and aerospace harnesses.
Authoritative technical guidance compiled by Yueqing Sibo Tools' senior engineering and quality control departments.
Ratchet crimping pliers (e.g., SO-30J Pro, SO-125) utilize dedicated, precision-machined cavities for specific cross-sectional wire gauges (e.g., 0.5-1.5, 1.5-2.5, 4.0-6.0 mm²). They lock until the required crimp height is completed. Self-adjusting crimpers (e.g., 16-6 Hexagonal, SO 16-4) automatically adapt their 4- or 6-mandrel jaws to match the wire diameter, making them ideal for varying end-ferrule tasks without swapping dies.
Our SO-2546C Pro solar crimping pliers employ a calibrated full-cycle ratchet wheel that prevents handle opening until the internal dead-center point is bypassed. If an obstruction occurs, an internal manual emergency release lever can be triggered. Every batch is calibrated using a pull-force tester to surpass IEC 62852 standards (min. 310N pull-out force for 4.0 mm² and 360N for 6.0 mm² solar cable).
We forge our precision crimp dies from 42CrMo or high-carbon 40Cr alloy tool steel. The parts undergo vacuum atmospheric quenching followed by precision tempering to achieve HRC 58-62 surface hardness. This prevents profile rounding, burring, or wall bowing under high-tonnage crimping cycles, ensuring dimensional repeatability across high-volume production.
Yes. By leveraging in-house Wire-cut EDM (Electrical Discharge Machining) and multi-axis CNC grinding centers in Yueqing, we create custom crimp cavities from customer-supplied CAD files (.STEP/.DXF) or stamped terminal samples. We perform test stampings, calculate cross-section compression ratios, and supply verified micrographic section cut reports before volume production.
For standard models with customized handle colors and laser-etched branding, our typical MOQ starts at 500 units. For completely custom tooling dies or bespoke Oxford bag combination kits, initial pilot runs of 300 to 500 sets are supported. Tooling prototypes are completed in 15–20 days, with container production fulfilling in 30–45 days.
Standard utility snips crush and flatten multi-strand copper cables into an oval geometry, complicating lug insertion and causing strand breakage. The FST-520 and FST-520A use dual curved, high-leverage ratchet scissor blades that encircle and shear conductor strands inward, preserving a rounded, unfrayed cable end ready for immediate terminal entry.
Review our extended factory portfolio of non-insulated terminal crimpers, mini European pliers, and heavy-duty mechanical ratchets.