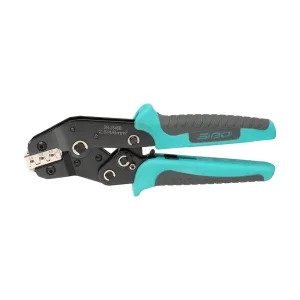
Engineered for zero-defect electrical terminations across open barrel terminals, pre-insulated connectors, wire ferrules, and MC4 solar contacts. Every unit undergoes automated mechanical torque testing.
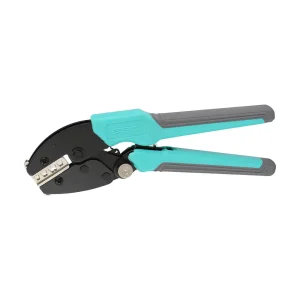

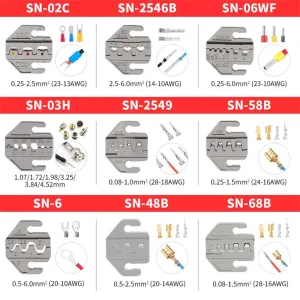
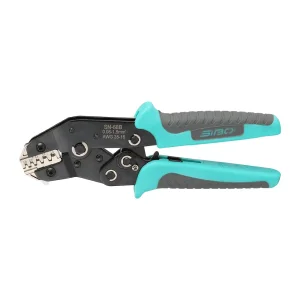
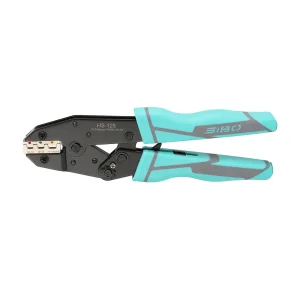

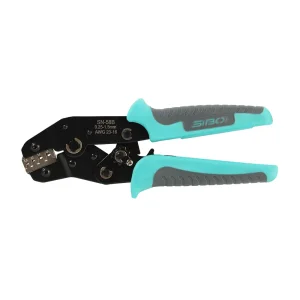
A crimp connection is not merely a mechanical squeeze—it is a controlled metal plastic deformation that creates a gas-tight, solderless atomic bond between stranded conductors and the terminal sleeve.
Under optimal crimp force, oxide layers on copper conductor strands and terminal barrels shatter. The metal flows into an inter-locking matrix with less than 5% micro-void spaces, preventing atmospheric oxygen, moisture, and hydrogen sulfide from penetrating and causing galvanic oxidation over 25+ years of operational service.
The single most critical quality indicator in automated and manual crimping is crimp height tolerance. Yueqing Sibo maintains jaw cavity tolerances within ±0.02 mm using ultra-slow wire EDM cutting. An over-crimped wire experiences tensile shearing, while an under-crimped joint suffers elevated electrical resistance.
Operator fatigue is the primary cause of intermittent electrical failures in manual harness assembly. SIBO's integrated ratcheting mechanism will strictly not disengage until the mechanical toggle reaches dead center, ensuring that every technician produces an identical metallurgical compression curve.
While soldered joints create an abrupt metallurgical boundary prone to brittle failure when subjected to cyclic harmonic vibration (such as automotive engine compartments or wind turbine nacelles), a cold-pressure ratcheted crimp redistributes mechanical stress along the terminal’s relief bell-mouth. SIBO tool crimpers achieve mechanical retention forces exceeding IEC 60352-2 baseline requirements by an average of 22% across copper and tinned conductors.
Located in Yueqing, Zhejiang—the renowned capital of low-voltage electrical apparatus in China—Yueqing Sibo Tools leverages an unrivaled cluster advantage that slashes prototyping lead times from months to days.
Certified AISI 4140 chrome-molybdenum alloy steel, high-carbon tool steel (SK-5), and high-strength forged structural carbon plates are sourced within a 15 km perimeter, providing steady metallurgical consistency and zero border-tariff friction on input metals.
Vacuum carburizing and continuous oil-quenching heat treatment facilities operating under strict German DIN 50150 norms deliver guaranteed working jaw hardness of HRC 42 - 48 while maintaining core toughness to eliminate jaw shear failure.
In-house CAD/CAM toolrooms equipped with Sodick wire EDM cutting machines allow our tooling specialists to deliver custom die prototypes in as fast as 72 hours for bespoke connector configurations submitted by clients.
Direct high-speed expressway access to Ningbo Port (2.5 hrs) and Shanghai Port (4 hrs) means regular containerized shipments, consolidated LCLs, and air-express sample shipments leave our warehouse loading docks without transit bottlenecks.
Procurement teams require more than commodity items; they demand private-label custom ergonomics, brand-specific color injection, custom Oxford kits, and rigorous regulatory compliance documentation.
Dual-component thermoplastic elastomer (TPR) and polypropylene (PP) grips engineered to client Pantone specifications. Ergonomically shaped to distribute hand palmar pressure evenly across 4 fingers, dramatically lowering repetitive strain injury (RSI) risks during high-frequency assembly line shifts.
High-contrast fiber laser etching of brand logos, model identification, wire cross-sections (mm² and AWG equivalents), and production batch QR codes directly on hardened carbon tool frames. Provides full traceability for aerospace, railway, and automotive audits.
Heavy-duty 1680D Oxford fabric carrying bags, custom EVA foam cutouts, and blow-molded hard cases containing interchangeable quick-change dies, wire strippers, and ratcheted cable cutters (FST-325A / FST-520), ready for distributor retail shelves or Amazon FBA warehousing.
| Wire Size (mm²) | AWG Equivalent | IEC 60352-2 Minimum Pull-Out Force (N) | SIBO Tested Force Guarantee (N) | Compatible SIBO Hand Crimper Models |
|---|---|---|---|---|
| 0.50 mm² | AWG 20 | ≥ 50 N | 68 N (Pass) | SN-2549, SN-58B, SO-125, SO-30J |
| 0.75 mm² | AWG 18 | ≥ 85 N | 110 N (Pass) | SN-2549, SO-125, SO-10WF Pro |
| 1.50 mm² | AWG 16 | ≥ 150 N | 195 N (Pass) | SO-30J Pro, SO-125 Pro, SO-10 Pro |
| 2.50 mm² | AWG 14 | ≥ 230 N | 285 N (Pass) | SO-2546B Pro, SO-2546C Pro, SO-10 Pro |
| 4.00 mm² | AWG 12 | ≥ 310 N | 390 N (Pass) | SO-2546C Pro, SO-16-4, SO-10WF Pro |
| 6.00 mm² | AWG 10 | ≥ 360 N | 460 N (Pass) | SO-2546C Pro, SO-16-4, SN-2546B |
| 10.00 mm² | AWG 8 | ≥ 500 N | 620 N (Pass) | SO-16-4 Ultra-Compact, SO-10WF Pro |
Global market entry requires stringent legal adherence. SIBO crimpers undergo full third-party substance screening and metallurgical evaluation to comply with European, North American, and Asia-Pacific industrial mandates.
All hand tools, including handles, electroplated frames, and return springs, are certified compliant with RoHS (2011/65/EU and 2015/863/EU) and REACH (EC No 1907/2006). Free from lead, mercury, hexavalent chromium, polybrominated biphenyls, and phthalate plasticizers.
SIBO crimpers are engineered to pass Underwriters Laboratories (UL) 486A-486B wire connector pullout tests. We maintain computerized digital tensile testing benches in our Yueqing quality lab, delivering pull-out graphs and standard deviation certificates with each export batch.
Electroless nickel plating and black oxide surface passivation withstand over 72 to 96 hours of neutral salt spray (NSS) testing without white corrosion or pitting, ensuring tools survive coastal offshore solar farms, marine shipyards, and damp basement switchgear rooms.
As renewable energy installations surge and automotive wiring harnesses embrace lightweight aluminum conductors and micro-signal sensors, hand crimping tools are evolving from simple mechanical levers into high-precision instruments.
With solar utility projects migrating to 1500V DC architectures, contact resistance at MC4-type junctions must stay below 0.25 mΩ. SIBO's SO-2546 series provides calibrated B-crimp and locator brackets designed specifically for thick-walled PV1-F and H1Z2Z2-K cross-linked solar cables.
Automotive ADAS sensors and CAN-bus networks require terminal crimping down to 0.03 mm² (AWG 32). Our SN-58B and SN-68B open barrel tools utilize EDM-ground micro-step teeth that form micro-spring tabs without terminal neck distortion.
Contractors no longer carry 5 separate pairs of crimpers. Patented push-button and magnetic slide-lock quick-release die systems allow technicians to swap from insulated terminals to solar connectors or wire ferrules in under 5 seconds without screwdrivers.
Next-generation prototype crimpers integrate micro-electromechanical sensors and Bluetooth cycle loggers, verifying full-closure strokes and notifying QA supervisors when calibration recalibration intervals are due after 10,000 cycles.
From extreme weather desert solar arrays to vibration-heavy high-speed rail locomotive control cabinets, our tools guarantee uninterrupted current transmission.
In 500 MW solar parks across the Middle East and Southwestern United States, thousands of MC4 connectors are crimped daily under direct sunlight exceeding 45°C. SIBO SO-2546B Pro and SO-2546C Pro provide forged frame stability that prevents jaw spreading under heavy continuous load, maintaining sub-milliohm joint conductivity.
Dense terminal block wiring requires perfectly squared ferrule cross-sections. SIBO's SO-16-4 self-adjusting quadrangular and hex crimpers automatically compress multi-stranded copper conductors from 0.08 to 16 mm² into compact, burr-free ferrules that slide effortlessly into spring-clamp DIN-rail terminals.
Commercial vehicle fleet maintenance demands exact B-crimps on open-barrel spring terminals. The SN-2549 and SN-68B pliers roll the terminal ears cleanly over the conductor core and insulation jacket simultaneously, satisfying SAE/USCAR-21 vibration resilience standards.
Direct engineering answers to the most common questions raised by electrical distributors, brand product managers, and supply chain directors.
Ratchet crimping pliers (e.g., SO-30J, SO-125, SN-2549) use rigid, fixed-dimension EDM die cavities dedicated to specific terminal gauges and profiles (such as pre-insulated rings, spade terminals, or open-barrel connectors). The full-cycle ratchet ensures complete stroke compression before opening. In contrast, self-adjusting crimping pliers (such as the SO 16-4) incorporate a rotating cam mechanism with 4 or 6 synchronized jaws that dynamically adapt their closing circumference to the wire cross-section (from 0.08 to 16 mm²). Ratchet tools are ideal for high-volume repeatable production with fixed terminal specs, while self-adjusting tools excel in maintenance and control panel building where mixed wire sizes are terminated sequentially.
The SIBO SO-2546 Pro Series (including SO-2546B Pro and SO-2546C Pro) is expressly designed for 2.5 mm², 4.0 mm², and 6.0 mm² (AWG 14 / 12 / 10) photovoltaic cable contacts. Featuring precision-milled stepped die cavities with an integrated contact locator, it ensures that open-barrel or solid solar contact pins sit at the exact focal axis during crimping. This creates the optimal B-crimp geometry that guarantees minimal electrical resistance (< 0.25 mΩ) to prevent hot-spot formation in utility PV arrays.
Yes. We regularly develop custom OEM/ODM dies for automotive tier-1 suppliers, telecom OEMs, and industrial automation clients. By providing your terminal 2D/3D engineering drawings (STEP/IGES/DXF) or sample pins along with wire cross-sections, our CAD engineering team designs custom die cavity geometry using slow-wire EDM cutting. Prototype samples are typically completed within 5 to 7 working days, accompanied by cross-section micro-photographs and tensile pull test reports.
For standard factory tool models with custom laser-etched brand logos, our MOQ starts at 200 to 500 units. For custom dual-color TPR handle mold injection to match brand Pantone shades and bespoke blister card or color box packaging, MOQ is generally 1,000 to 2,000 units. Standard batch lead time ranges from 20 to 35 calendar days following final sample sign-off and packaging art confirmation.
Every SIBO ratchet crimper incorporates an eccentric star-wheel adjustment disc locked by a grub screw. This allows recalibration as internal pivot pins bed in over tens of thousands of cycles. In our factory QA facility, every production lot is spot-checked using digital force load cells and calibrated tensile test benches to verify that pull-out forces meet or exceed IEC 60352-2 and UL 486A-B standards before packaging.
Browse our additional heavy-duty ratchet pliers, mini European style wire-end ferrule crimpers, and non-insulated terminal solutions ready for containerized wholesale export.


Speak directly with our senior tooling engineers in Yueqing. We review terminal drawings, recommend optimum compression ratios, and provide sample die prototypes with full mechanical pull test verification before tool steel hardening.