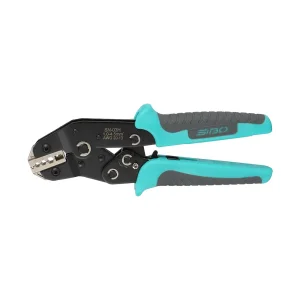
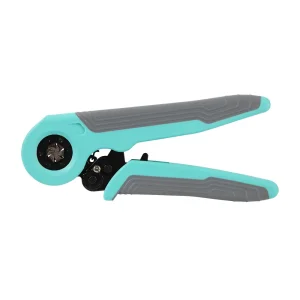
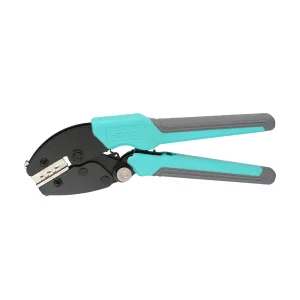
Direct factory-manufactured termination tooling optimized for non-stop field work. Every tool integrates cold-formed alloy jaws, hardened shear edges, and ergonomic force multipliers to minimize cycle times across high-volume installation projects.
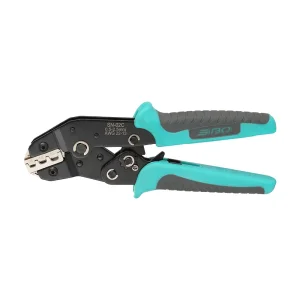

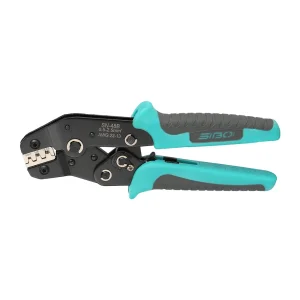
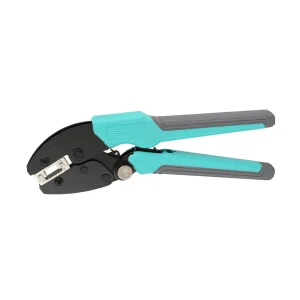
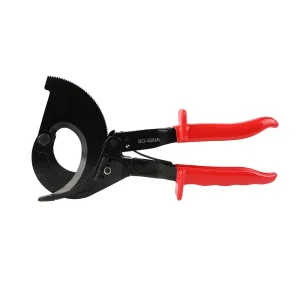
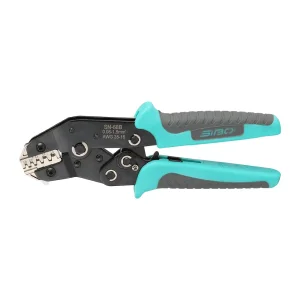
Modern electrical engineering and assembly automation demand extreme repeatability and streamlined operator workflows. The traditional paradigm of switching between stand-alone cable shears and dedicated terminal crimpers introduces tool-switching latency, increases technician carrying weight, and elevates the rate of incomplete joint compressions. SIBO Tools solves this challenge by engineering combined 2-in-1 crimp-and-cut mechanisms that execute clean, non-deforming copper/aluminum shearing alongside calibrated, gas-tight terminal crimping within a singular, balanced tool chassis.
In high-density industrial control cabinet production, assembly personnel execute thousands of terminations per shift. Research demonstrates that swapping between an independent cutter and a crimping plier expends an average of 3.8 seconds per termination cycle. SIBO's integrated 2-in-1 design combines an induction-hardened bypass shear blade behind the primary die cavity, dropping transition time to zero while maintaining absolute mechanical integrity.
A compromised, crushed, or splayed conductor end guarantees poor terminal entry, causing splayed strands and catastrophic hot spots. Our 2-in-1 shear elements utilize curved, razor-honed SK5 alloy blades that encircle multi-strand conductors, maintaining exact cylindrical geometry. The prepared conductor immediately feeds into the terminal barrel without fraying, enabling precision crimping in one continuous motion.
Manual pliers without ratchets allow operator discretion, leading to incomplete crimps when muscles tire. SIBO's integrated full-cycle ratchet interlock holds the jaw jaws captive until maximum engineered compression is attained. A built-in safety release mechanism allows immediate clearance in case of foreign body jams, ensuring both worker protection and terminal standardization across multi-shift factories.
The international electrical contracting and manufacturing landscape is undergoing rapid modernization driven by clean energy installation, transportation electrification, and factory automation. As global hardware brands and regional suppliers seek to capture market share, the demand for dual-action hand tools has shifted from novelty utility items to certified industrial-grade equipment capable of meeting exacting international testing protocols.
| Geographic Territory | Primary Industrial Drivers | Dominant Connection Types | Core Compliance Standards | Key Procurement Priorities |
|---|---|---|---|---|
| European Union & UK | Renewable EPCs, Building Automation, Machine Tool Wiring | DIN 46228 Wire-End Ferrules, Twin Ferrules, MC4 | DIN EN 60352-2, CE, RoHS 3, REACH | Ergonomics, VDE certification synergy, calibrated pull-out force |
| North America | Commercial Switchgear, Solar Utility, EV Fleet Maintenance | Insulated Ring/Spade, Open Barrel B-Crimp, Splices | UL 486A-486B, CSA C22.2 No. 65, OSHA Ergonomics | High leverage, long tool lifespan, high drop impact resistance |
| Asia-Pacific (APAC) | Automotive Wire Harness, Consumer Electronics Assembly | Non-Insulated Open Barrel, Miniature Crimp Pins | JIS C 2805, GB/T 14048, ISO 9001:2015 | High precision die geometry, volume scalability, OEM private labeling |
| Middle East & Africa | Large-scale Utility PV, Infrastructure, Substation Cabling | Heavy-Duty Lugs, Photovoltaic Connectors | IEC 60947-1, IEC 61238-1 | Corrosion resistance, heat-treated durability, multi-gauge die coverage |
The true measure of a high-quality 2-in-1 crimp-and-cut tool resides in its metallurgical execution. In cutting, high surface hardness is required to maintain sharp shear edges against multi-strand copper work-hardening. In crimping, fracture toughness and dimensional stability under repetitive cyclic stresses are vital to avoid die-pocket distortion.
Our tool chassis is cold-stamped and CNC-milled from premium S50C structural carbon steel and 40Cr alloy steel. Through controlled atmospheric heat treatment, the frame achieves a core tensile strength capable of withstanding mechanical spreading forces exceeding 15 kN without structural deflection, preserving die-cavity parallelism over tens of thousands of cycles.
The integrated shearing elements utilize Japanese SK5 high-carbon tool steel, hardened via vacuum quenching to HRC 58-62. Precision diamond-wheel ground cutting profiles feature an optimized bypass scissor geometry that cleanly shears soft copper and aluminum wire up to 16 mm² without pinching, flattening, or disturbing individual conductor strands.
Mechanical wear over thousands of operational cycles can impact crimp compression height. SIBO integrates an eccentric gear regulation disc on the primary pivot assembly. Technicians can adjust the mechanical compression stroke in 6 distinct micro-increments, compensating for die wear and ensuring ongoing compliance with UL pull-out force criteria.
From extreme outdoor climate environments to high-speed electronics bench assembly, dual-action crimping and cutting tools are deployed across mission-critical sectors where electrical fault downtime carries immense financial cost.
Utility-scale solar fields require installers to terminate thousands of MC4 connectors under harsh outdoor conditions. Having a 2-in-1 tool enables technicians working on rooftop racks or ground mounts to trim double-insulated 4mm² or 6mm² PV cables cleanly and crimp precision solar contacts with a single tool, eliminating tool drops and safeguarding electrical conductivity.
Modern vehicle wiring utilizes high-density open-barrel non-insulated pins (such as AMP/Molex contacts). Our SN-series dies produce an authentic "F" or "B" roll crimp that mechanically clinches the wire insulation tab while forming a gas-tight bond on the conductor core. The integrated shear allows rapid trim adjustment in confined engine bays and instrument clusters.
Industrial panel shops demand strict wire ferrule compliance under UL 508A and IEC 60204-1. SIBO self-adjusting ferrule crimpers with integrated cutters allow panel builders to quickly cut flexible control wires to length, insert ferrules, and produce uniform square or hexagonal profile crimps that slide effortlessly into terminal blocks with zero strand damage.
Operating from our modern manufacturing base in Yueqing, Zhejiang—the epicenter of China's low-voltage electrical tooling industry—SIBO Tools functions as a premier contract manufacturer and private-label partner for world-leading brands. We offer end-to-end customization services supported by thorough in-house metallurgical and dimensional testing.
Have an engineered terminal design requiring non-standard crimp geometries? Our engineering team utilizes 3D CAD modeling, CNC wire-EDM cutting, and rapid prototyping to produce bespoke crimping die sets tailored to proprietary connector terminals in as few as 18 working days, accompanied by complete CMM dimensional inspection reports.
Strengthen your retail and distribution presence. SIBO offers multi-cavity injection molding for custom ergonomic dual-material handles (PP + TPR) in your brand’s custom Pantone colors. Precision fiber-laser marking delivers crisp, permanent corporate logos, model codes, and wire gauge designations directly on the blackened tool steel chassis.
Every manufacturing lot undergoes automated tensile pull-off testing on calibrated digital force gauges to guarantee mechanical performance that surpasses DIN EN 60352-2 standards. We perform continuous metallurgical micro-section cross-examinations, confirming zero conductor voiding and pure mechanical consolidation before packing and dispatch.
The mechanical hand tool sector is not static. SIBO Tools invests continuously in metallurgical science, biomechanics, and digital QA systems to build termination tools ready for Industry 4.0 data traceability.
Optimized handle curve vectors and thermoplastic elastomer (TPE) palm zones reducing grip activation strain by 24% while resisting aggressive industrial motor oils, hydraulic fluids, and sunlight UV radiation.
Integration of nanotech PVD carbon-matrix coatings on shear blades, multiplying cutting longevity by 400% when trimming difficult tinned copper strands and cross-linked polymeric jacketing.
Embedding passive NFC micro-transponders within handle moldings, enabling quality inspectors on factory floors to log lifetime crimp cycles via mobile tablet to maintain preventative maintenance schedules.
Miniature piezo-electric micro-sensors embedded in die housings that provide instant visual LED verification when terminal compression achieves gas-tight density specifications.
Clear, engineering-focused answers to common technical, metallurgical, and supply chain queries raised by procurement directors and quality assurance managers.
The shear blades are situated in an independent mechanical shear pocket positioned behind the primary crimp dies on the leverage fulcrum. The cutting movement functions through scissor bypass geometry that activates seamlessly through handle closure. The cutting teeth are ground from high-carbon SK5 steel hardened to HRC 60+, while the crimp dies are isolated from lateral shear strain, allowing each functional zone to operate without mechanical interference.
To achieve full verification, a crimped termination sample is potted in epoxy resin, sectioned perpendicular to the axis, and polished for optical microscopy. The conductor strands must show pure polygonal plastic deformation with zero air voids between individual strands or the terminal sleeve. Additionally, tensile extraction testing is performed on a motor-driven digital pull tester to verify that pull-out forces exceed the Newton thresholds mandated for each respective conductor gauge.
Yes. We manufacture magnetic quick-change and precision knurled thumb-screw die lock systems. This modularity enables a single 2-in-1 tool frame to switch between insulated terminal jaws, non-insulated open barrel dies, solar PV connector profiles, and wire ferrule assemblies in seconds, all while utilizing the same built-in high-leverage cable cutter.
For standard production catalog models featuring custom laser-marked corporate branding, our base MOQ starts at 500 units. For fully customized dual-color molded handles and custom retail packaging (such as blister cards or Oxford combination tool kits), the typical MOQ is 1,000 units. Standard production lead times run between 25 and 35 calendar days following pilot sample verification.
Discover our high-precision ratcheting crimpers, self-adjusting ferrule systems, and industrial cable cutters designed for extreme reliability across solar EPC, manufacturing plant maintenance, and electrical construction installations.