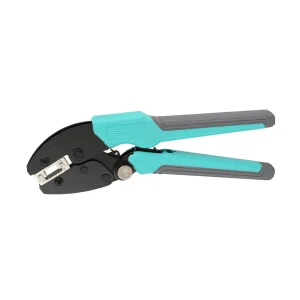
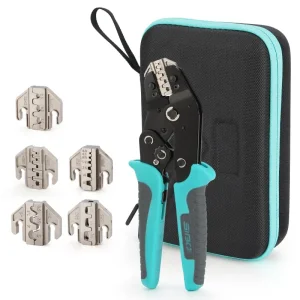
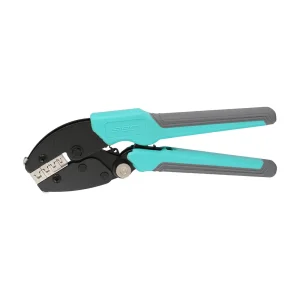
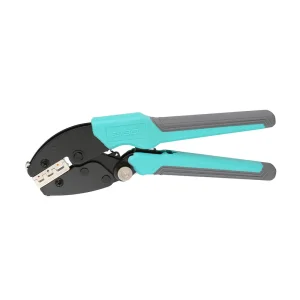
Explore precision-calibrated ratchet tools designed for non-insulated terminals, insulated terminations, open-barrel connectors, and heavy-duty industrial shearing.

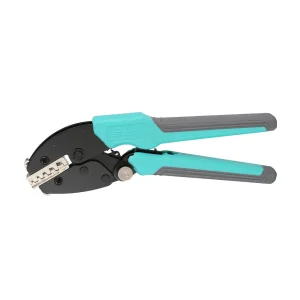
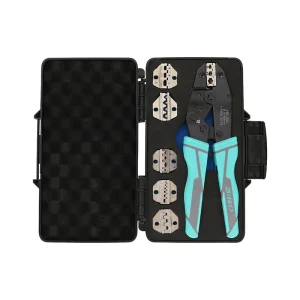
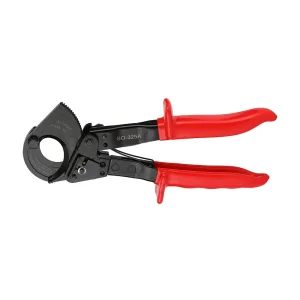
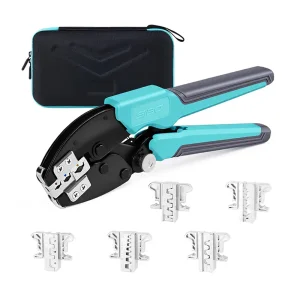
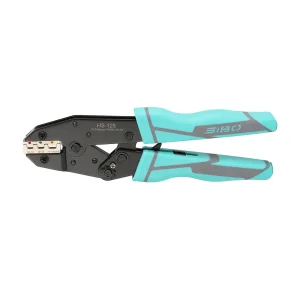
Analyzing macroeconomic electrification, transition bottlenecks, and why metallurgical repeatability defines procurement success across modern production environments.
The rapid expansion of electric mobility (EVs), grid-scale photovoltaic arrays, commercial energy storage systems (BESS), and edge-computing data centers has surged demand for mechanical connector crimping by over 240% globally. In electrical infrastructure, a single improperly crimped pin terminal creates thermal runaway risks capable of decommissioning entire multi-megawatt switchgears.
Manual pliers without ratcheting mechanisms yield inconsistent compaction densities, varying between 65% and 85% solid state wire fill depending on technician grip strength. SIBO's integrated precision ratchets lock the tool until predetermined mechanical closure forces (exceeding 1.8 kN) are met, eliminating cold welds, voids, and vibration-induced conductor pull-outs.
Global original equipment distributors are actively migrating away from multi-tier trading entities toward vertically integrated manufacturing hubs in Yueqing, China. Procuring directly from factory floors guarantees continuous metallurgical quality tracing, customizable die cavity EDM machining, and 30-45% lower total cost of ownership (TCO).
A comprehensive examination of how die tolerances, progressive carbon steel heat treatments, and controlled plastic deformation eliminate contact resistance.
In electrical engineering, crimping is fundamentally a controlled cold-welding process. When stranded copper wire is placed within an open-barrel or tubular ferrule, the crimping die applies concentrated multiaxial forces. This collapses the terminal sleeve, extruding individual strands together until interstitial air gaps collapse below 5% cross-sectional area.
SIBO's die geometries are engineered via Finite Element Analysis (FEA) to provide clean compressive flow without shearing outer strands. This mechanical cohesion creates a verified gas-tight joint, preventing airborne oxygen, sulfur dioxide, and corrosive humidity from entering the contact core, thereby preventing copper oxide insulating films from elevating electrical resistance over decades of deployment.
Every jaw family (including the SO-10 Pro and SO-125 Pro series) is calibrated to exceed international terminal retention standards, ensuring tensile rupture occurs in the copper conductor body rather than slipping out from the crimped barrel.
Our crimper frames undergo progressive stamping from reinforced high-carbon steel plates. Frame jaws undergo controlled vacuum oil quenching to achieve Rockwell hardness of HRC 42–46 for flexural resilience, while crimping dies reach HRC 58–62 for exceptional wear resistance.
Die profile deviations directly impair terminal crimp height. SIBO cuts all interchangeable jaw inserts using precision slow-walk Wire Electrical Discharge Machining (Wire-EDM) within tolerances of ±0.015mm and micro-finish Ra ≤ 0.4μm, eliminating burrs and plating scuffing.
Employing optimized multi-pivot compound linkage geometry, SIBO pliers multiply manual operator hand grip force by a mechanical ratio of up to 1:18. This reduces trigger hand effort during repetitive crimping cycles in industrial panel assembly.
| Crimp Architecture | Applicable Tool Series | Terminal Cross-Section Scope | Deformation Topology | Typical Industrial Deployment |
|---|---|---|---|---|
| Pre-Insulated Oval / Double Crimp | SO-30J Pro, SO-125 Pro | 0.5 – 6.0 mm² (20–10 AWG) | Simultaneous copper wire compaction & outer PVC/Nylon jacket strain relief | Switchgear cabinets, Building power distribution, Industrial automation |
| Open-Barrel "B-Type" Roll Crimp | SO-06B Pro, SO-04B Pro | 0.5 – 6.0 mm² (20–10 AWG) | Dual folding wings curled symmetrically into stranded copper center | Automotive wire harnesses, Appliance wiring, White-goods assembly |
| Hexagonal / Self-Adjusting Square | HSC8 16-6, SO 16-4 | 0.08 – 16.0 mm² (28–5 AWG) | Concentric 4 or 6-face uniform dynamic radial contraction | PLC terminal blocks, DIN-rail spring clamp interfaces, High-density cabinets |
| Heavy Indent Non-Insulated Lug | SO-10 Pro, SO-056FL-Pro | 1.5 – 10.0 mm² (16–8 AWG) | Deep central mechanical punch indentation into solid annealed copper lug | Battery bank cables, Power transformer feeds, Marine grounding bars |
| Solar Photovoltaic Specialized | SO-2546B Pro, SO-2546C Pro | 2.5 / 4.0 / 6.0 mm² (14–10 AWG) | Precision step-gauge MC4 open/machined contact pin compression | Solar PV farm installations, Inverter balance-of-system (BOS) strings |
From solar farms enduring extreme UV exposure to mission-critical aerospace testing benches, discover how our tools guarantee operational integrity.
Utility-scale 1500V DC photovoltaic strings operate in desert and maritime environments with ambient shifts from -30°C to +65°C. An improper MC4 solar connector crimp introduces high contact micro-resistance (>2 mΩ), precipitating hot-spot fires. Utilizing our SO-2546B/C Pro ratchet tool guarantees repeatable crimp depth across 2.5, 4.0, and 6.0 mm² solar cables, keeping joint resistance below 0.3 mΩ.
Modern commercial trucks and passenger vehicles feature high-speed CAN-bus networks and sensor architectures subjected to continuous harmonic vibration. Our SO-04B Pro and SO-06B Pro deliver crisp "B-crimps" on open-barrel spade and receptacle pins. The rolled wings lock conductor strands firmly without nicking the copper core, completely passing SAE/USCAR-21 automotive vibration standards.
Building high-density control panels requires terminating hundreds of thin control cables into tight push-in terminal blocks. The SO 16-4 and HSC8 16-6 mini self-adjusting ferrule crimpers apply balanced hexagonal or quadrilateral pressure across 0.08–16mm² ferrules. The result is smooth, snag-free insertion into DIN rail terminals without frayed strands or high contact heat.
Complete quality governance from Yueqing Sibo Tools: raw steel metallurgical certification, precision stamping, vacuum heat treatment, and automated calibration.
We source heavy-gauge structural carbon steel and Cr-Mo alloy stock with complete mill heat certificates. Raw plates undergo chemical spectrometry to verify optimal carbon, chromium, and molybdenum ratios prior to progressive punch-die blanking.
Stamped frames and EDM-cut jaws undergo computer-controlled vacuum furnace hardening and continuous dual-stage tempering cycles. This prevents microscopic surface stress fractures and maintains long-term structural dimensional stability.
Every individual tool assembly undergoes manual technician calibration of the eccentric gear pressure adjustment wheel. Random sample batches from every shift are subjected to digital load-cell pull-off tests to verify absolute DIN compliance before packaging.
Examining disruptive advancements in smart tool sensor integration, aerospace-grade alloy frames, and magnetic rapid-interchange systems.
Industrial 4.0 specifications are entering the hand-tool sector. SIBO's engineering department is actively prototyping embedded micro-piezoelectric sensors within ratchet housings. These systems log crimping cycle completions and peak pressure spikes via Bluetooth LE / NFC to mobile quality-assurance consoles.
This guarantees 100% auditable documentation for mission-critical installations such as passenger rail switchgear, subsea power links, and nuclear power plant instrumentation cabinets.
Technicians frequently waste up to 25% of their working hours searching for screwdrivers to swap out threaded jaw sets when moving between terminal types. Our patented Magnetic Quick Replacement Crimper Sets use precision guide dowels backed by high-coercivity Neodymium magnets.
Dies snap in securely within 3 seconds, self-aligning to within ±0.02mm tolerance. They withstand up to 15,000 continuous compression cycles without jaw shift or looseness.
Accelerating product line expansion for international hardware brands, tool wholesalers, and private-label electrical conglomerates.
Reinforce your brand identity with custom handle colors, ergonomic textures, and custom dual-shot injection molds. We offer high-definition fiber laser engraving andpad printing with your proprietary logos, serial numbering, and regional compliance symbols.
Package our ratchet pliers, interchangeable die sets (HS-30J, SO-125, SO-10WF), wire strippers, and cable cutters into ballistic Oxford cloth carrying cases, high-density blow-molded storage boxes, or clear clamshell blister packaging ready for store shelves.
If you have proprietary stamped connectors or specialized automotive connectors, send us your terminal samples. Our R&D team uses CAD/CAM modeling, 3D printing validation, and wire-EDM cutting to produce production-grade custom dies within 15–20 business days.
In-depth technical answers addressing quality assurance, jaw compatibility, wire pull-out ratings, and direct OEM procurement procedures.
Standard non-ratchet crimping pliers rely entirely on manual hand strength, resulting in uneven terminal compression and cold solder failures. Full-cycle ratchet crimping tools (such as the SIBO SO-10 Pro and SO-125 Pro) feature internal gear-driven pawls that do not release until complete mechanical closure is achieved. This ensures every crimp reaches the exact designed crimp height without operator dependency.
Self-adjusting crimpers like the HSC8 16-6 and SO 16-4 employ floating radial carbon steel cam segments. When the handles are squeezed, the segments slide symmetrically toward the center, automatically contracting until meeting the natural resistance of the copper conductor and ferrule sleeve. This eliminates manual die swapping across 0.08–16 mm² wires.
Overheating in photovoltaic arrays is primarily caused by loose crimping, which leads to contact resistance over 3 mΩ and burns out connector housings under continuous 30A DC loads. Our SO-2546B Pro and SO-2546C Pro are calibrated to produce an exact B-type roll crimp on MC4 contact pins, consistently keeping contact resistance under 0.3 mΩ and fully meeting IEC 62852 standards.
SIBO ratchet crimpers feature a star-wheel eccentric calibration disc on the frame's pivot axis. By loosening the locking screw and rotating the stepped eccentric dial toward the "+" position, technicians can fine-tune mechanical linkage pre-load to compensate for pin wear and maintain precision factory crimp heights even after 10,000+ operations.
For custom handle color molding, laser branding, and tailored packaging, standard MOQ starts at 500 to 1,000 units depending on the model. Standard production lead times run between 25 and 35 calendar days from sample sign-off, supported by real-time tracking from our Yueqing factory floor.
Our internal testing laboratory performs micrographic cross-section testing, tensile pull-off force testing using digital load cells, and micro-ohmmeter contact resistance evaluations according to UL 486A-B and DIN EN 60352-2 protocols. Batch inspection certificates and material declarations accompany every export shipment.
Complete your procurement line with self-adjusting hexagonal pliers, quick-change combination toolsets, and heavy ratchet cable cutters.