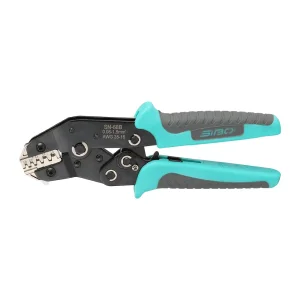
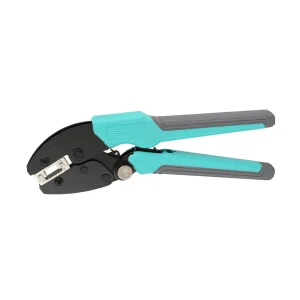
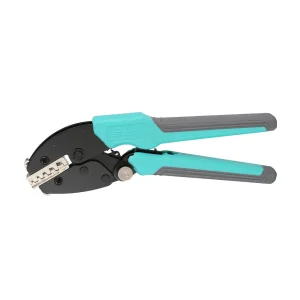
Explore our heavy-duty ratchet crimpers, calibrated for fork, spade, and open-barrel wire terminations with full-cycle ratchet integrity and mill-spec die accuracy.

Analyzing structural wire termination dynamics across automotive e-mobility, grid modernization, and high-frequency vibration environments.
Global transition towards distributed renewable energy and microgrid architectures requires millions of high-integrity terminations per megawatt. Fork terminals, widely preferred for their serviceability in barrier strip architectures, demand uniform mechanical compression to prevent micro-arcing and subsequent thermal runaways.
SIBO's full-cycle ratchet designs eliminate intermediate release states, ensuring cold-welded copper-to-terminal gas-tight interfaces compliant with international pull-out thresholds.
As electrical engineering contractor forces encounter aging demographics and shortage bottlenecks, operator repetitive strain injuries (RSI) have surfaced as a major project risk factor. Traditional high-leverage manual crimpers impose up to 450 N of hand force per stroke.
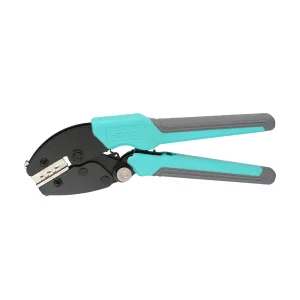
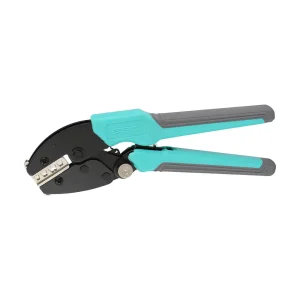
SIBO incorporates high-mechanical advantage toggle linkages, redistributing effort across multi-pivot kinematics and slashing peak operational force by over 38% without compromising jaw compression.
Modern PLC switchboards and distributed control units (DCUs) demand sub-millimeter clearances. Standard fork terminal crimpers often distort terminal insulation sleeves during lateral crimp cycles, leading to cross-terminal dielectric failure.
SIBO’s progressive CNC-milled dies isolate the conductor strand compaction barrel from the outer nylon/PVC strain relief sleeve, delivering symmetrical, non-flaring crimp geometries.
A granular look into our precision die tooling, alloy selection, and heat treatment methodology located in Yueqing, Zhejiang Province.
Tool jaws are drop-forged and investment cast using premium chromium-molybdenum alloy steel, retaining extreme mechanical fatigue thresholds under 20,000+ cycle fatigue loads.
Induction-hardened jaws achieve a surface hardness of 48-52 HRC, preventing cavity deformation when pressing thick cold-rolled copper fork connectors up to 16 mm² (6 AWG).
An integrated micro-adjusting star wheel enables precise calibration of jaw preload pressure over extended operating years, counteracting natural component mechanical wear.
In the event of accidental foreign object insertion or misaligned terminal positioning, our integrated quick-release pawl safely disengages the ratchet stroke instantaneously.
| Series Model | Terminal Suitability | Wire Cross-Section | Crimp Profile | Body Material | Compliance Standards |
|---|---|---|---|---|---|
| SO-30J / SO-30J Pro | Pre-Insulated Fork / Spade / Ring | 0.5 – 6.0 mm² (20-10 AWG) | Oval & Double Crimp | Carbon Steel Frame | DIN EN 60352-2 |
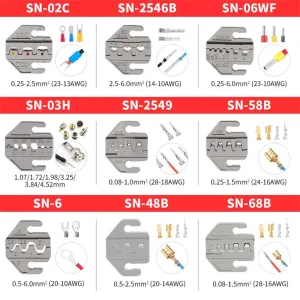
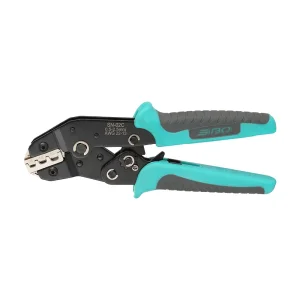
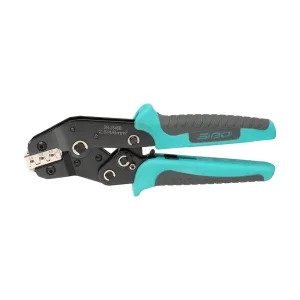
| SN-02C Mini European | Insulated Fork & Pin Terminals | 0.25 – 2.5 mm² (24-14 AWG) | Micro-Conductor Profile | AISI 4140 Die Alloy | UL 486A-486B |
| SO-10 Pro | Non-Insulated Lugs & Open Forks | 1.5 – 10.0 mm² (16-8 AWG) | Deep Point Indent | Drop-Forged 50CrV4 | RoHS / CE Compliant |
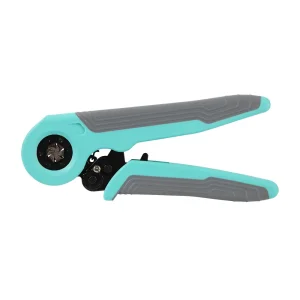
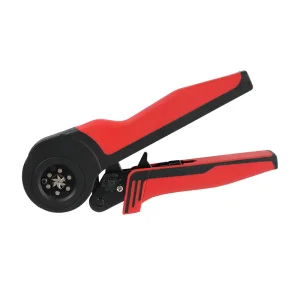
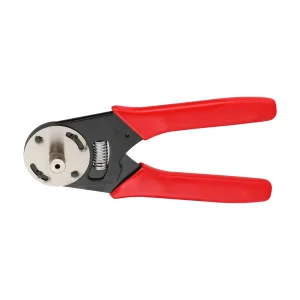
| SO-16-6 Hex Series | End Sleeves & Composite Forks | 0.08 – 16.0 mm² (28-5 AWG) | Hexagonal Uniform Wrap | High-Strength Manganese | MIL-SPEC Calibrated |
Engineered to satisfy demanding environmental constraints across North America, Europe, East Asia, and emerging industrial hubs.
Designed around standard NEMA terminal blocks and transformer interfaces. Certified SIBO dies yield gas-tight compressions on UL-rated copper fork lugs, withstanding continuous thermal fluctuations from -40°C to +105°C without dielectric insulation rupture.
Rolling stock and wayside signaling enclosures experience constant multi-axis harmonic vibration. Our crimpers enforce terminal barrel closure conforming to EN 50155 vibration and shock profiles, preventing wire creep and contact resistance degradation.
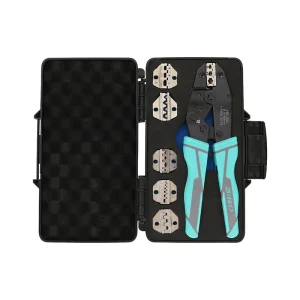
Automotive service depots handle a multitude of terminal formats. SIBO quick-swap modular jaw plier platforms enable mechanics to transition from insulated fork lugs to uninsulated open-barrel B-crimps in under five seconds without external tools.
How Yueqing Sibo Tools guarantees reproducible crimp geometries conforming to DIN, UL, and IEC verification protocols.
Every crimper configuration undergoes strict tensile pull tests according to UL 486A-486B and IEC 60999. Samples are pulled at calibrated rates to verify that the terminal junction fails via wire conductor rupture before physical pull-out occurs.
Our quality assurance laboratory conducts metallurgical potting, slicing, polishing, and chemical etching on sample crimps. Microscopic inspections verify zero strand void pockets, confirming ideal cold-weld compaction rates between 85% and 92%.
Plier frames receive black oxide surface passivation, electrophoretic deposition, and salt spray testing exceeding 72 hours per ASTM B117, assuring non-corrosive reliability in coastal, marine, and chemical plant environments.
SIBO’s strategic technological milestones in ergonomic lightweighting, digital crimp tracking, and IoT fleet management.
Targeted for mass-market launch, our R&D team is developing hybrid magnesium-carbon composite crimper bodies that reduce overall tool payload weight by 42% while retaining 100% frame rigidity under extreme 15 kN peak mechanical stress.
Next-generation precision crimpers will incorporate micro-piezoelectric pressure transducers within the toggle nexus, providing visual LED and acoustic feedback confirming whether each stroke fell inside specified crimp pressure tolerances.
Embedding non-volatile near-field communication tags directly within handle grips allows enterprise contractors to scan tool maintenance history, cumulative cycle counts, and recommended re-calibration schedules via any standard smartphone interface.
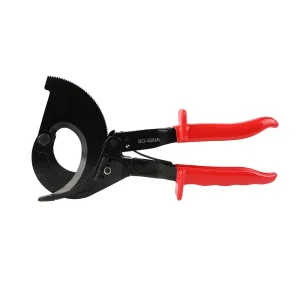
Comprehensive connection solutions spanning multi-conductor European pliers, heavy cable shear cutters, and solar array tools.
In-depth responses compiled by our chief technical specialists for hardware distributors, OEM buyers, and electrical contractors.
Insulation sleeve fractures occur when crimping dies lack an independent secondary relief zone. SIBO’s pre-insulated dies (such as our SO-30J and SN-02C series) are CNC-machined with dual-stage cavities: a primary compression zone compacts the metallic barrel onto the conductor strands, while a precisely contoured radius gently forms the nylon or PVC insulation sleeve to act as strain relief without puncturing or stressing the polymer jacket.
Non-ratcheting pliers rely completely on operator discretion and hand strength, causing significant crimp height variations throughout a worker’s shift. A full-cycle ratchet mechanism remains locked until the tool reaches absolute bottom dead center, ensuring identical crimp height and mechanical tension on every single joint. If a foreign body blocks completion, an integrated safety release lever unlocks the mechanism immediately.
Yes. Operating our own EDM wire-cutting machines, CNC tooling centers, and hardening furnaces in Yueqing, SIBO provides complete ODM design services. Clients simply submit their terminal technical drawings or sample physical connectors with conductor specifications. Our engineering unit will generate 3D CAD/CAM die proofs, build pilot tooling, and supply metallurgical crimp cross-section reports within 15 to 20 working days.
We offer flexible tier structures tailored to regional brands and multinational importers. Standard wholesale orders with SIBO branding feature low baseline thresholds. For custom private-label solutions (custom handle dual-color molding, laser engraving of company trademarks, customized blister packs, or heavy-duty Oxford tool cases), MOQs generally start at 500 units per tooling configuration with full volume break discounts available.
