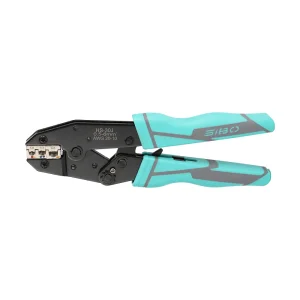
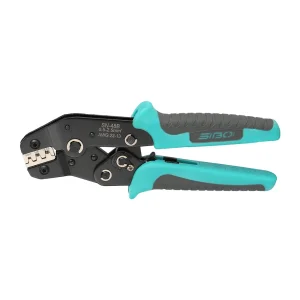
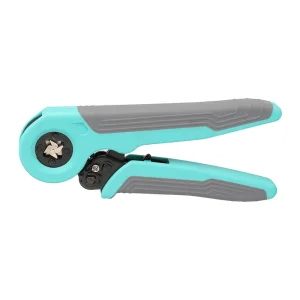
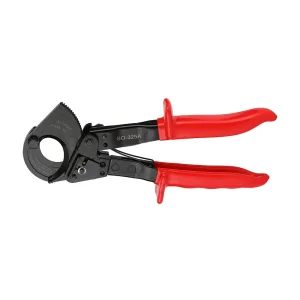
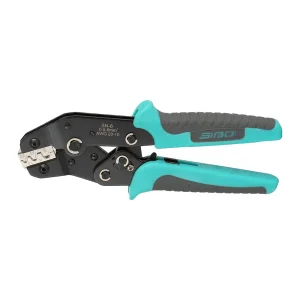
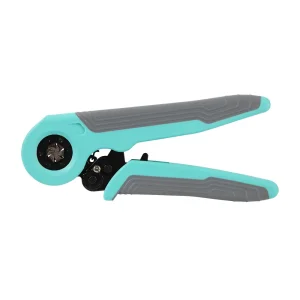
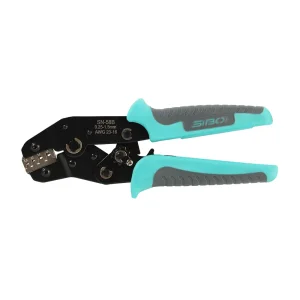
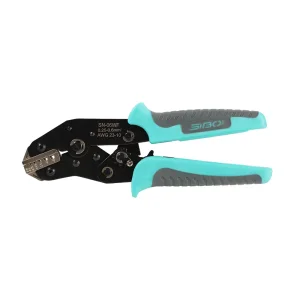
Explore our factory-calibrated lighting crimpers, self-adjusting wire ferrule pliers, and quick-change jaw sets engineered to eliminate cold crimps and contact resistance in smart lighting arrays.
The shift toward solid-state LED fixtures, automated DALI/DMX-512 driver topologies, and hazardous-location luminaires has transformed wire crimping from basic electrical installation to micro-tolerance electrical joint mechanics.
In contemporary luminaire manufacturing and high-density architectural electrification, the physical integrity of a terminal connection directly determines luminous longevity, driver efficiency, and thermal stability. Modern lighting installations have progressed far beyond standard incandescent lamp sockets; current applications feature complex low-voltage DC drive circuitry, micro-gauge signal interconnects (AWG 28 to AWG 18), constant-current LED array wiring, and severe outdoor environment luminaire nodes. When wiring architectural linear strips, high-bay factory floodlights, stadium array towers, or smart horticultural grow lights, a single substandard crimp leads to micro-arcing, intermittent flicker, junction heating, and accelerated component degradation.
A specialized Lighting Crimper must achieve cold-weld gas-tight compression under repetitive assembly line stress. Unlike general manual pliers, industrial lighting crimpers incorporate hardened carbon-steel jaws wire-EDM cut to fractions of a millimeter, paired with synchronized mechanical ratchets that prevent pre-release before the metal barrel transitions through its elastic deformation threshold into permanent plastic compaction. This ensures the copper strands and connector shroud merge into an oxygen-void mass with minimal millivolt drop.
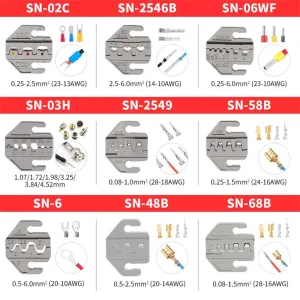
During the termination of luminaire wiring, three primary forces dictate connection quality: compaction ratio, pull-out retention force, and terminal barrel springback. When applying an open-barrel B-crimp or a hexagonal ferrule compression via tools like the SO-30J, SO-125 Pro, or SN-48B, the crimper jaws fold and burnish the tin-plated brass or copper terminal ears over uninsulated copper wire strands. SIBO Tools engineers our jaw cavity profiles to maintain an optimal 80% to 85% wire cross-sectional density compaction. This specific threshold displaces interfacial surface oxidation without compromising individual strand tensile integrity, satisfying the stringent mechanical pull-off benchmarks mandated by international standards such as IEC 60352-2 and UL 486C.
Precision-milled jaw dies create gas-tight metallic bonding that maintains low micro-ohm electrical resistance, preventing thermal hotspots across high-wattage LED driver feed lines.
Engineered strain relief crimping zones protect thin stranded lighting conductors against dynamic oscillations found in transit vehicles, tunnel installations, and wind-loaded street luminaires.
Forged from high-tensile alloy structural steel and hardened through dual-stage vacuum heat treatment, SIBO crimper pivot joints resist jaw misalignment over extended shift cycles.
Compound-action toggle levers reduce operator hand-squeeze pressure by up to 45%, reducing carpal stress and repetitive strain injuries during high-tempo industrial lighting pre-assembly.
Situated in Yueqing, Zhejiang Province — China’s premier capital of low-voltage electrical apparatus — SIBO Tools leverages a localized ecosystem of metallurgy, micro-tooling, and automated testing to outpace global lead times.
In global wholesale procurement, manufacturing velocity is not merely about rapid assembly line speeds; it represents the friction-free coordination of tool steel sourcing, precision wire-EDM (Electrical Discharge Machining), surface chemical blackening, continuous heat-treating, ergonomic plastic bi-material injection molding, and digital multi-stage QC calibration. Because SIBO Tools operates at the core of the Yueqing electrical industry hub, our manufacturing workflow eliminates cross-regional supply logistics bottlenecks.
Our vertical integration enables custom die cavity prototyping in as little as 5 to 7 business days, compared to the 6 to 8-week turnaround typical of Western European toolmakers. In-house computer-controlled stamping presses ranging from 60 to 250 metric tons fabricate tool chassis from high-purity structural carbon steel (AISI 1045 and 40Cr-Mo alloy), while automated computerized furnace lines treat jaw dies to an exact Rockwell hardness of HRC 42 - 48 for handles and HRC 58 - 62 for critical die teeth. This prevents die rounding, wall gouging, and dimensional degradation even after hundreds of thousands of terminal cycles.
From architectural LED ceiling systems to high-vibration automotive headlight assemblies, our lighting crimpers deliver specialized performance tailored to each wire cross-section and terminal family.
Linear luminaires, troffer panels, and magnetic track systems require compact connections to fit within extruded aluminum profiles. The SO-30J and SO-10-4 provide uniform ferrule and fork crimps that seat cleanly into push-in cage clamps without stray conductor whiskers.
Municipal lighting networks operate in demanding outdoor environments exposed to severe humidity, thermal cycling, and lightning surge conditions. Our heavy-duty ratchet crimpers ensure compression cable lugs and moisture-resistant splice sleeves maintain structural contact integrity under wind vibration.
Vehicle headlights, interior ambient LED harnesses, and trailer illumination arrays endure continuous mechanical shock and thermal swings. Tools like the SN-48B and SN-58B execute flawless dual-stage open-barrel crimps that lock both the conductor core and silicone weather seals.
Chemical refineries, offshore platforms, and manufacturing hangars utilize explosion-proof (ATEX/IECEx) luminaires where loose wiring could generate catastrophic spark ignition. The SO-125 Pro produces repeatable cold compression joints certified to withstand severe vibration without stress-loosening.
Contemporary smart lighting fixtures integrate microcontrollers, Bluetooth mesh radios, and PIR sensors requiring micro-pitch connectors such as JST, Molex, and Dupont headers. SIBO’s SN-58B series allows field technicians and factory line workers to crimp sub-miniature pins without damage.
How global environmental directives, smart ergonomic mandates, and automated quality testing protocols are reshaping the hand tool manufacturing ecosystem.
The industrial hand tool sector is undergoing rapid modernization driven by Industry 4.0 production guidelines and stringent occupational safety standards. Modern lighting equipment procurement departments no longer purchase non-ratcheted crimping pliers due to the associated failure rates and warranty liabilities. Today, enterprise procurement directors, private-label tool conglomerates, and Tier-1 lighting OEMs enforce strict verification parameters before approving a manufacturing vendor:
1. Mechanical Retention Tensile Verification: Wire crimps must undergo rigorous motorized tensile pull testing. For instance, an AWG 14 (2.5mm²) terminal joint must withstand a sustained pull force exceeding 220 Newtons without conductor slippage or core rupture, complying with UL 486C criteria.
2. Contact Resistance & Millivolt Drop: Across multi-thousand-hour operating spans in commercial lighting fixtures, contact resistance cannot exceed initial baseline values by more than 1.5 milliohms. SIBO's micro-machined jaw radii prevent excessive necking down of stranded conductors while maintaining low resistance.
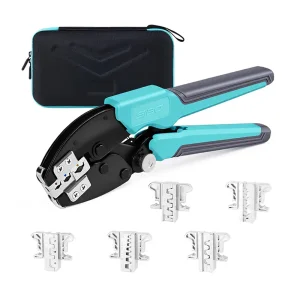
3. Magnetic Quick-Change Modular Tool Platforms: Rather than carrying five distinct pliers to an installation site, field electricians demand modular systems. SIBO's patented quick-replacement magnetic jaw sets allow instant changeovers between insulated, non-insulated, ferrule, and solar MC4 dies in under five seconds without external screwdrivers or alignment jigs.
| Tool Model | Applicable Terminal Profile | Wire Capacity (mm² / AWG) | Jaw Material & Hardness | Mechanism Type |
|---|---|---|---|---|
| SO-30J Pro | Pre-Insulated Ring / Spade / Butt Connectors | 0.5 - 6.0 mm² (AWG 20 - 10) | AISI 4140 Alloy Steel / HRC 58±2 | Full-Cycle Ratchet with Quick-Release Lever |
| SN-48B | Non-Insulated Open Barrel & Automotive Tabs | 0.14 - 1.5 mm² (AWG 26 - 16) | High-Carbon Tool Steel / HRC 60±1 | Progressive Double-D-Crimp Dual Axis |
| SO 10-6 Pro | Self-Adjusting Hexagonal Wire Ferrules | 0.08 - 10.0 mm² (AWG 28 - 7) | Vacuum-Treated Tool Steel / HRC 59±2 | 6-Synchronized Cam Self-Adaptive System |
| SN-58B | Precision Micro-Pitch Dupont / JST / Molex | 0.08 - 1.5 mm² (AWG 28 - 16) | High-Precision Wire-EDM Cut Die Steel | Compound Leverage Ratchet with Calibrator |
| FST-325A | Heavy-Duty Copper & Aluminum Cable Shearing | Max 240 mm² / 500 MCM Cable | Drop-Forged 65Mn Alloy Blade / HRC 62 | Ratcheting Guillotine Drive with Spring Return |
SIBO Tools functions as the primary contract manufacturing partner for international brand owners, electrical wholesale distributors, and hardware retail franchises. Our full OEM/ODM manufacturing suite encompasses:
Critical technical considerations, procurement parameters, and manufacturing standards addressed by our senior applications engineering team.
Broaden your distribution inventory with our high-volume micro-pitch connector crimpers, self-adaptive hex ferrule tools, and comprehensive multi-jaw contractor kits.
Partner directly with Yueqing Sibo Tools Manufacture Co., Ltd. for factory pricing, guaranteed die repeatability, and full OEM packaging solutions. Request our comprehensive industrial catalog and sample kits today.