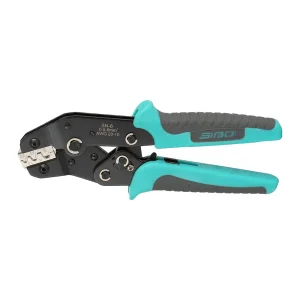
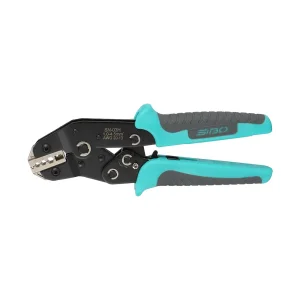
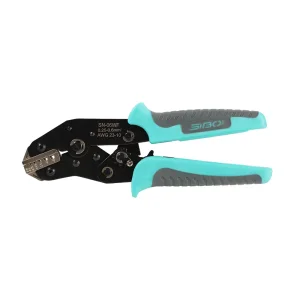
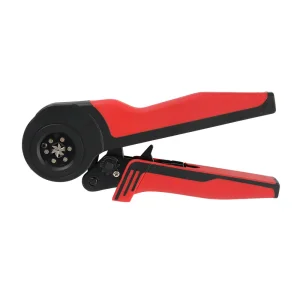
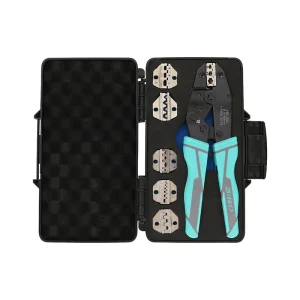
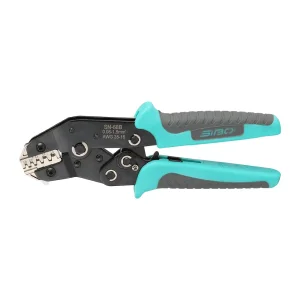
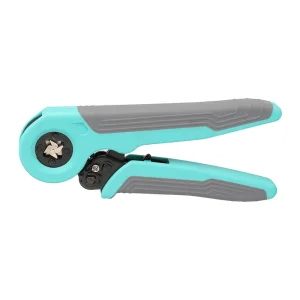
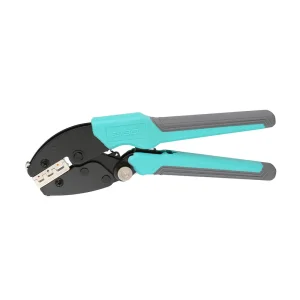
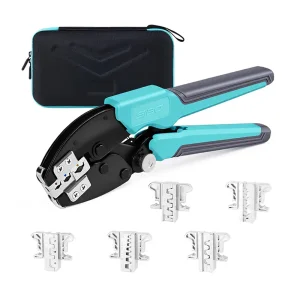
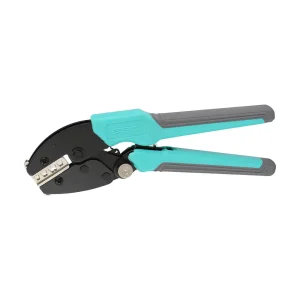
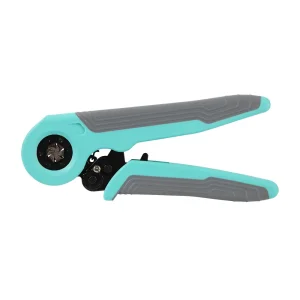
Engineered for repeatable radial tolerance, anti-fatigue mechanical advantage, and harsh jobsite longevity. Explore our factory-direct wholesale crimping assemblies.
Evaluating regulatory compliance, cross-linked polyethylene pipe adoption, and the structural transition from copper soldering to cold-mechanical jointing.
In modern mechanical plumbing and hydronic heating infrastructure, cross-linked polyethylene (PEX-a, PEX-b, and PEX-c) has emerged as the global benchmark material, displacing copper and galvanized steel. The physical integrity of these installations rests entirely upon the mechanical reliability of the mechanical joint—primarily executed via ASTM F1807 / ASTM F2159 copper crimp rings or ASTM F2098 stainless steel clamps (pinch clamps). As a premier Chinese manufacturer headquartered in the manufacturing cluster of Yueqing, Zhejiang, our engineering initiatives address the macro demands of high-volume wholesalers, private-label enterprise brands, and major engineering EPCs worldwide.
The global PEX crimper sector is characterized by strict convergence between metallurgy, mechanical leverage tolerances, and regulatory standards. In North America, the International Plumbing Code (IPC) and Uniform Plumbing Code (UPC) enforce rigid Go/No-Go gauge calibrations. In Europe and Australasia, EN ISO 21003 and AS/NZS 2537 dictate distinct radial compression profiles. Consequently, selecting an authorized wholesale PEX crimper manufacturer is no longer merely a pricing calculation; it is a critical safeguard against catastrophic catastrophic water damage, building litigation, and warranty liabilities.
While fitting and pipe costs are static, 85% of downstream installation failures stem from under-crimped or ovalized rings. High-leverage, calibrated tooling mitigates workforce-induced joint failures.
OEM suppliers must manufacture to dual-standard benchmarks: ASTM F1807 (copper ring crimp), ASTM F2159 (engineered plastic fittings), and CSA B137.5 for North America, alongside CE and DIN compliance.
Precision EDM-machined 40Cr carbon steel and 42CrMo drop-forged jaws guarantee that dimensional tolerances remain under ±0.03mm over 30,000 continuous compression cycles without recalibration.
A comprehensive metallurgical and kinematic assessment of connection methods, enabling B2B purchasers to select optimal inventory configurations.
| System Type | Applicable Standards | Tool Mechanism | Mechanical Advantage | Field Inspection Mechanism | Production Cost Index |
|---|---|---|---|---|---|
| Copper Crimp Ring (ASTM F1807) | ASTM F1807, ASTM F2159, CSA B137.5 | Toggle Linkage / Full-Cycle Ratchet | 33:1 Compound Leverage | Go / No-Go Caliper Gauge | Optimal / High Volume |
| Stainless Steel Clamp (ASTM F2098) | ASTM F2098, NSF/ANSI 14/61 | Ratchet Pinch Jaw with Auto-Release | 28:1 Mechanical Ratio | Visual Tab Collapse Indent | Economical / Flexible |
| Axial Cold Expansion (ProPEX) | ASTM F1960, CSA B137.5 | Cone Expander + Axial Sleeve Press | Hydraulic / Multi-Segment Expander | Visual Collar Seating Verification | Premium Enterprise |
| Multi-Layer Composite (PEX-AL-PEX) | EN ISO 21003, DIN 16836 | Radial TH / U / V Profiling Dies | Linear Gear Drive / Electro-Hydraulic | Acoustic Click / Stroke Control | Specialized / Infrastructure |
Our patented ratchet lock mechanisms prevent premature release. The jaws will not disengage until the toggle linkage reaches bottom dead center (BDC), generating up to 1,200 kg of radial force. This guarantees 100% full-stroke closure regardless of technician fatigue or arm positioning.
Every crimp die jaw undergoes computer-controlled vacuum carbonitriding, achieving a surface hardness of HRC 58-62 while maintaining core ductility at HRC 42-45. This dual-phase microstructure prevents catastrophic brittle fracture during cold weather field operations (-20°C to +50°C).
Tailored tool configurations optimized for specific regional building codes, climate demands, and structural architectural constraints.
Engineered for 16-inch center joist bays and wall stud cavities. Our angle-head crimpers and mini-profile jaws allow single-handed operation in confined spaces without sacrificing ASTM F1807 perimeter compression integrity.
Optimized for radiant underfloor heating and multi-layer PEX-AL-PEX distribution headers. Self-adjusting and interchangeable die sets eliminate tool proliferation for mechanical contractors installing 12mm to 32mm lines.
Designed for large-diameter sub-slab, trench, and municipal water service entries. Heavy-duty toggle mechanisms deliver linear radial crimp on 1-inch and 1-1/4-inch heavy-gauge copper rings without operator slippage.
High-temperature solar glycol return loops require joint tooling that retains calibration under severe thermal-cycling conditions. Our heat-stabilized jaw designs prevent loose joints under high thermal expansion.
Automated bench-top and pneumatic crimping integration for off-site volumetric modular bathroom pod construction, maintaining 100% joint traceability and uniform crimp depth in high-throughput production lines.
Equipped with specialized zinc-nickel alloy plating to resist extreme marine saltwater fog and moisture in luxury yachts, commercial ships, and coastal modular residences.
Where mechanical engineering converges with sensor telemetry, lightweight composite alloys, and predictive QA documentation.
Reduction of total tool mass by 38% utilizing aircraft-grade forged aluminum and titanium mechanical linkages, curbing repetitive strain injuries (RSI) across 8-hour construction shifts.
Embedded piezoelectric pressure sensors transmitting real-time peak compressive force (kN) via Bluetooth to cloud compliance dashboards, creating undeniable warranty proof for commercial plumbing contractors.
Single hand-frame accommodating copper ring (ASTM F1807), stainless clamp (F2098), and European axial press sleeves (TH/U profile) with tool-less magnetic release in under 3 seconds.
Complete elimination of single-use PVC blisters in wholesale distribution, replaced by heavy-duty 600D recycled Oxford tool storage bags and biodegradable molded pulp boxes.
SIBO Tools operates advanced 5-axis CNC machining centers, coordinate measuring machines (CMM), and automatic optical sorting equipment in Yueqing, Zhejiang. We offer turnkey ODM engineering:
How tier-1 wholesale distributors and national retail tool networks protect their brand equity through factory-direct governance.
Each tool is factory pre-calibrated against hardened master gauges. Our 100% end-of-line Go/No-Go screening guarantees that every tool departing our factory requires zero initial field adjustment.
We source certified high-grade alloy steel from certified domestic mills. Spectral chemical analysis and tensile yield verification documents are archived for every production batch.
Support for mixed-SKU full-container loads (FCL) combining manual PEX crimpers, self-adjusting ferrule crimpers, solar cable pliers, and ratchet cable cutters with localized port handling in Ningbo or Shanghai.
Clear, authoritative technical answers addressing die compatibility, OEM labeling, field adjustment, and standards certification.
ASTM F1807 applies to full-circle copper crimp rings compressed over brass or PPSU fittings using toggle-jaw pliers; inspection requires a Go/No-Go caliper checking finished diameter. ASTM F2098 specifies stainless steel pinch clamps where a ratchet tool pinches a central tab until mechanical release occurs, verified by tab closure.
Our tools feature an integrated eccentric calibration dial. Loosening the locking set screw allows micro-rotation of the eccentric pivot pin, compensating for mechanical wear and returning jaw clearance to exact ASTM F1807 Go/No-Go specifications in under 60 seconds.
For laser-etched custom logos on existing tool frames, our baseline MOQ starts at 300 units. For fully customized dual-color ergonomic handle grips and private-label retail packaging, the typical MOQ is 1,000 units per model.
No. Copper rings require 360-degree radial inward compressive force to shrink the ring circumference, whereas stainless steel pinch clamps require a pincers-type jaw that draws an raised ear together until flat. We manufacture dedicated tools for both systems.
Every production run undergoes 100% visual inspection, optical comparator die profile measurements, Rockwell surface hardness testing, and a 1,000-crimp destructive pressure test verifying burst strength beyond 300 PSI on standard PEX-B tubing.
Standard production lead times for consolidated 20ft containers average 25–35 days from technical sign-off and deposit receipt. Expedited reorders for established OEM partners can be fulfilled in 15–20 days via our strategic parts buffer inventory.
Expanding your product line with verified commercial ratchet, ferrule, and photovoltaic connection hand tools directly from our Yueqing factory.