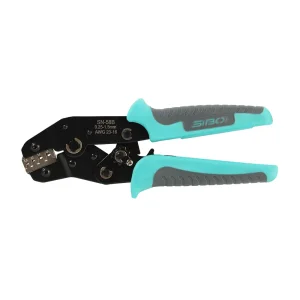
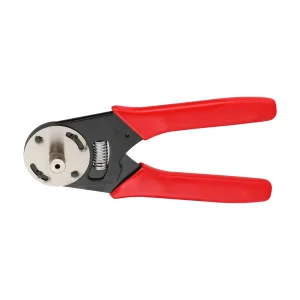
High-demand precision manual and ratchet crimping tools calibrated to meet strict CE, RoHS, and DIN testing criteria across Bucharest, Timișoara, Cluj-Napoca, and Pitești assembly lines.

Romania has firmly positioned itself as a critical manufacturing powerhouse within the European Union, functioning as a high-density node for automotive wiring harness production, smart energy transition, and machine assembly.
Romania serves tier-1 multinational automotive contract manufacturing for brands like Dacia-Renault, Ford Otosan, Continental, Draxlmaier, Leoni, and Yazaki. In modern harness architectures, cold-welded crimp terminations must withstand heavy road vibration, severe thermal cycles (-40°C to +125°C), and micro-voltage degradation without solder reliance.
Bolstered by EU Modernisation Funds and the Romanian National Recovery and Resilience Plan (PNRR), utility-scale photovoltaic farms and wind facilities are scaling exponentially. Solderless field termination using MC4, H4, and solar cable lug crimping demands airtight joints that avert hot spots, dielectric breakdown, and destructive micro-arcing.
From modern logistics parks outside Bucharest to high-tech machinery workshops across Cluj-Napoca, industrial panel builders mandate consistent ferrule and spade crimping under DIN 46228 standards. Under-crimping risks terminal pull-out and electrical fires; over-crimping cuts fine stranded copper strands, diminishing current capacity.
Industrial buyers across the European Single Market do not evaluate crimping pliers as simple hardware accessories—they treat them as calibrated precision instruments that define conductor mechanical retention and electrical conductance.
| Evaluation Parameter | SIBO Classic Industrial Specification | DIN EN 60352-2 Standard Requirement | Quality Impact on Romanian Job Sites |
|---|---|---|---|
| Crimp Height & Width Ratio | ±0.03 mm strictly calibrated via wire EDM | Within connector manufacturer tolerance | Prevents strand thinning or incomplete compaction voids |
| Mechanical Pull-Out Force | 125% of IEC minimum required rating (e.g. >360N on 4.0mm²) | Mandatory minimum tensile pull threshold (N) | Prevents harness dislocation under continuous automotive vibration |
| Metallographic Compaction | >85% honeycomb gas-tight solid cross-section | Zero uncompressed interstitial air pockets | Immunity to atmospheric oxidation in coastal or humid environments |
| Contact Resistance (mΩ) | <1.8 mΩ total loop resistance per joint | Negligible increase across test cycles | Averts thermal runaway and power transmission loss in PV arrays |
| Mechanism Life Cycle | >50,000 ratcheting cycles without frame deflection | Not specified (standard tools degrade <10k cycles) | Significantly reduces tool amortization and total procurement cost |
Based in Yueqing, Zhejiang—the epicenter of global low-voltage electrical tooling—SIBO tools integrate automated production lines, metallurgical precision, and agile OEM supply chains serving Romanian distributors directly.
Cheaper commercial pliers rely on stamped mild steel that twists under high leverage. SIBO jaws and leverage linkages are forged from high-tensile 42CrMo and cold-rolled alloy steel plates, ensuring zero mechanical flex even after 35,000 continuous ratcheting cycles.
Through computer-controlled multi-stage quenching and salt bath vacuum carburizing, our die sets reach an exact surface hardness of HRC 48-52 while preserving internal core ductility. This prevents jaw fractures when processing high-toughness nickel-plated brass terminals.
By controlling all tooling operations in-house—die-sinking EDM, stamping, CNC grinding, surface black-oxide finishing, and dual-color TPR handle molding—we compress lead times to under 25 days, shipping seamlessly via maritime corridors to Constanța Port or rail to European consolidation centers.
From cleanroom automation labs to high-humidity outdoor agricultural substations, explore how classic crimping tools are deployed across Romanian key sectors.
Used widely across repair depots and Tier-2 wiring sub-suppliers in Craiova and Pitești. Pliers with open-barrel B-crimp cavities securely fold both conductor strands and insulation support wings simultaneously, complying with OEM harness rebuild protocols.
Romania's national rail overhaul initiatives demand vibration-proof, flame-retardant electrical terminations. Self-adjusting square and hexagonal ferrule crimpers compress multi-stranded conductors into dense geometric geometries that seat without screw loosening inside WAGO-style cage clamps.
Field installations in Brasov and Iasi demand fast, error-free crimping of 4mm² and 6mm² PV cables under extreme sunlight exposure. Our specialized ratchet tools with built-in locator pins hold the open MC4 terminal securely in place prior to closure, preventing human misalignment.
Clear, technically verified answers addressing pull-out compliance, private labeling, custom die engineering, and European import procedures.
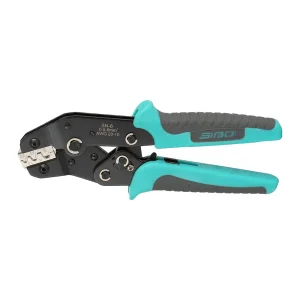
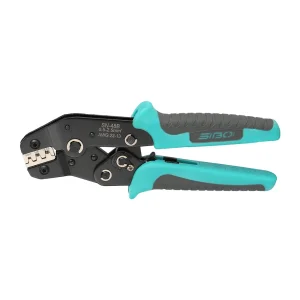
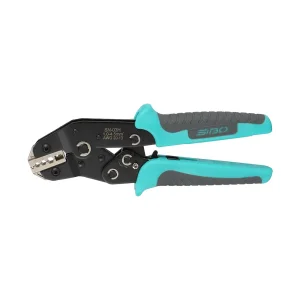
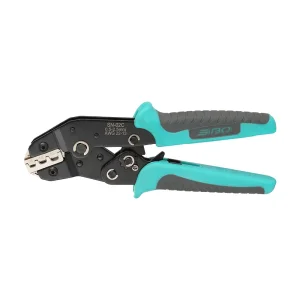
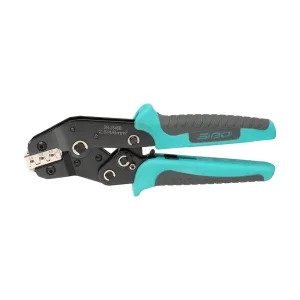
Engineered for durability, ergonomic grip, and universal conductor compatibility. Explore our high-volume factory catalog serving Romanian wholesale distributors.

Whether you require standard wholesale volumes, specialized custom EDM die cavities, or full turnkey OEM branding for the Romanian market, our engineering team responds with technical drawings and quotations within 24 hours.