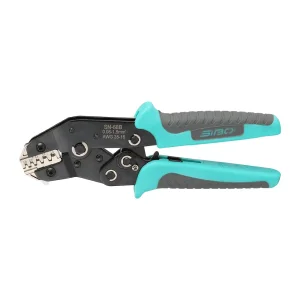
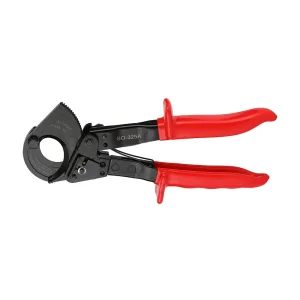
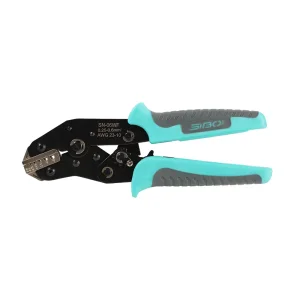
Direct factory configurations engineered for repeatable pull-out force, standardized contact resistance, and ergonomic industrial assembly.

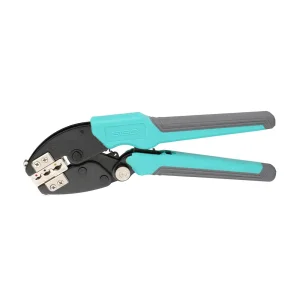
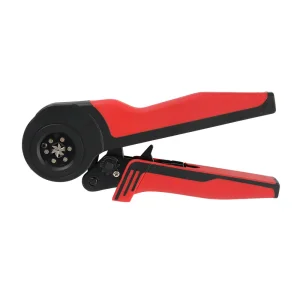
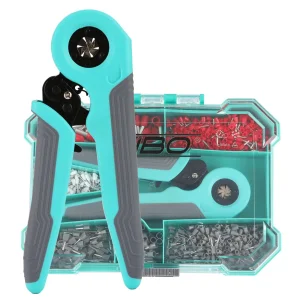
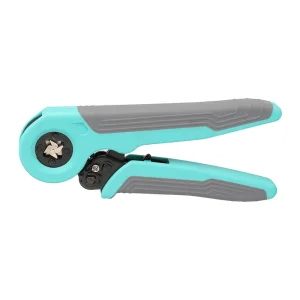

In modern industrial electrical distribution, photovoltaic energy systems, aerospace, and high-frequency wire harness manufacturing, a crimped termination is not merely a mechanical fold—it is a cold-welded metallurgical molecular interface.
A hand crimping tool must systematically transform multi-strand copper conductors and a stamped or machined terminal barrel into a homogenous solid mass. According to DIN EN 60352-2 and IEC 60352-2 standards, a compliant crimp requires the total expulsion of air voids from the conductor compaction envelope, preventing contact resistance spikes, thermal hotspots, galvanic corrosion, and vibrational mechanical failure over decades of field service.
Yueqing Sibo Tools Manufacture Co., Ltd., based in Yueqing, Zhejiang—the global capital of low-voltage electrical apparatus—operates at the exact convergence of metallurgical science and structural kinematics. By employing vacuum-quenched alloy tool steels, computer-optimized mechanical compound-leverage linkage, and calibrated full-cycle micro-tooth ratchets, our tools deliver consistent terminal compression force without premature jaw release or plastic handle deflection.
Whether processing delicate 0.08 mm² (AWG 28) electronics wire ferrules or heavy-duty solar PV connector cables exceeding 6.0 mm² (AWG 10), Chinese precision tool engineering guarantees that the operator’s manual exertion translates into an exact, micrometer-calibrated crimp height.
The production of hand crimping pliers in China has transformed from low-tier labor-intensive assembly to advanced, automated, vertically-integrated industrial precision engineering.
Located in Yueqing, Zhejiang Province, our manufacturing infrastructure interfaces directly with the world’s most concentrated supply chain for electrical terminals, copper lugs, switchgear accessories, and tooling dies. Proximity to wire-EDM die makers, progressive stamping lines, and automated electroplating facilities cuts prototype turnarounds from months to days.
Unlike conventional investment-cast jaws prone to internal porosity, our dies undergo Slow-Feeding Wire Cut Electrical Discharge Machining (Wire EDM) after vacuum quenching. This achieves a profile repeatability of ±0.005 mm. Conductor strands cannot leak into parting lines, ensuring flash-free, perfectly symmetrical crimps every cycle.
Through proprietary automated stamping lines and continuous computerized heat-treatment kilns, our Yueqing factory provides top-tier German-grade dimensional stability and metallurgy at 40%–60% lower total procurement cost, allowing international tool distributors and wholesalers to capture strong retail margins and market share.
From self-adjusting quadrangular geometries to ergonomic leverage kinematics, the next generation of hand crimping pliers is driven by automation, occupational ergonomics, and renewable energy grids.
The global market is migrating rapidly toward self-adjusting ferrule crimpers (e.g., SIBO SO-16-4 square and SO-16-6 hexagonal series). Instead of fixed cavities requiring manual cross-section selection, multi-synchronized sliding cam segments dynamically compress ferrules from 0.08 to 16 mm², eliminating operator error and optimizing rectangular terminal block fitment.
With utility-scale solar arrays moving to 1500V DC system voltages, poor field terminations directly cause catastrophic electrical arcs and fire hazards. Modern solar hand crimpers (such as the SO-2546 Pro series) incorporate dedicated locating positioners and specialized B-crimp cavities for genuine MC4, MC4-EVO2, and compatible connectors on 2.5, 4.0, and 6.0 mm² PV cables.
Repetitive strain injuries (RSI) across panel builders and electrical wire harness workshops are driving stringent ergonomic regulations. Factory advances feature dual-compound TPR/PP slip-proof handles, optimized handle opening spans (under 60 mm at initial grip), and toggle-link mechanical transmissions that yield peak mechanical advantage exactly at the point of terminal deformation.
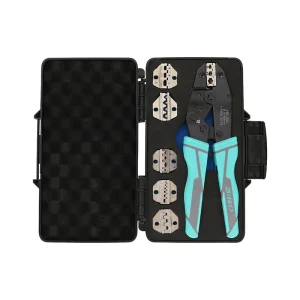
Field engineers demand versatile multi-use tool platforms without carrying dozens of heavy individual pliers. Combination kits like the HS-30J 5-Jaw Set and magnetic tool-less rapid jaw couplers enable instant changeovers between pre-insulated red/blue/yellow terminals, uninsulated lugs, bootlace ferrules, and open-barrel automotive terminals in seconds.
Deploying hand tools across harsh environments requires matching the crimping mechanical profile to the unique thermal, chemical, and physical stresses of each vertical industry.
On a 100 MW utility PV site, over 200,000 field-made DC crimps endure 30 years of thermal cycling, UV radiation, and heavy humidity. Using high-precision tools such as the SO-2546C Pro solar crimper ensures contact pull-out values exceed 310 Newtons, contact resistance stays below 0.25 mΩ, and thermal camera inspections reveal zero hot-spot variance.
High-density PLC I/O modules and DIN-rail terminal blocks rely on bootlace ferrules conforming to DIN 46228 Part 1 & Part 4. Self-adjusting pliers (SO 16-4, SO 10-4) compress thin stranded flex conductors into uniform rectangular blocks that will not splay or shear under screw-clamp or spring-cage vibration.
Vehicle engine bays and marine engine compartments experience intense vibration and saltwater fog. Open-barrel pliers (SN-2549, SN-68B) deliver authentic dual-stage B-crimps: one stage rolling the conductor wings into the bare copper core, and the second rolling the insulation wings around the cable jacket for essential mechanical strain relief.
International tool brands, private-label distributors, and supply-chain directors must verify these engineering verification criteria before signing OEM agreements.
| Inspection Dimension | Critical Quality Parameter | Standard / Verification Protocol | SIBO Yueqing Factory Benchmark |
|---|---|---|---|
| Mechanical Pull-Off Force | Wire tensile retention without terminal slippage | UL 486A-B / IEC 60352-2 / DIN EN 60352 | 120% to 140% above nominal safety limits |
| Crimp Height & Width | Micro-dimensional repeatability under load | Calibrated Digital Micrometer (±0.01 mm) | Total cavity variance controlled within <0.02 mm |
| Ratchet Life Span | Zero mechanism slip or tooth disengagement | Automated Pneumatic Actuation Bench Test | >50,000 full-cycle actuations verified |
| Polymer Handle Safety | No cracking, chemical leaching, or slipping | RoHS 2.0 / REACH (SVHC List) compliance | Dual-injection virgin TPR/PP handles |
| Micrography Void Ratio | Cross-sectional microscopic gas-tightness | Metallographic Polish & Optical Microscopy | Zero internal air gap; compacted gas-tight matrix |
We offer complete private-label engineering: dual-tone handle mold injection with custom Pantone corporate colors, laser-etched high-contrast vector logos on plier bodies, and branded blow-molded or Oxford canvas packaging tailored for retail distribution.
Have a proprietary connector geometry or custom stamped terminal? Our in-house CAD/CAM tooling department produces custom wire-EDM test die cavities within 7 to 10 working days, backed by comprehensive tensile pull-test and cross-section micrography reports.
With shipments to Europe, North America, Japan, and the Middle East, our Yueqing factory maintains end-to-end batch traceability from raw alloy steel heat lots down to assembly batch numbers, ensuring seamless customs entry and zero recall liability.
Direct technical answers from SIBO tool designers addressing mechanical failure modes, die selection, calibration, and OEM supply chain agreements.
Explore our specialized open-barrel automotive crimpers, heavy ferrule ratchet tools, and clean-cut cable shears manufactured in Yueqing, China.