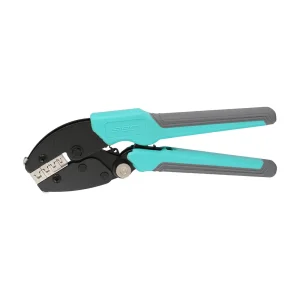
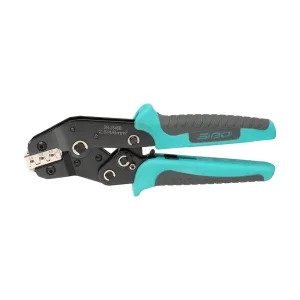
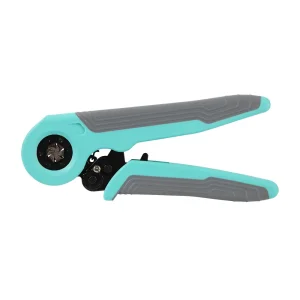
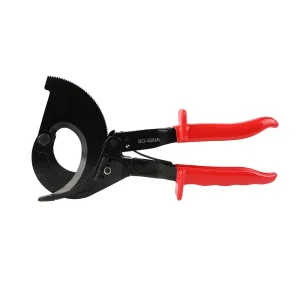
Explore our industrial-grade crimping hand tools, engineered in Yueqing for repeatable tensile strength, exact crimp height (CH), and zero terminal distortion across high-reliability wiring harnesses.
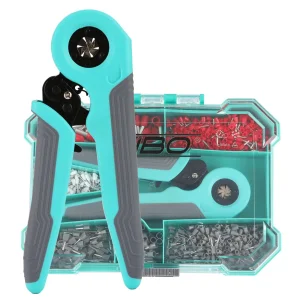
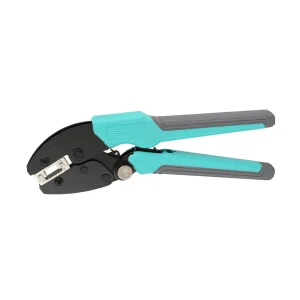
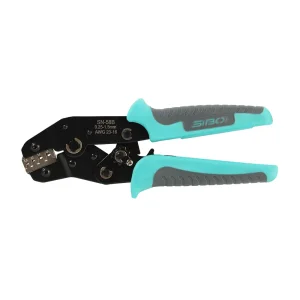
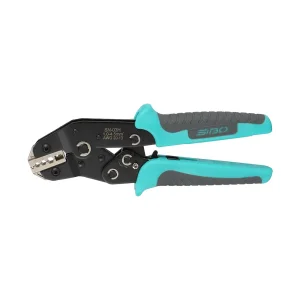
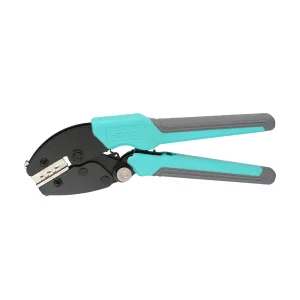
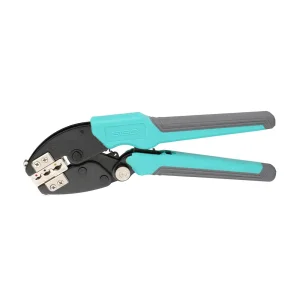
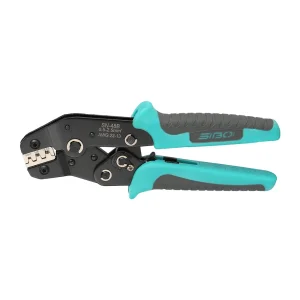

In electrical harness fabrication, a crimp joint is not merely a mechanical fold—it is a cold-welded metallurgical gas-tight bond. Explore how custom Molex crimper manufacturing controls microscopic compaction parameters.
Proper crimping of Molex open-barrel terminals (such as Micro-Fit 3.0, Mini-Fit Jr., and KK 254) demands high-precision deformation. Our dies generate sufficient radial compression to disrupt individual copper strand oxide films, cold-flowing copper into terminal brass without void spaces.
Unlike generic stamped tools that fracture fine terminal wings, our customized Molex dies use slow-speed wire electrical discharge machining (WEDM). This creates ultra-smooth cavity geometry that simultaneously forms the conductor "B-crimp" and insulation support wrap.
Operator fatigue is the leading cause of field connection failure. Sibo Tools integrates factory-calibrated mechanical rachet locks with an over-center toggle mechanism, ensuring the jaws cannot disengage until exact nominal crimp closure is attained.
Located in Yueqing, Zhejiang—the global capital of low-voltage electrical apparatus—our manufacturing cluster provides unmatched metallurgical sourcing, tooling agility, and rapid production turnaround.
Yueqing hosts over 10,000 electrical component manufacturers. This proximity provides Sibo Tools with instant access to certified alloy steel supplies, vacuum heat-treatment centers, precision surface plating, and high-speed CNC turning workshops within a 15-kilometer radius.
Direct benefit: Raw material lead times reduced by 60%, delivering unprecedented prototype validation speeds.
We do not outsource critical manufacturing steps. From initial 3D parametric CAD modeling and die cavity flow analysis to computerized EDM wire cutting, stamping, assembly, and optical crimp-height cross-sectioning, our facility controls the entire lifecycle under ISO 9001:2015.
Direct benefit: Full lot-to-lot traceability and zero dependency on external sub-tier vendors.
By pairing high-tonnage automated progressive stamping presses with proprietary jaw calibration jigs, we achieve unmatched manufacturing throughput. International OEMs acquire bespoke, high-tolerance Molex-compatible tooling at 30% to 50% lower tooling amortizations than European or Japanese competitors.
Direct benefit: Economical low-volume customization for specialty harness configurations.
Reference technical parameters for wire gauge capability, crimp height tolerances, and pull-out retention force according to IPC/WHMA-A-620 Class 3 specifications.
| Molex Terminal Family | Pitch Dimension | Wire Range (AWG / mm²) | Crimp Height (CH) Target | Min Pull-Out Force (UL) | SIBO Matched Tool Series |
|---|---|---|---|---|---|
| Micro-Fit 3.0™ (43030 / 43031) | 3.00 mm | AWG 20 - 30 (0.50 - 0.05 mm²) | 0.76 - 0.96 mm ±0.03 | 58 N (AWG 20) | SN-58B Series / Custom EDM |
| Mini-Fit Jr.™ (5556 / 5558) | 4.20 mm | AWG 16 - 28 (1.30 - 0.08 mm²) | 1.12 - 1.45 mm ±0.04 | 88 N (AWG 16) | SN-48B / SO-056FL-Pro |
| KK® 254 / KK® 396 | 2.54 / 3.96 mm | AWG 18 - 30 (0.82 - 0.05 mm²) | 0.89 - 1.25 mm ±0.03 | 67 N (AWG 18) | SN-58B Pro / SO-04B |
| PicoBlade™ 1.25 | 1.25 mm | AWG 26 - 32 (0.13 - 0.03 mm²) | 0.48 - 0.62 mm ±0.02 | 19.6 N (AWG 26) | Custom Ultra-Micro EDM |
| Standard .093" / .062" Pin & Socket | Standard Pitch | AWG 14 - 24 (2.08 - 0.20 mm²) | 1.38 - 1.82 mm ±0.05 | 110 N (AWG 14) | SO-10 Pro / SN-03H Series |
We serve industrial tool importers, automotive tier-1 suppliers, and specialty contract manufacturers across North America, Europe, and Asia with tailored private-label capabilities.
Build your brand equity with custom dual-color handle moldings, laser-etched jaw part numbers, corporate Pantone matching, and custom Oxford carry cases or high-impact clamshell packaging ready for distributor showroom floors.
Send us your terminal samples, CAD profiles, or cable specification sheets. Our Yueqing R&D engineering team designs custom EDM electrode geometries, producing functioning sample dies in as little as 10 business days.
All tool bodies, plastic grips, and carbon steel assemblies adhere to strict EU and US environmental protocols. We supply comprehensive RoHS 2.0 test certificates, REACH SVHC declarations, and California Proposition 65 compliance reports.
From electric mobility to medical diagnostic racks, custom Molex-compatible crimpers are evolving toward tighter pitch tolerances, smart feedback mechanisms, and automated field servicing.
Battery Management Systems (BMS) in modern Electric Vehicles utilize ultra-compact Molex Micro-Lock Plus and DuraClik connectors. Our calibrated tools guarantee continuous continuity under intense thermal vibration and mechanical shock cycles.
Power distribution units (PDUs) and server blade backplanes employ high-density Molex Mini-Fit and Mega-Fit interconnects. Accurate crimp geometry maintains minimal bulk resistance, preventing catastrophic thermal hotspots under 24/7 load.
As board-to-board connectors shrink past 1.0mm down to sub-millimeter pitches, manual crimping is moving toward integrated optical alignment aids, quick-insert locator nests, and digitized stroke counters ensuring strict preventive maintenance auditing.
Direct technical answers from Yueqing Sibo Tools' senior toolmakers on tolerance control, maintenance, calibration, and OEM delivery schedules.
We replicate genuine performance by analyzing original terminal spec sheets and metallurgical sample sections. Our dies undergo precision slow-feeding wire EDM, ensuring identical horn angles, crimp height (CH), crimp width (CW), and bell-mouth extrusion radii as recommended by the connector manufacturer.
For existing standard hand tool frames with custom-engineered EDM jaws, our MOQ begins at 100 units. For fully customized frame forgings, specialized handle mouldings, or turnkey kits, MOQs typically range between 500 to 1,000 units depending on customization complexity.
Every tool model batch undergoes optical cross-sectioning (crimp micrography), micro-ohm resistance testing, and motorized pull-out tensile testing. We verify that conductor compaction achieves 15-20% copper extrusion without burring, wing rollover distortion, or copper wire strand severance.
Yes. By customizing the B-crimp height and cavity width, our engineers design stepped dies specifically calculated for two-wire insertions (common in automotive pass-through wiring) while maintaining full gas-tight integrity and meeting UL 486 pull-force minimums.
Explore our specialized range of flag terminal crimpers, high-power solar connector tools, and precision mechanical shears supporting industrial panel building and OEM production lines.