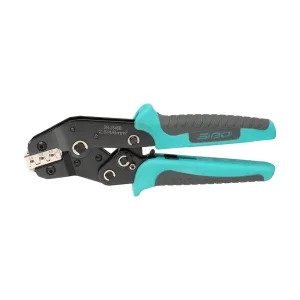
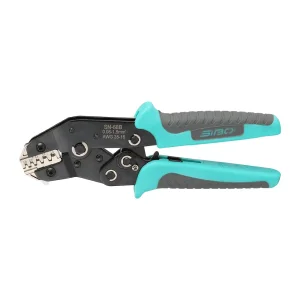
Explore our core series of heavy-duty ratchet crimpers engineered for insulated and non-insulated ring terminals, open barrel lugs, and high-integrity photovoltaic cable assemblies.


A technical treatise on mechanical deformation, metallurgical contact resistance, ratchet mechanism dynamics, and tooling longevity in high-reliability electrical infrastructure.
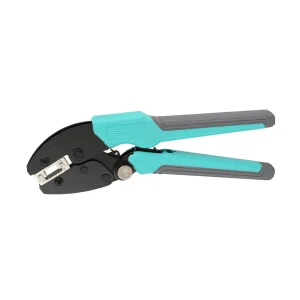
Achieving a certified crimped connection requires an exact volumetric balance between the cross-sectional area of the multi-strand cable (copper wire AWG 26 through 250 kcmil) and the internal volume of the ring terminal shank. When mechanical force is applied by an authentic SIBO ratchet crimper—such as our SO-056FL-Pro or heavy-duty SO-125 Pro series—the tool delivers a controlled force profile that drives the copper strands beyond their yield point into plastic deformation. This process shears the ambient copper oxide film, initiating cold welding across strand boundaries and forming a cohesive solid metal mass.
According to international benchmarks defined in IEC 60352-2 and UL 486A-B, an optimal ring terminal crimp must achieve a compaction ratio of 85% to 92%. Under-crimping leaves microscopic air pockets that foster atmospheric oxidation, escalating contact resistance and precipitating localized resistive heating. Over-crimping severely thins the conductive barrel wall and notches individual copper strands, causing premature mechanical failure under cyclic vibration. SIBO Tools solves this via wire-EDM die cutting, producing cavities with micrometer tolerances that precisely match the target ring terminal outer diameters and wall thicknesses.
Engineering Law of Hand Crimping: Manual operator strength varies between 150N and 450N. Relying on hand feel alone yields crimp height variations up to 35%. SIBO's integrated eccentric adjustment cams and hardened full-cycle ratchet mechanisms mechanically mandate 100% stroke completion, guaranteeing zero die release until uniform crimp compaction is achieved.
| Crimping Geometry | Typical Terminal Family | Compaction Density | Tensile Retention (IEC 60352-2) | Target Industrial Sectors |
|---|---|---|---|---|
| Double Indent (Conical Point) | Non-Insulated Seamless Tubing Ring Lugs | 90% - 94% | Exceeds 100% of nominal wire rating | Switchboards, Rail Rolling Stock, Substation Busbars |
| Confined Hexagonal | Wire Ferrules & Heavy Solid Barrel Ring Terminals | 88% - 92% | Uniform radial pull-out resistance | Automation Control Panels, Variable Frequency Drives |
| B-Crimp (Open Barrel Roll) | Stamped & Formed Sheet Ring / Spade Terminals | 86% - 90% | Independent conductor and insulation crimp | Automotive Wire Harnesses, Marine Outboards |
| Oval / Asymmetric Nested | Pre-Insulated (Vinyl / Nylon / PC) Ring Terminals | 84% - 88% | High mechanical grip without dielectric rupture | HVAC Control Wiring, Industrial Machinery, Appliances |
From gigawatt photovoltaic generation fields to high-frequency electric powertrain assembly, SIBO custom ring terminal crimpers resolve critical mechanical connection bottlenecks.
Utility-scale solar farms demand crimp consistency across thousands of string inverters and combiner boxes. Our dedicated solar crimpers like the SO-2546B Pro and SO-2546C deliver repeatable crimp heights for 2.5mm² to 6.0mm² solar conductors, withstanding UV radiation, thermal cycling (-40°C to +90°C), and micro-vibrations.
Modern commercial battery management systems (BMS) and e-mobility drive inverters require ring terminals to endure severe road shocks. Using open barrel tools such as the SN-68B and SO-04BPro, OEMs obtain precision B-crimps that isolate mechanical strain on the wire jacket while preserving copper conductor conductivity.
Within dense PLC panels and high-voltage switchgear, loose terminal rings cause devastating phase-to-phase short circuits. SIBO's SO-30J and SO-125 Pro series ensure insulated red/blue/yellow ring terminals are compressed without cracking the insulating collar, preserving 600V dielectric breakdown resistance.
Salt spray, galvanic corrosion, and continuous mechanical shock on marine vessels and high-speed rolling stock require gas-tight crimp seals. Our heavy-tonnage indent dies create seamless interfaces that prevent electrolyte ingress, meeting rigorous EN 50155 and DNV maritime electrical installation standards.
Navigating nearshoring trends, supply chain volatility, and private-label brand differentiation through integrated manufacturing clusters.
Global hardware conglomerates in North America and Western Europe increasingly rely on Yueqing's specialized tool manufacturing corridor. By outsourcing core forging, heat treatment, and ratchet calibration to SIBO Tools, international brands eliminate high domestic labor overhead while maintaining stringent DIN ISO 5743 metallurgical standards.
The proliferation of unhardened stamped steel crimpers in the spot market poses catastrophic risks to industrial projects. Incomplete heat treatment leads to jaw splaying after fewer than 500 cycles. SIBO guarantees high-carbon tool steel (such as 42CrMo and S50C) quenched and tempered to HRC 42-48, ensuring die tolerances stay within ±0.02mm across 50,000 cycles.
Different regional engineering ecosystems follow distinct terminal standards: North America utilizes color-coded vinyl/nylon ring terminals (AWG 22-10), Japan relies on JIS C 2805 closed-end ring lugs, while Europe mandates DIN 46234 non-insulated compression joints. SIBO's rapid tooling capability produces custom-matched jaw sets in 15 days, allowing distributors to capture localized niche tenders.
Every hand crimping tool delivered by Yueqing Sibo Tools undergoes strict empirical qualification to satisfy global statutory and industrial benchmarks.
Optical emission spectrometer checks alloy composition of incoming carbon tool steel batches.
Ultra-slow wire electrical discharge machining shapes the crimping cavity within ±0.015mm.
Multi-stage computerized heat treatment achieves HRC 45 core and HRC 50 jaw surface hardness.
Calibrated electronic tensile rigs execute destructive pull tests per UL 486A and IEC 60352-2.
Cross-sectional polishing reveals internal strand compaction ratio and validates zero gas permeability.
Beyond mechanical durability, SIBO Tools guarantees compliance with European Union RoHS (2011/65/EU) and REACH (EC 1907/2006) regulations. All dual-component TPR (thermoplastic rubber) ergonomic handle grips are formulated without toxic phthalates, polycyclic aromatic hydrocarbons (PAHs), or lead stabilizers. In addition, our manufacturing facilities operate in accordance with CE machine directives, ensuring export distributors can clear international customs smoothly.
How SIBO is modernizing manual crimping ergonomics through advanced metallurgy, digital validation, and eco-efficient manufacturing.
Integrating mechanical resonance clickers that output a distinct acoustic signature when full ratchet stroke compression is completed, alerting operators in high-noise shipyard settings.
Replacing standard solid carbon steel handles with forged aerospace aluminum-magnesium alloys to cut total tool weight by 38% without sacrificing mechanical yield strength under 15kN loads.
Developing micro-ratchet counter modules that log cumulative crimp cycles via NFC/Bluetooth, helping aerospace assembly plants automate maintenance schedules before wear tolerances are exceeded.
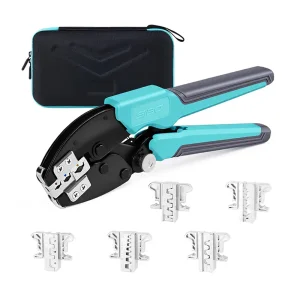
Upgrading our magnetic quick-change jaw patent to a push-button self-aligning lock system, enabling die exchanges in under three seconds with zero wobble and zero misalignment risk.
Direct answers from SIBO's Yueqing factory engineering department regarding custom specifications, die tolerances, minimum order quantities, and crimp certification.
Complete your catalog with factory-direct ratcheting pliers, adjustable hexagonal wire end ferrule crimpers, and professional energy-saving tools.
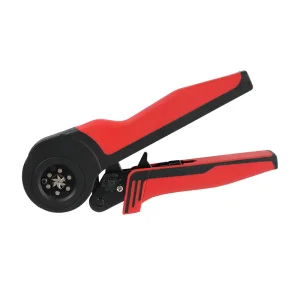
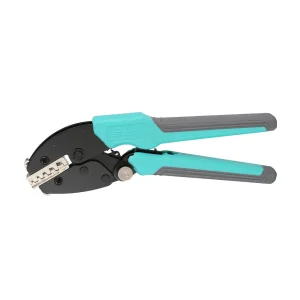
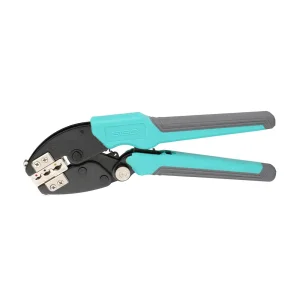
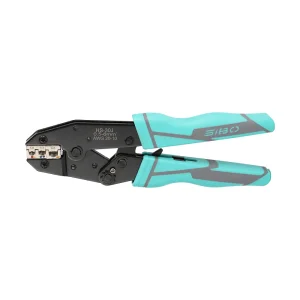
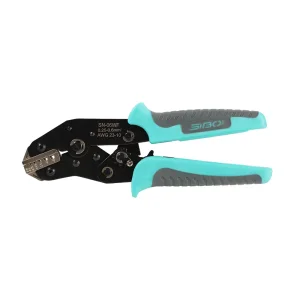
Whether you are a global brand seeking private-label manufacturing or an electrical distributor looking to expand your hand tool lineup, our engineering team provides end-to-end support—from initial die profile simulation to mass production and custom retail packaging.
