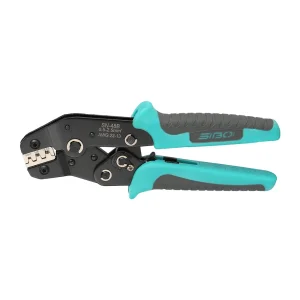
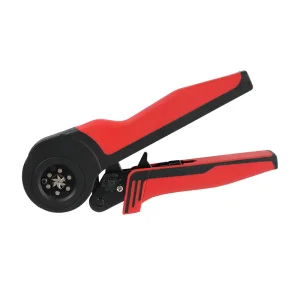
Explore our heavy-duty ratchet crimpers, self-adjusting ferrule pliers, and quick-change modular jaw sets manufactured under strict micron-level dimensional controls in Yueqing, China.

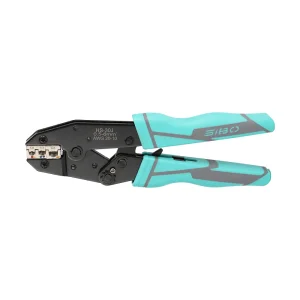
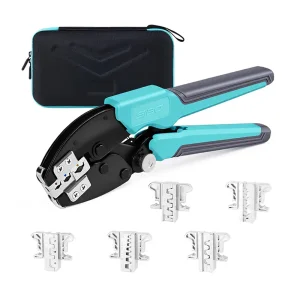

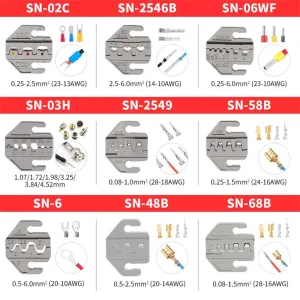
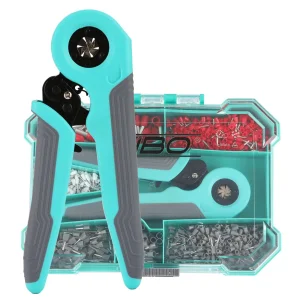
A high-performance crimper does far more than crush metal around wire strands; it induces controlled metallurgical compaction to establish a permanent, gastight, and vibration-proof electrical joint.
In modern industrial electrification, power transmission, and electronic control systems, solderless crimp connections serve as the critical conduit for high-amperage current transfer. The fundamental objective of the Superepoch crimper architecture is to eliminate air voids between flexible copper conductor strands and the terminal barrel. When the tool executes a mechanical cycle, compressive pressure forces the copper strands into a unified honeycomb structure. This micro-level cold plastic deformation breaks the natural insulating copper oxide layer, generating true metal-to-metal contact junctions without thermal embrittlement.
Incomplete compression creates internal micro-voids where atmospheric oxygen, moisture, and corrosive industrial gases enter. Over time, galvanic corrosion causes contact resistance ($R_{cont}$) to rise exponentially. Under high continuous currents, $I^2R$ power dissipation leads to localized overheating, accelerated insulation degradation, and hazardous thermal runaway. Conversely, excessive crimp pressure fractures individual copper filaments or thins the terminal barrel wall, dramatically reducing mechanical pull-out strength ($F_{pull}$) below standard thresholds. SIBO Tools solves this challenge by engineering calibrated leverage linkages, precision-ground tool steel jaw dies, and full-cycle release ratchets that eliminate human variability from every crimping cycle.
Operating from the global epicenter of low-voltage electrical engineering, Yueqing Sibo Tools leverages unmatched industrial clustering to provide superior precision, scalability, and cost efficiency.
Yueqing hosts over 10,000 electrical component manufacturers. SIBO sources certified alloy steels, specialized cold-drawn rods, and micro-injection molding within a 15-kilometer radius, drastically reducing material acquisition cycle times and component freight costs.
Our in-house toolroom utilizes Japanese slow-wire Electrical Discharge Machining (EDM) to produce crimping dies with tolerances within ±0.005mm. This guarantees consistent, burr-free crimping contours that match European and American connector profiles.
Structural handles and linkages are stamped from high-carbon manganese steel, while die jaws undergo multi-stage vacuum oil quenching and cryogenic stabilization. This prevents brittle fracture while maintaining core fatigue resistance over tens of thousands of cycles.
Enterprise buyers need more than competitive prices—they demand batch consistency, private label branding, and end-to-end quality governance.
Complete custom branding options including laser-etched brand identities, dual-injection TPR/PP handle color schemes, customized blister packaging, and rugged blow-molded or Oxford storage kits.
Statistical Process Control (SPC) with CPK ≥ 1.33 across core die profiles. Every batch is cataloged with tensile retention force and dimensional verification reports for full audit traceability.
Low initial MOQs for catalog validation combined with rapid container-load scalability. Distributors can mix ratchet pliers, cable cutters, and multi-piece ferrule kits in a single consolidated ocean container.
Dedicated toolroom engineers deliver customized die-profile samples within 14 business days from 2D/3D connector drawings, reducing development cycles for proprietary terminal shapes.
SIBO Superepoch hand tools undergo rigorous mechanical and electrical qualification tests to satisfy stringent North American, European, and Asian statutory safety regulations.
A high-quality industrial crimper must deliver joints that satisfy international standards for pull-out retention force, electrical resistance, and environmental resilience under thermal cycling. SIBO crimpers are validated against DIN EN 60352-2 (solderless crimped connections), UL 486A-486B (wire connectors), and IEC 60947-7-1 electrical distribution specifications. The table below outlines our factory mechanical verification thresholds compared to international baselines across standard AWG / metric conductor cross-sections:
| Wire Size (Metric) | Wire Gauge (AWG) | DIN EN 60352-2 Requirement | UL 486A-486B Minimum Pull Force | SIBO Tool Tested Retention | Die Contours Available |
|---|---|---|---|---|---|
| 0.5 mm² | 20 AWG | 50 N (11.2 lbf) | 40 N (9.0 lbf) | 68 N (15.3 lbf) | Insulated / Ferrule / Open Barrel |
| 1.0 mm² | 18 AWG | 108 N (24.3 lbf) | 90 N (20.2 lbf) | 135 N (30.3 lbf) | Color Coded Red Cavity |
| 2.5 mm² | 14 AWG | 230 N (51.7 lbf) | 220 N (49.5 lbf) | 285 N (64.1 lbf) | Blue Cavity / Solar MC4 Profile |
| 4.0 mm² | 12 AWG | 310 N (69.7 lbf) | 310 N (69.7 lbf) | 380 N (85.4 lbf) | Solar MC4 / Industrial Hex |
| 6.0 mm² | 10 AWG | 360 N (80.9 lbf) | 355 N (79.8 lbf) | 440 N (98.9 lbf) | Yellow Cavity / Solar SO-2546 |
| 10.0 mm² | 8 AWG | 500 N (112.4 lbf) | 400 N (89.9 lbf) | 620 N (139.4 lbf) | Indent Lug / Ferrule 16-6 |
Beyond mechanical pull strength, our factory conducts salt spray tests (ASTM B117 / ISO 9227) exceeding 72 hours on tool bodies and 120 hours on electroplated and black-oxide treated die components. Grip materials comply with EU REACH Annex XVII hazardous chemical requirements and RoHS Directive 2011/65/EU to prevent toxic plasticizer exposure during extended industrial handling.
Crimping tool manufacturing is transitioning from passive manual hardware to ergonomically optimized, modular, and application-specific engineered systems.
Utility-scale solar systems operating at 1500V DC require minimal contact resistance to prevent field fires. SIBO's SO-2546 Pro series integrates precision locators and micro-stepped crimp dies that deliver consistent terminal roll-in on stiff, double-insulated cross-linked polyethylene (XLPO) solar cables.
Traditional screw-retained crimping dies require manual disassembly, increasing tool downtime. Our magnetic jaw system uses rare-earth neodymium retention to allow technicians to swap between insulated, non-insulated, and ferrule profiles in under 5 seconds without screwdrivers.
Mini self-adjustable crimpers (such as the SO 16-6 series) replace single-cavity manual tools with six synchronously moving jaws. The mechanism self-compensates for wire variance from 0.08mm² up to 16mm², creating a round, uniform hexagonal profile that seats easily into compact terminal blocks.
From utility-scale solar arrays to aerospace wire harnesses, SIBO crimpers provide reliable connections where mechanical or electrical failure is not an option.
High-density automation panels demand clean ferrule terminations. SIBO self-adjusting ferrule crimpers produce clean square and hexagonal profiles, preventing loose wire strands and short circuits in spring-clamp DIN-rail terminals.
SO-06B and SN-48B series crimpers provide precision open-barrel "B-crimps." The wire conductor and insulation wings are rolled smoothly inward, delivering the high vibration resistance required by modern automotive standards.
Field installations of MC4 and compatible solar connectors require tools with factory-calibrated stops. The SO-2546 series provides repeatable crimp heights across thousands of PV junctions, preventing DC arc faults and generation loss.
Shipboard and rolling stock electrical installations experience continuous mechanical vibration and salt air exposure. Our heavy-duty insulated ratchet tools deliver gas-tight joints that resist corrosion and conductor pull-out.
Direct answers from our tooling engineers addressing common questions about tolerances, die selection, private labeling, and quality control.
Discover our specialized tool lines, including high-leverage open-barrel pliers, 1500V solar PV crimpers, and heavy-duty hexagonal terminal kits designed for enterprise use.