

Direct factory configurations covering ultra-compact spring terminals, open-barrel micro-connectors, and multi-profile self-adjusting ferrule mechanisms.

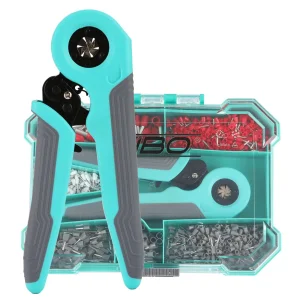
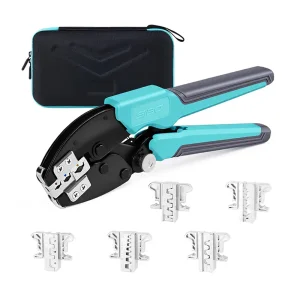
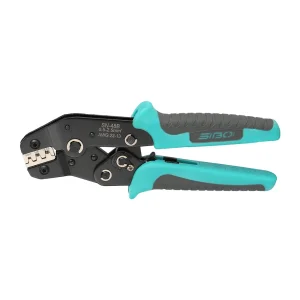
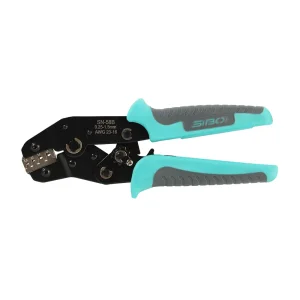
Evaluating compressive plastic deformation, molecular void elimination, and spring-back mechanics across micro-gauge conductor cross-sections.
In micro-crimping architectures spanning AWG 30 down to AWG 8 (0.05 to 10mm²), the terminal barrel and copper stranded filaments must undergo controlled plastic deformation. SIBO micro-dies apply precision radial vectors that rupture the external oxide films on individual copper strands, generating an oxygen-free, hermetically sealed mass with virtually zero internal gas voids.
An incorrect crimp height variance as minor as 0.02mm can induce either conductor strand shearing or terminal micro-slippage under vibration. Yueqing Sibo integrates calibrated eccentric star-wheel adjustment cams in every ratchet chassis, maintaining a strict optimal ratio between mechanical compaction density (80%–88%) and conductor tensile yield limits.
Micro jaws encounter localized yield pressures surpassing 850 MPa when compressing hardened brass, phosphor bronze, or nickel-plated copper terminals. Our die profiles are manufactured from vacuum-degassed SKD11 tool steel hardened to HRC 58-62, while body frames utilize drop-forged AISI 4140 carbon steel to completely eliminate structural frame deflection.
How Yueqing Sibo Tools leverages world-class industrial clustering in Zhejiang to compress development lead-times and optimize unit manufacturing economics.
Located in Huanghua Town, Yueqing—China’s global nucleus for electrical components—we reside minutes away from premier alloy smelters, heat treatment centers, and terminal manufacturers.
From CAD/CAM cavity design, high-speed wire-cut EDM, CNC progressive stamping to final mechanical ratchet assembly, every manufacturing gate is kept in-house with zero third-party dependencies.
Processing millions of hand crimpers annually allows Yueqing Sibo to procure high-purity alloy tool steel at institutional tiers, securing audited metallurgical consistency down to the heat batch.
While European or US tool shops require 12 to 16 weeks for custom jaw geometries, our direct Yueqing CAD/CAM rapid prototype cycle delivers field-ready sample dies within 14 working days.
| Tool Model Architecture | Applicable Cross-Section (mm²) | Conductor AWG Standard | Terminal Interface Compatibility | Die Geometry Mechanism | Standard Pull-Force (N) |
|---|---|---|---|---|---|
| SN-2549 Pro | 0.08 – 0.5 / 1.0 mm² | AWG 28 – 18 | JST, Molex, TE, DuPont Spring Terminals | Dual-Step Open Barrel Roll (F/B Crimp) | ≥ 18 N – 55 N |
| SO 16-4 Series | 0.08 – 16.0 mm² (Optimized 0.08–10) | AWG 28 – 5 | End Sleeves, Insulated & Bootlace Ferrules | Quad-Serrated Self-Adjusting Mandrel | ≥ 80 N – 570 N |
| SN-48B Micro | 0.14 – 1.5 mm² | AWG 26 – 16 | Faston 2.8mm, 4.8mm Open-Barrel Tabs | Progressive Radius B-Crimp Profile | ≥ 40 N – 135 N |
| SN-58B Universal | 0.25 – 1.5 mm² / Micro 0.05 opt. | AWG 30 – 16 | JST XH/SM, Dupont 2.54, Molex Micro-Fit | High-Density Precision Step Indenters | ≥ 15 N – 120 N |
| SO-2546C Pro | 2.5 / 4.0 / 6.0 / 10.0 mm² | AWG 14 – 8 | MC4 Solar Photovoltaic Connectors | High-Compression Hex/Indent Locators | ≥ 310 N – 800 N |
| SO-10 Pro | 0.5 – 10.0 mm² | AWG 20 – 7 | Non-Insulated Lugs, Copper Ring Terminals | Centric Punch & Saddle Indent Die | ≥ 110 N – 700 N |
How tier-1 hardware brands, telecom utilities, and electrical wholesalers scale branded tool programs with zero compromise on ergonomic longevity.
SIBO delivers end-to-end white-labeling capabilities: dual-color injection-molded TPR/PP soft grips molded to your corporate Pantone guidelines, fiber laser etching of high-resolution brand identifiers, and customized blister packaging, EVA-foam storage trays, or heavy-duty 1680D Oxford fabric storage cases.
Industrial harness assembly lines subject operators to over 3,500 manual cycles per shift. SIBO's compound mechanical linkage reduces required hand grip actuation pressure by 35% to 42%, redistributing vector peak loads evenly across the palm to safeguard assembly personnel against repetitive carpal tunnel strain.
We provide pre-packaged multi-die micro-crimping ecosystems featuring quick-release magnetic retainers. Technicians can pivot from 0.08mm² JST signal lines to 10mm² main power ferrules in under 5 seconds without unscrewing fixtures or re-calibrating mechanical stop-collars.
Global technical assurance designed to satisfy CE, UL, RoHS, REACH, and ISO 9001:2015 traceability audits.
Every batch of ratchet mechanisms undergoes automated pneumatic cycling rigs in our Yueqing testing facility. Tools are cycle-tested through 50,000 full mechanical closures under resistance load, confirming zero slippage of the ratchet teeth, zero jaw alignment drift, and uncompromised release tooth reliability.
Grip coatings, thermoplastic components, and surface conversion coatings (black oxide, chemical nickel, zinc-iron passivation) are formulated free of hazardous phthalates, SVHC substances, hexavalent chromium, and restricted heavy metals, facilitating unobstructed customs clearance throughout North America and the European Union.
To fulfill the demands of automotive (IATF 16949 supply chain) and aerospace wire harnesses, SIBO conducts cross-section metallurgical polishing and acid-etch micrograph analysis. We inspect strand deformation ratios, crimp symmetry, and compression depth to prevent under-crimped overheating or over-crimped conductor embrittlement.
Where vibration resistance, low millivolt drop, and microscopic mechanical tolerances determine system stability.
Modern electric vehicle battery management systems rely on micro-gauge signal harnesses (0.14–0.5mm²) operating in extreme thermal-vibrational environments. Our SN-2549 and SN-58B deliver cold-welded crimp joints with ultra-low milliohm contact resistance that eliminate false CAN-bus error triggers.
Surgical robotic limbs and patient monitoring telemetry mandate high-density 0.05mm² (AWG 30) micro-pitch connectors (Hirose DF13, JST SH 1.0mm). SIBO’s micro-cavity dies prevent damage to micro-locking tangs while achieving high-integrity mechanical retention.
Dense DIN-rail terminal blocks in PLC panels demand clean square or hexagonal bootlace ferrule crimping from 0.25 to 10mm². The SO 16-4 self-adjusting mechanism forms compact, non-fraying terminal sleeves that slip effortlessly into spring-clamp or screw cages.
Analyzing the next decade of connector miniaturization, alloy innovations, and smart crimp process telemetry.
As autonomous devices, UAV drones, and IoT edge controllers compress internal spatial volume, wire gauges are shifting beyond AWG 28 toward ultra-fine AWG 32 (0.035mm²). Yueqing Sibo is actively engineering next-generation ultra-micro die geometries with micro-stepped positioning locators to guarantee fail-safe open-barrel roll crimps on sub-millimeter terminal pitches.
Future crimping tools are moving toward digital QA integration. SIBO's R&D team is developing passive tactile calibration feedback notches and integrated piezoelectric micro-sensors that provide mechanical verification that the critical threshold pressure was applied across the 0.05–10mm² span prior to ratchet disengagement.
By pairing drop-forged structural steel stress rings with high-strength carbon-fiber-reinforced polymer handles, upcoming SIBO tool platforms will achieve a 28% total weight reduction without yielding an ounce of mechanical stiffness or altering the critical die alignment axis under high-tonnage crimping cycles.
Exhaustive answers to technical and supply chain inquiries commonly raised by global electrical distributors and manufacturing buyers.
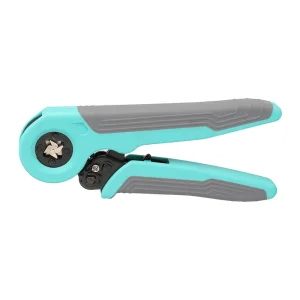
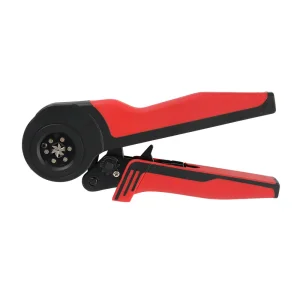
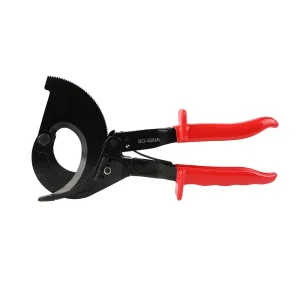
Expanding our wholesale portfolio with hexagonal ferrule pliers, high-tonnage cable shears, and specialized solar photovoltaic crimping equipment.

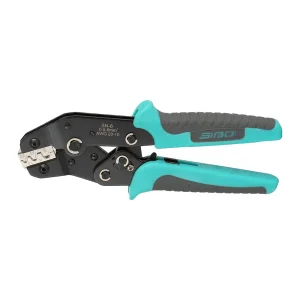
Request our exhaustive 2026 technical crimping catalog, discuss custom micro-die tolerances with our application engineers, or initiate your OEM private-label quotation today.