Direct from our specialized Yueqing production facility: verified alloy steel dies, self-regulating pressure ratchets, and high-repeatability hand tooling engineered for electrical contractors, panel builders, and harness manufacturers.
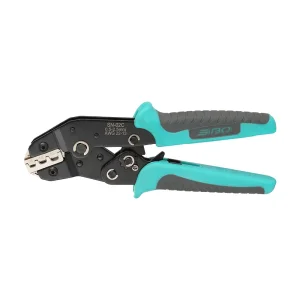
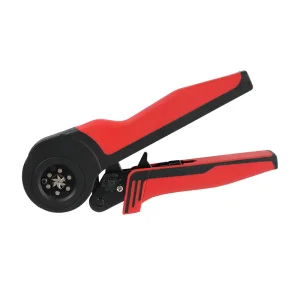
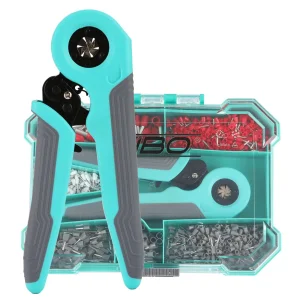
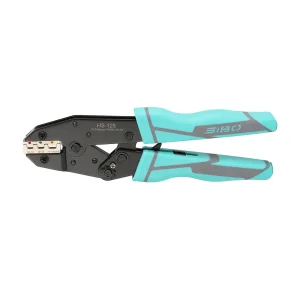
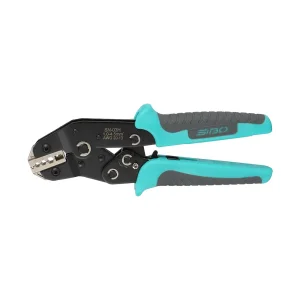
A wire terminal crimp is not merely a mechanical deformation; it is an electro-mechanical gas-tight interface designed to maintain micro-ohmic conductivity and extreme mechanical shear strength across decadal lifespans.
Within high-performance industrial electrical connections, terminal crimping replaces traditional soldering by achieving controlled plastic deformation of both the stranded conductor and the contact sleeve. When engineered correctly, this process generates a cohesive metallographic bond known as a "cold weld." The pressure exerted by our precision-ground die cavities exceeds the yield point of copper, breaking superficial oxide coatings and creating clean metal-to-metal contact boundaries.
Failure in crimp geometry results in two severe modes: under-crimping leads to high contact resistance, galvanic corrosion, and catastrophic thermal thermal runaway under full ampere load; over-crimping induces micro-fracturing of the outer copper strands, compromising mechanical tensile holding capability under cyclic mechanical vibration.
SIBO tooling parameters are systematically calibrated against international tensile pull-out thresholds to ensure zero pull-off or strand pull-out during operational lifetimes:
Positioned in Yueqing, Zhejiang—the global capital of low-voltage electrical apparatus—Yueqing Sibo Tools leverages unmatched vertical integration, proprietary tool-steel metallurgy, and scalable high-volume precision manufacturing.
Unlike assembly-only vendors, our production covers the complete chain: in-house CAD/CAM tooling design, wire electrical discharge machining (WEDM), automated CNC profile milling, stamping, and automated polishing. We control quality at the atomic metallurgical stage.
Yueqing hosts over 10,000 electrical component fabricators. Our engineers co-develop crimping jaws alongside connector mold makers, ensuring that whether dealing with DIN-standard ferrules or specialized open-barrel automotive tabs, our dies accommodate real-world stamping tolerances.
Every batch of pliers undergoes strict multi-axis automated testing: ratchet cycle lifespan evaluation, micro-hardness Rockwell testing (HRC), optical profile projection for die cavity wear, and tensile pull tests exceeding ASTM and ISO electrical guidelines.
High-precision slow-feeding wire electrical discharge creates cavity micro-profiles to +/- 0.005mm.
Heavy tonnage drop forging of structural carbon tool steel ensures continuous grain flow and rigidity.
Computer-monitored heat treatment prevents decarburization, stabilizing Rockwell hardness at HRC 45+.
Precision calibration of spring-loaded ratchet eccentric gears ensures mandatory cycle completion.
Batch sampling via automated tensiometers to confirm electrical resistance and tensile pull-off limits.
Professional tool importers, national electrical wholesalers, and multi-tier OEMs require stringent compliance, consistent supply cadence, customized ergonomic configurations, and retail-ready packaging programs.
Yueqing Sibo Tools provides end-to-end white-label and private-brand manufacturing programs. We work alongside category managers and technical directors to produce hand tooling that reinforces your brand identity in competitive retail and industrial distribution landscapes.
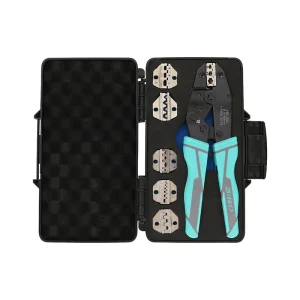
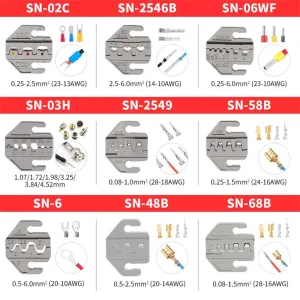
Our engineering services extend to complete modular kits, such as our popular Oxford cloth zipper-bag sets containing interchangeable jaw cassettes (pre-insulated, ferrule, open barrel, MC4, and coaxial), providing multi-industry utility within a single consolidated SKU.
Different regional markets enforce unique electrical codes and tool ergonomics. Our tools are systematically designed to fulfill specific regional installation standards across critical industrial sectors.
Utility-scale and rooftop PV farms demand precision crimps for MC4, Amphenol H4, and compatible connectors. Tools like our SO-2546B/C ensure absolute contact stability at 1500V DC under thermal cycling.
Modern vehicles and electric mobility systems employ micro-pitch open-barrel connectors and battery management sensors requiring F-crimp and B-crimp profiles with exceptional tensile retention.
High-density control cabinets, PLC terminals, and DIN-rail terminal blocks rely on bootlace ferrules crimped with square or hexagonal profiles (HSC8 series) to eliminate strand fraying.
Precision wire-to-board joints, gold-plated contacts, and avionics test fixtures demand tools with integrated emergency releases and unyielding mechanical stroke repeatability.
Driven by Industry 4.0 traceability, lightweight materials, and human-factors ergonomics, manual and electro-hydraulic terminal crimping technologies are undergoing substantial evolutionary breakthroughs.
Modern high-liability harness manufacturing is integrating sensor-laden ratchets. Micro strain-gauges monitor peak pressure curves in real-time, wirelessly communicating with factory MES systems to flag incomplete strokes and generate auditable batch quality logs.
Replacing traditional heavy stamped plates, modern structural designs integrate forged aircraft-grade aluminum handles and lightweight titanium pivot plates. This reduces hand fatigue by over 30% for field electricians operating at high duty cycles.
Tool-less magnetic and slide-lock quick-interchange cassettes allow technicians to swap between insulated flag terminals, non-insulated bootlaces, and solar contacts in under 5 seconds without carrying multiple complete plier frames.
Explore high-capacity self-adjusting ferrule tools, flag-terminal specialty ratchets, and modular multi-cavity crimp jaw combinations engineered for heavy-duty wiring solutions and precision electrical fabrication.

Essential technical, manufacturing, and supply-chain answers for industrial distributors, electrical wholesale procurement leads, and international OEM product managers.
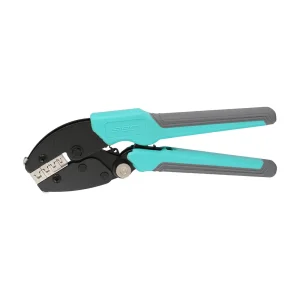
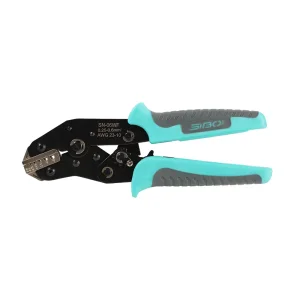
Every ratchet frame incorporates an internal multi-tooth escapement mechanism. Once the crimping stroke initiates, the spring-loaded pawl blocks reverse travel until the die faces fully mate at the factory-calibrated bottom dead center. This eliminates incomplete crimps caused by operator arm fatigue. Emergency release levers allow non-destructive release if an improper gauge wire is inserted.
Depending on client specification and volume requirements, our jaws are formed using either precision-investment cast 42CrMo structural alloy or wire-EDM milled AISI D2 / SKD11 cold-work die steel. Surfaces undergo controlled vacuum hardening and optional black oxide or micro-layer chrome plating, yielding a surface hardness of HRC 58-62 for over 50,000 crimp cycles without cavity widening.
For standard tool frames with customized laser-etched branding and private-label handle coloration, our typical MOQ starts at 500 units per SKU. For custom tool steel die geometries or specialized multi-jaw combo kits in custom-embroidered Oxford cases, MOQ is typically 1,000 units. Mixed container orders across multiple electrical tool categories are supported.
We supply comprehensive technical compliance dossiers including RoHS 2.0 and REACH SVHC test declarations, CE conformity documentation for powered or mechanical equipment, and destructive tensile pull-out verification data aligned with DIN EN 60352-2 and UL 486A-B testing methodologies.
Square profile crimpers (e.g., HSC8 6-4) offer optimal mechanical pull-off force and fit rectangular terminal block apertures seamlessly. Hexagonal crimpers (e.g., HSC8 6-6 and 16-6) provide a uniform 360-degree rounder cross-section, reducing insertion friction in compact round spring-clamp terminals and high-density PLC connection points.
Yes. By supplying sample terminal strips and copper wire specimens, our engineering team utilizes optical measuring systems and FEA stress simulation to produce custom EDM die prototypes within 10 to 14 working days, followed by sample crimp micrography validation prior to commercial tooling release.
Our CNC machining and grinding centers operate under statistical process control (SPC) with automated CMM inspections checking die radius and crimp height to +/- 0.015 mm. Assembly fixtures are audited every 2,000 cycles, and critical pivot pins are centerless-ground to prevent lateral jaw deflection.
Standard catalog items maintain buffer stock in Yueqing, enabling dispatch within 7 days. High-volume OEM production runs of 5,000 to 20,000 units are fulfilled in 25 to 35 calendar days. Consolidated shipping is coordinated through nearby Ningbo or Shanghai maritime container ports with complete export customs processing.
